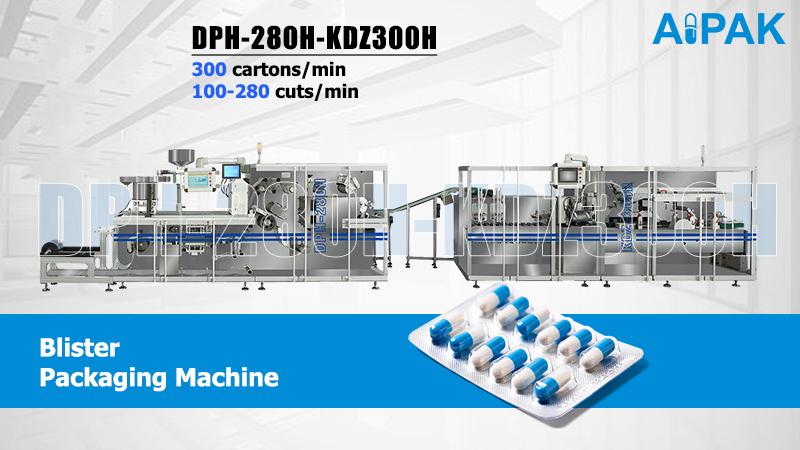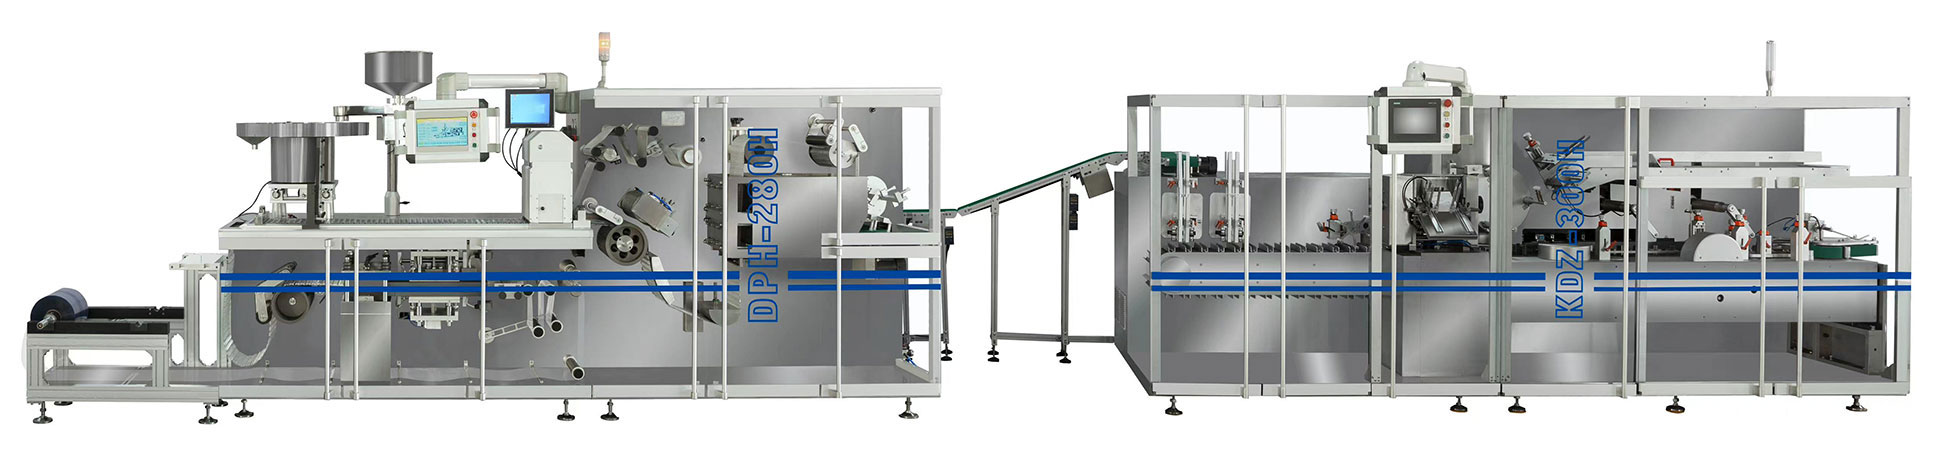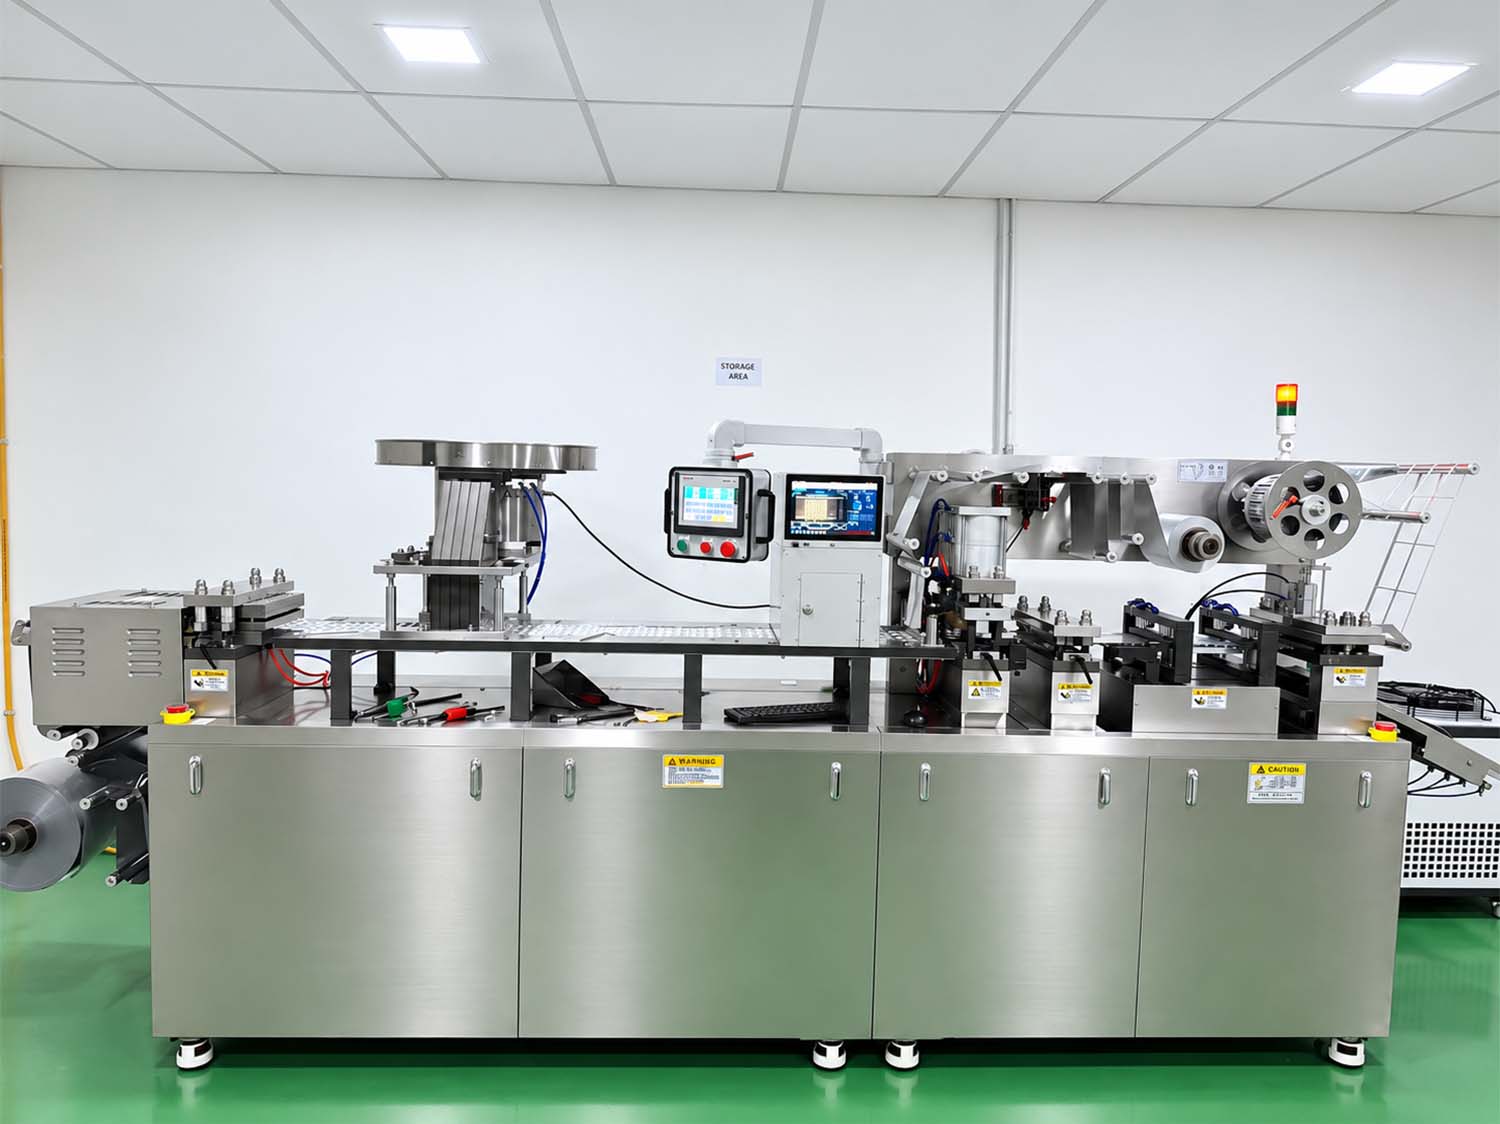
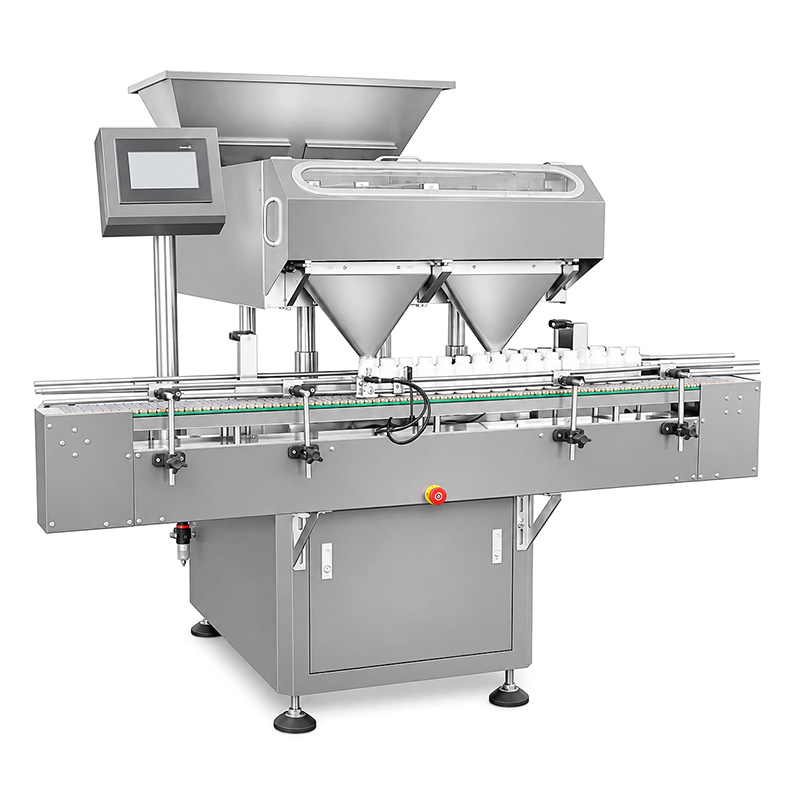
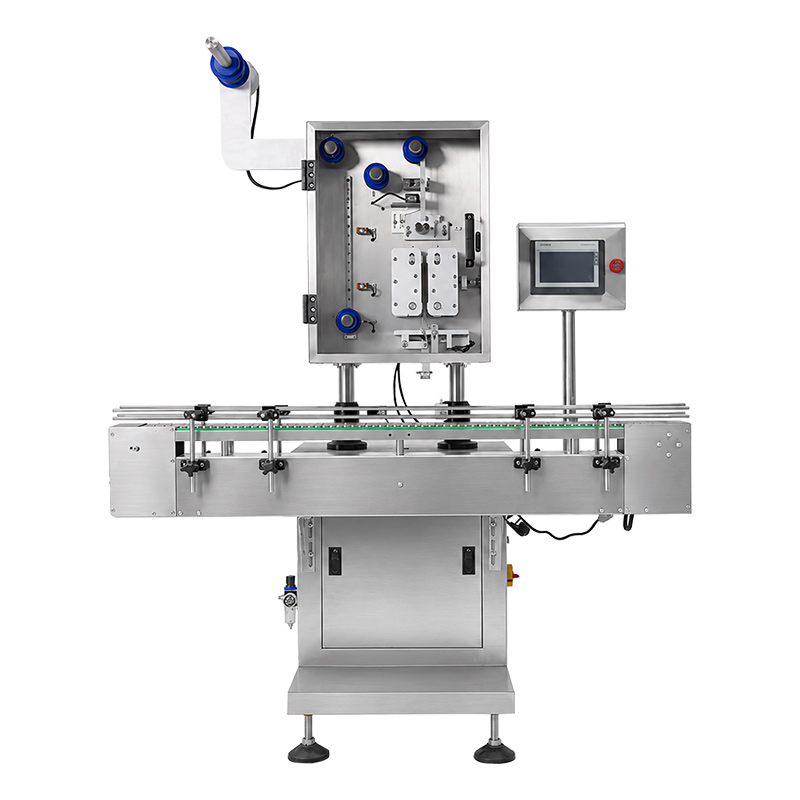
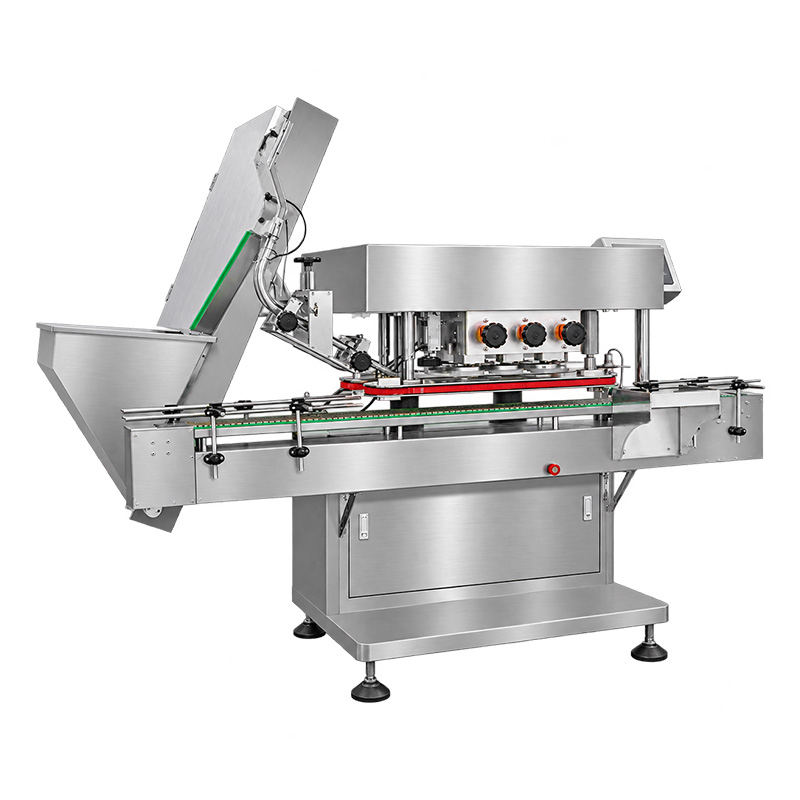
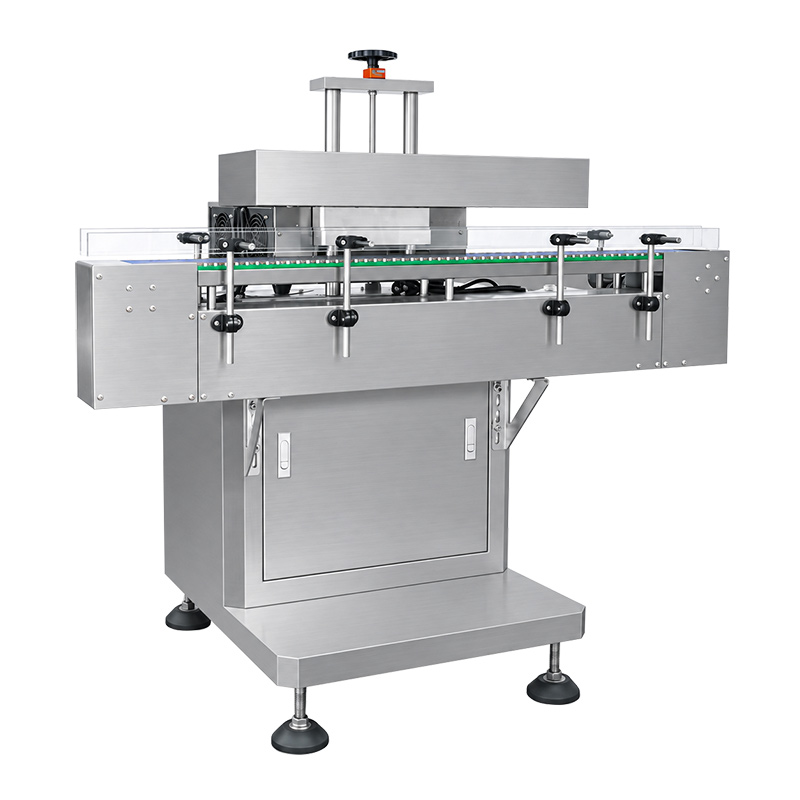
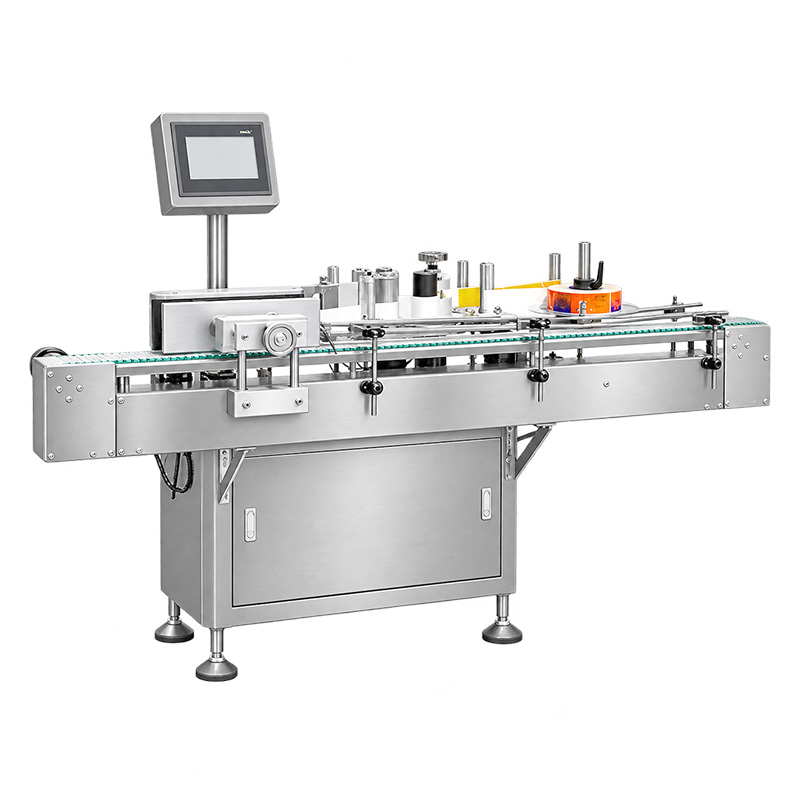
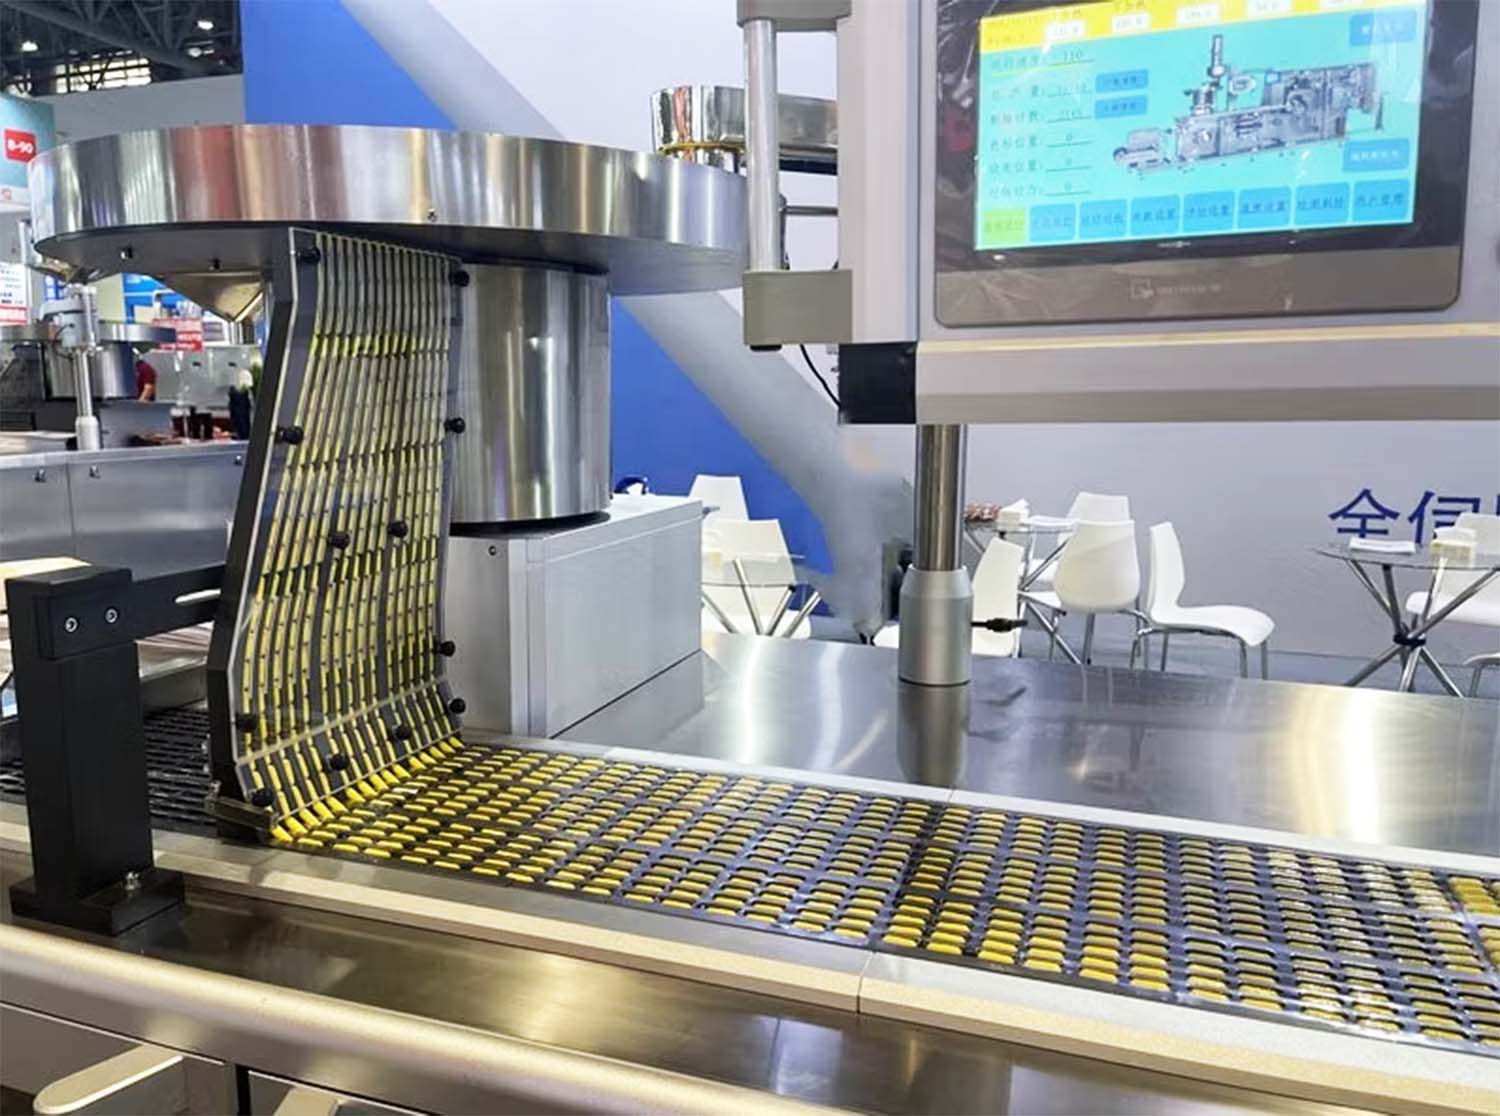
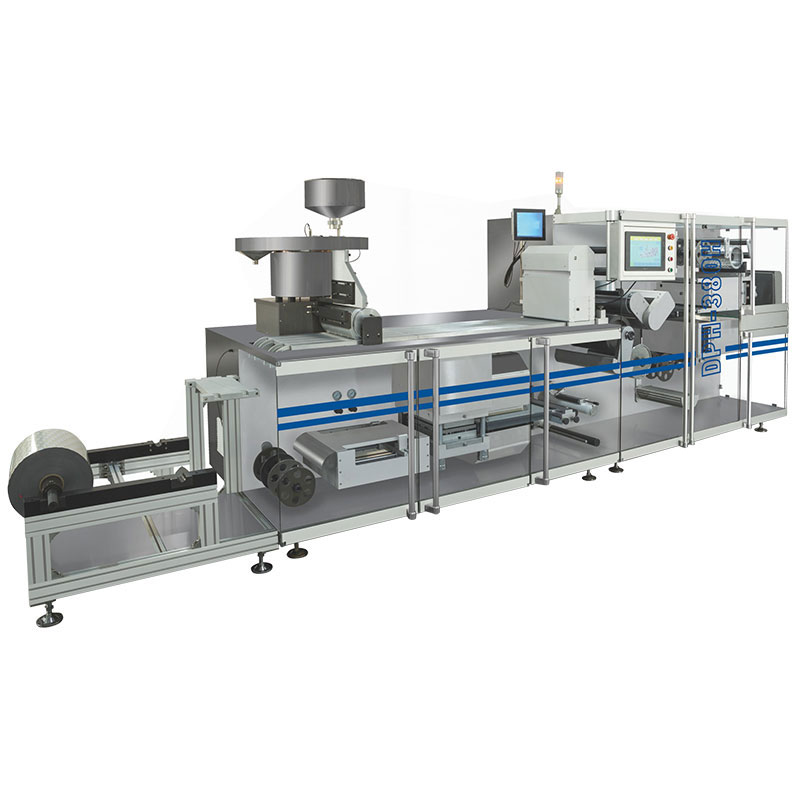
DPH-280H-KDZ300H Full Servo High-Speed Blister Cartoning Line

Your blister machine and your cartoner are two separate machines with an operator between them, and the carton bench is where the line backs up. This one links them — the blister machine sets the pace, the cartoner follows it, and a rejected blister means no carton and no leaflet are drawn for that cycle.

1. Line speed: up to 300 cartons a minute
2. Blister punch frequency: 40 to 180 a minute on Alu-PVC, 20 to 80 on Alu-Alu
3. Plates per carton: 1 to 10, set on the HMI
4. Carton size: 70–180 × 35–85 × 15–50 mm
5. Line footprint: 9,500 × 1,500 × 2,000 mm

Is this the right machine for you?

✓ Yes, if…

✕ Buy something else if…

Technical specification

Combined System

Specification


Model

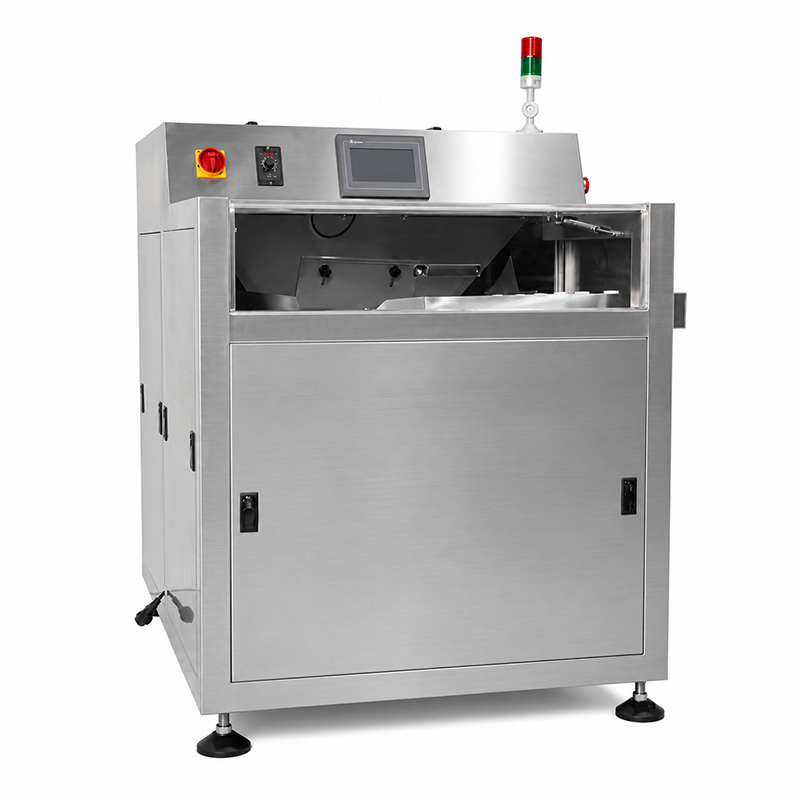
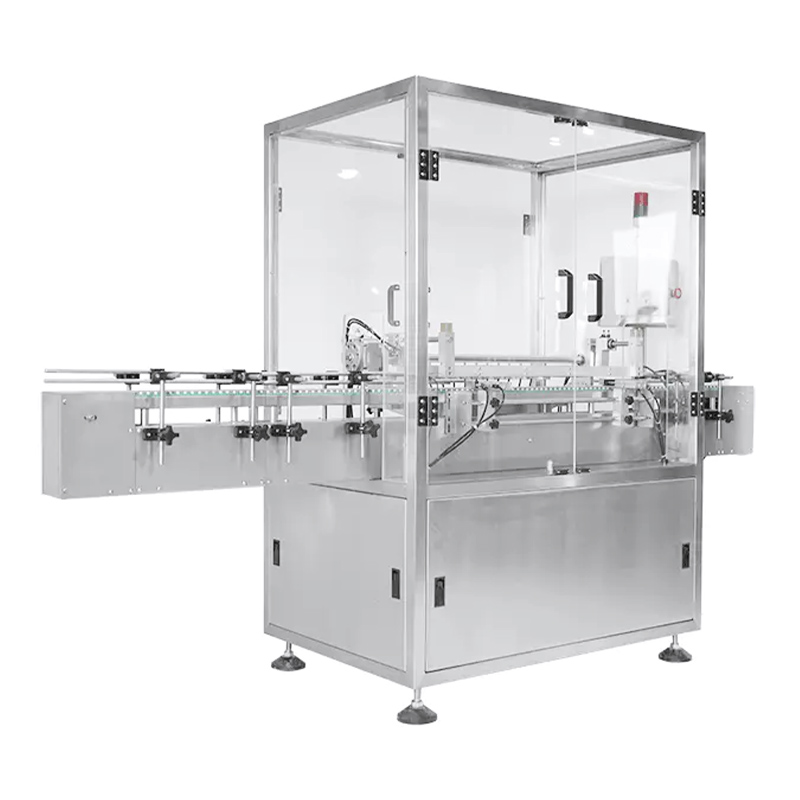
DPH-280H (Blister) + KDZ300H (Cartoner)


Max. Line Speed

300 cartons/min (Synchronized)

The cartoner’s ceiling. Your actual rate is set by the blister machine and your plates per carton

Blister Punch Frequency

40–180 cuts/min (Alu-PVC), 20–80 (Alu-Alu)


Max. Forming Area

280 × 200 mm


Carton Size Range (L×W×H)

(70 – 180) × (35 – 85) × (15 – 50) mm (customizable)


Leaflet Size Range (Unfolded)

(100-250) x (100-180) mm

Larger leaflets won’t fold on this folder

Blister Stacking Range

1 – 10 plates per carton (Servo-adjustable)

Changed on the HMI, not by mechanical adjustment

Total Power

25 kW (blister machine) + 6 kW (cartoner main motor)


Compressed Air

0.5–0.7 MPa; about 350 L/min (blister) + 160–200 L/min (cartoner)


Standard Material Width

270 mm (PVC/ALU/PTP)


Material Specification

PVC, ALU, PTP, Dialysis Paper, 250-350g Paperboard


Line Dimensions

9500 × 1500 × 2000 mm (L × W × H)

Straight-line layout. L or U shapes change the length

Total Weight

4,500 kg


Power supply

Three-phase five-wire, 60 Hz. Built to your U.S. supply; we confirm the voltage with your quote


Carton size

70–180 × 35–85 × 15–50 mm

Send us your carton — the pusher needs clearance a hand-packed carton doesn’t have


What the line actually does

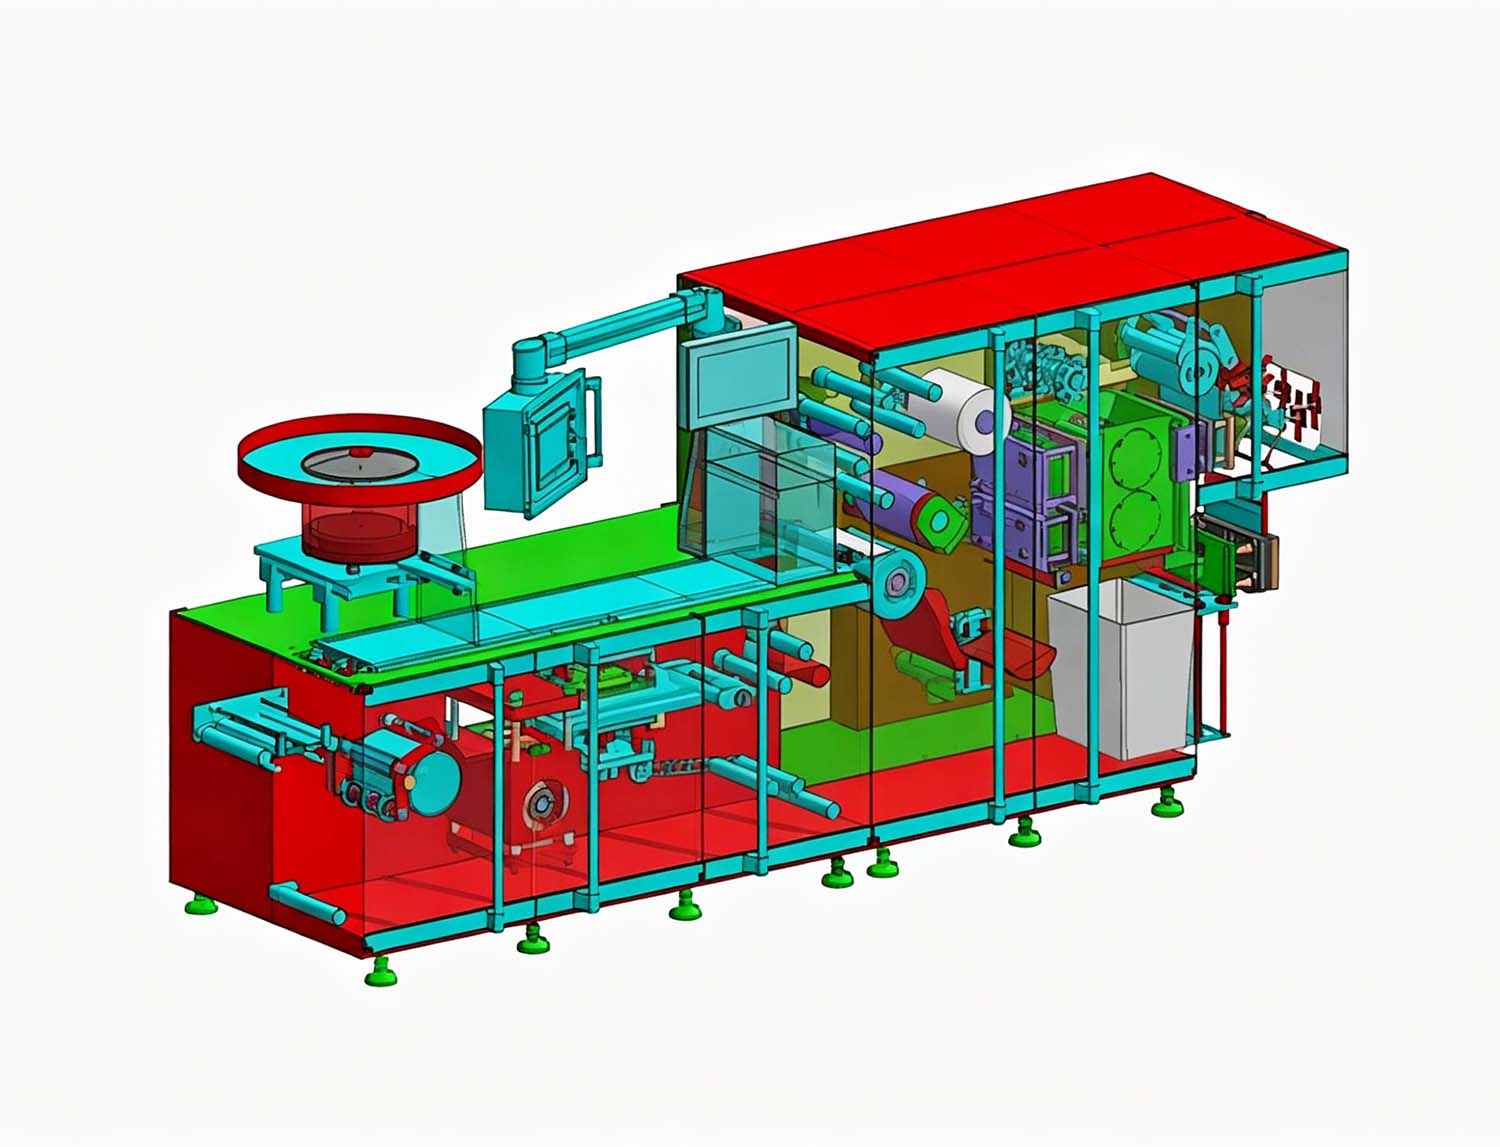
SEVEN STATIONS, ONE LINE

Station 1

Blister machine

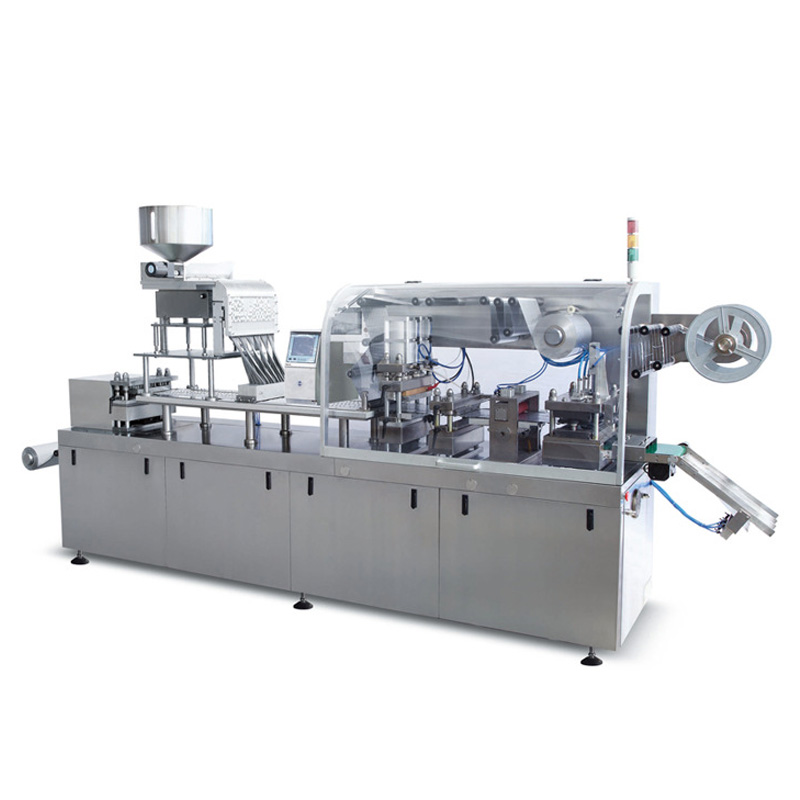
Forms, fills, seals and cuts the blister plates. Sets the pace of the whole line.

Station 2

Vision inspection and reject

A camera checks every plate for empty pockets and broken tablets. A failed plate is rejected here.

Station 3

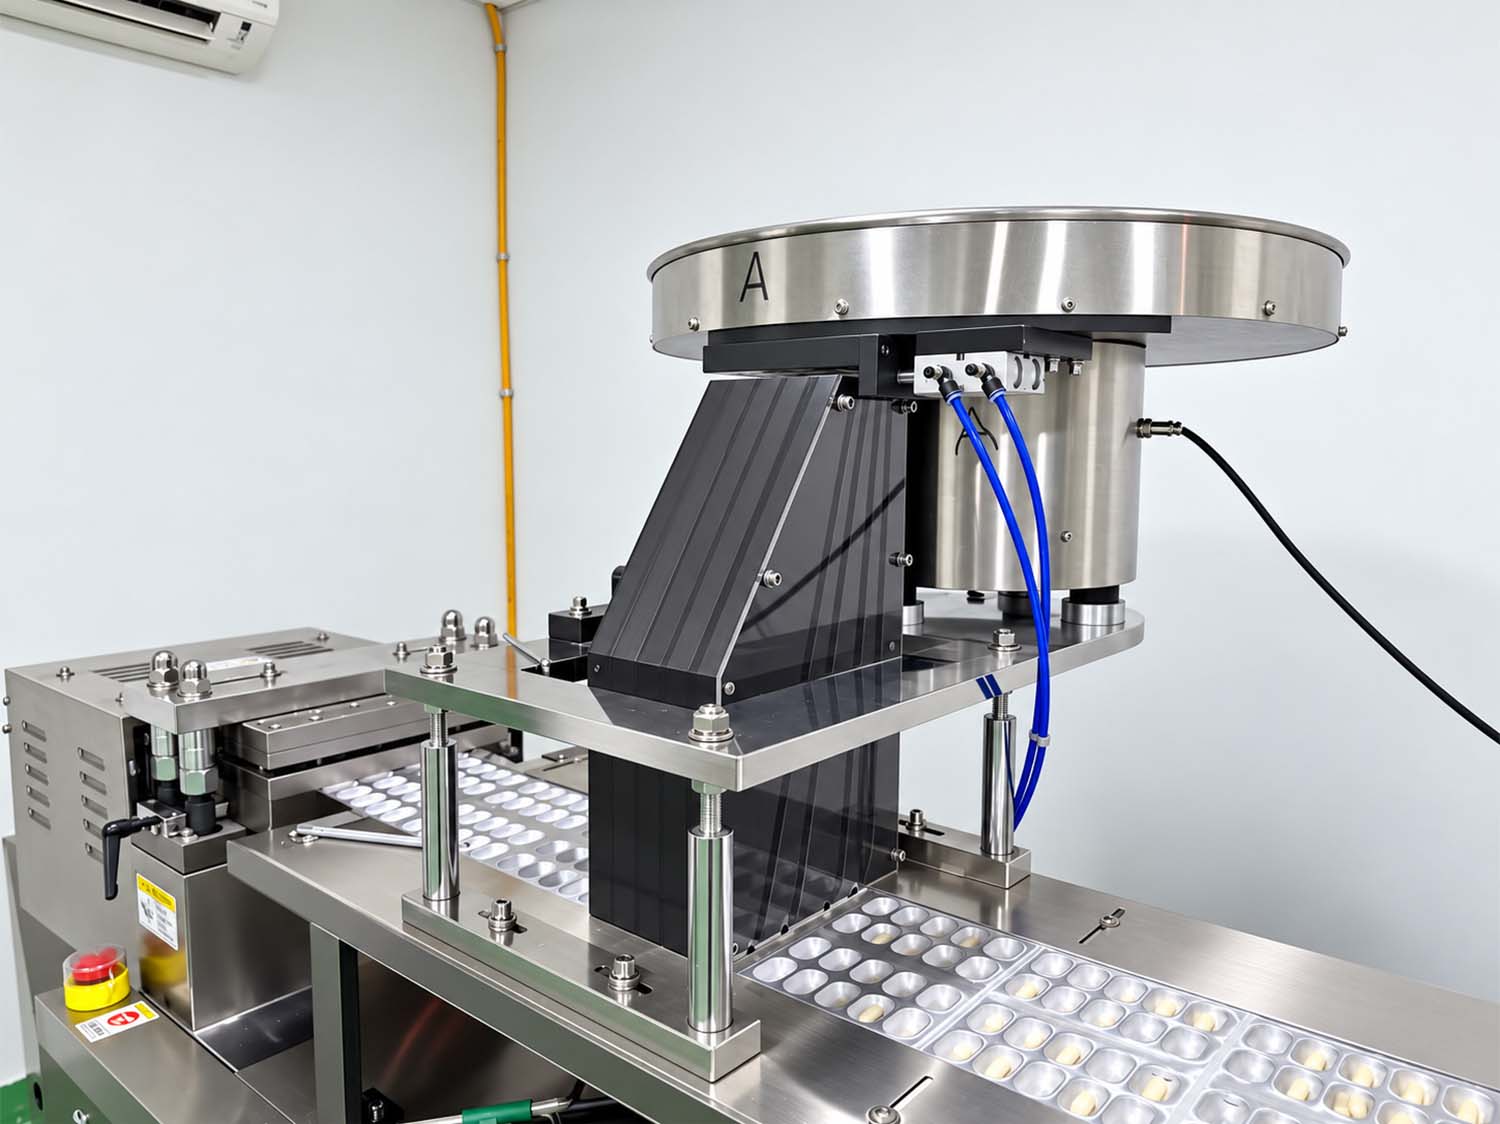
Stacking

Counts plates into stacks of 1 to 10 per carton, set on the HMI.

Station 4

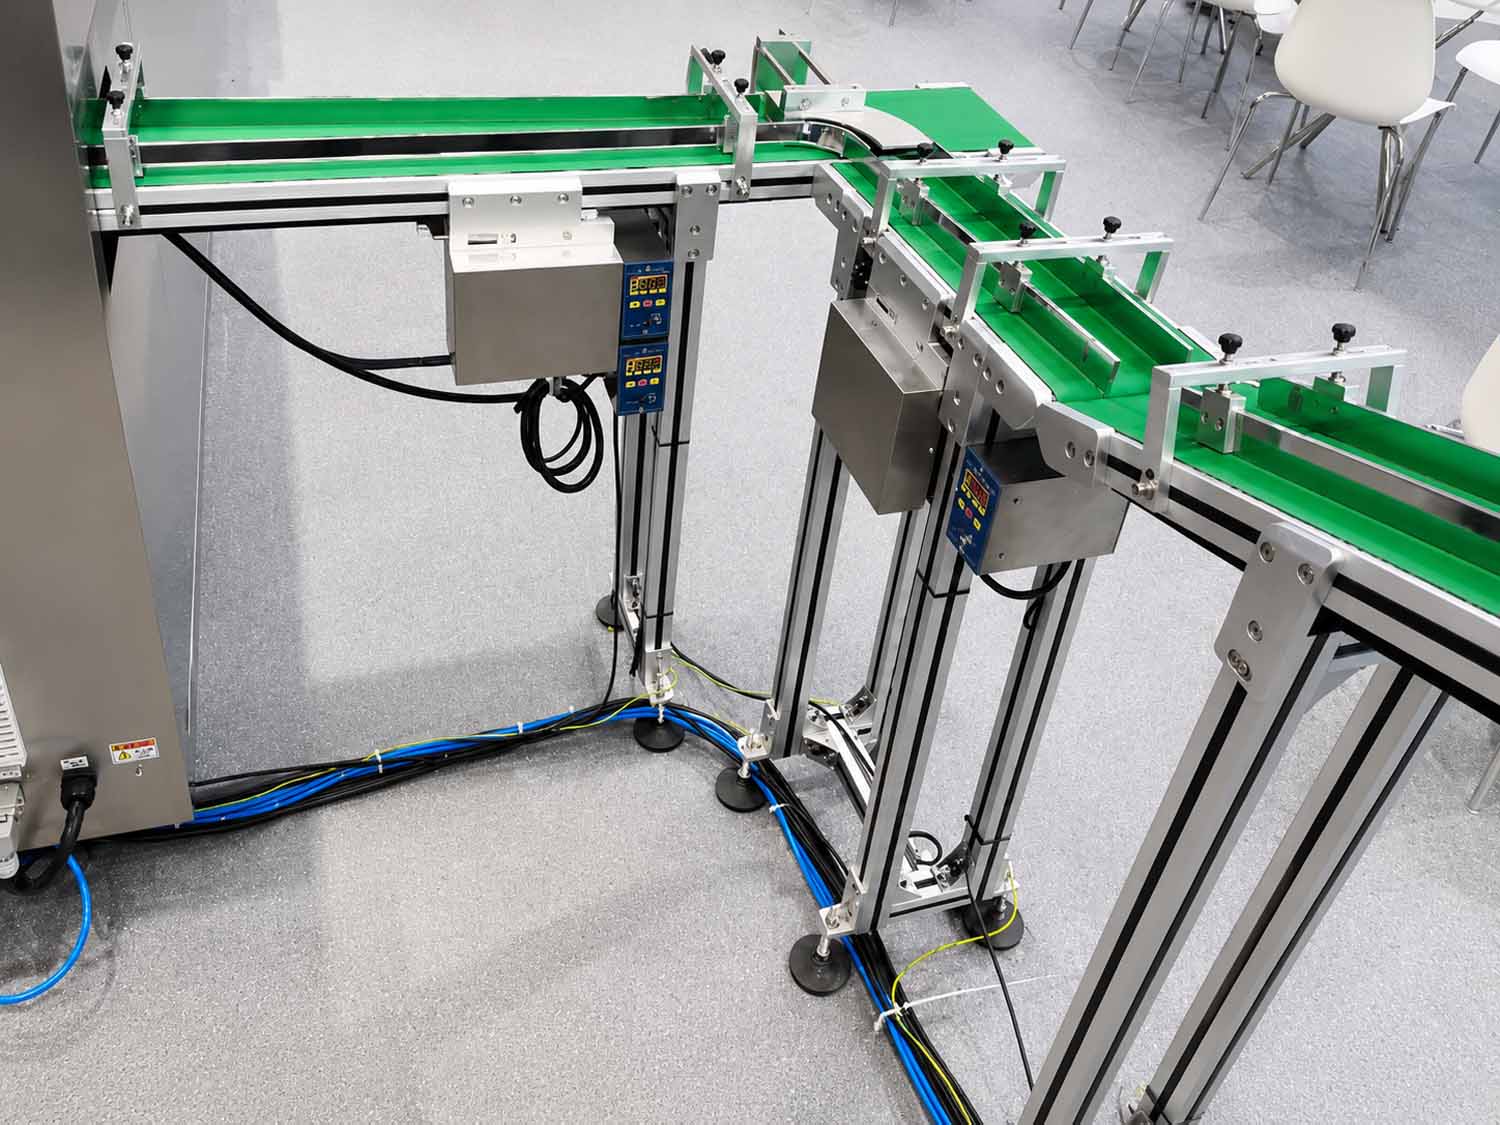
Transfer bridge

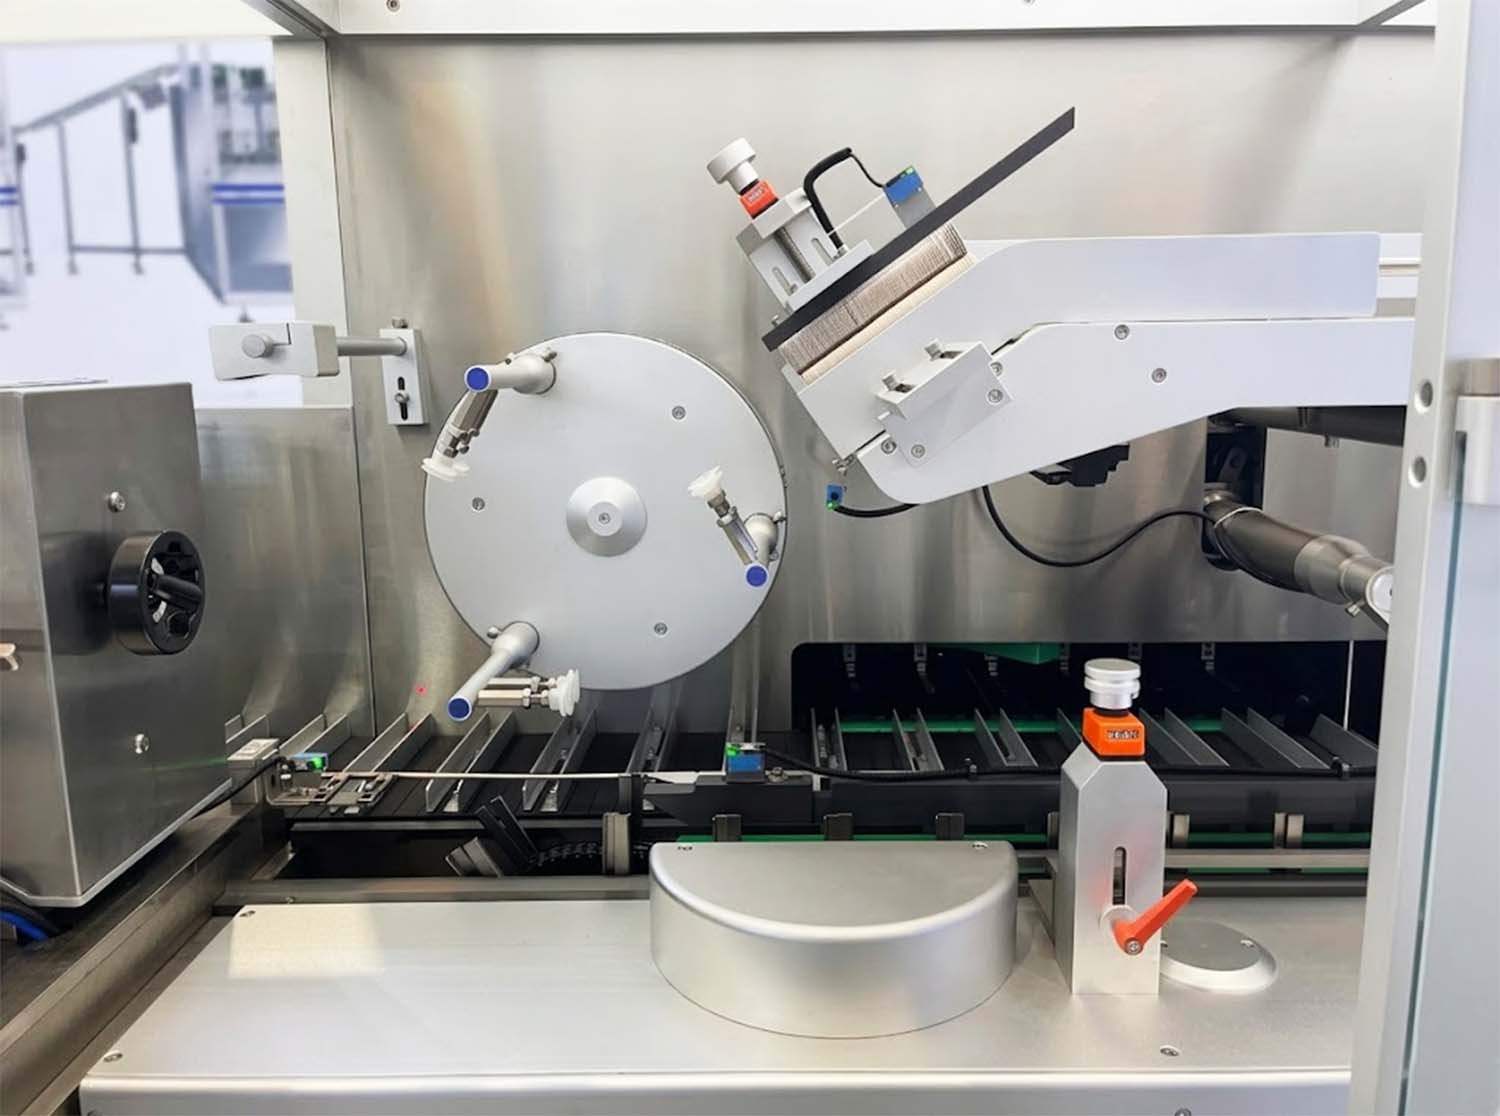
Lifts each stack with vacuum cups and carries it to the cartoner, with no sliding on the foil.

Station 5

Leaflet folding

Folds the leaflet and feeds it in step with each stack.

Station 6

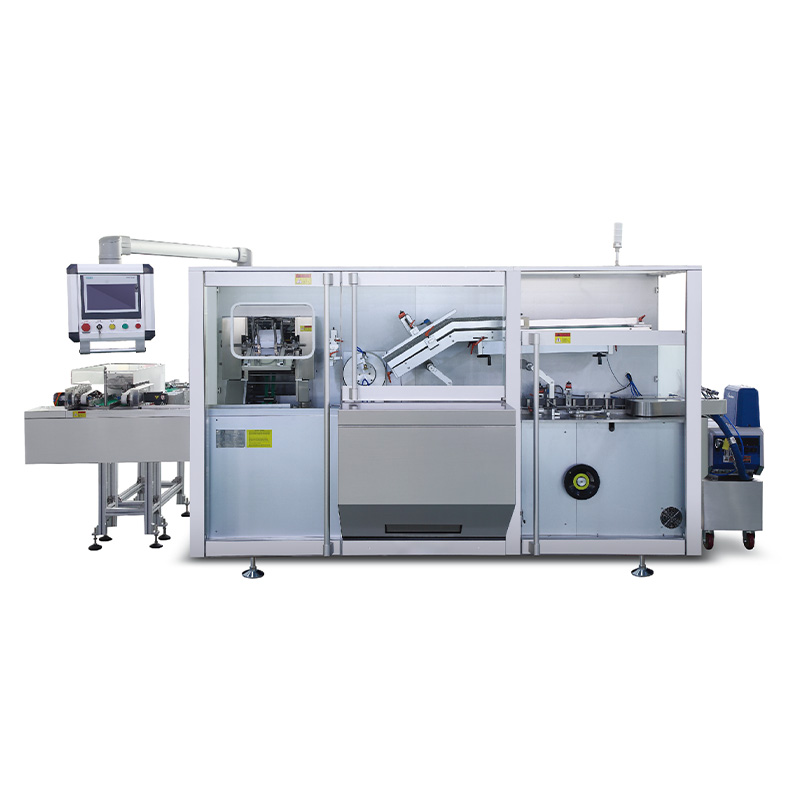
Cartoner

Opens the carton, inserts the stack and leaflet, and closes it.

Station 7

Outfeed

Discharges the finished cartons to your case packing.

The blister machine sets the pace. Everything downstream follows it — which is why the line speed on any spec sheet is the cartoner’s ceiling, not your output. Your actual rate is the plates the blister machine cuts a minute — punches times plates per punch — divided by plates per carton. At 180 punches a minute and two plates a punch, that’s 360 plates a minute: 36 cartons at ten plates a carton, or the cartoner’s 300 ceiling at one plate a carton. Tell us your plate layout and count per carton and we’ll work out your real number.

"Smart-Link" Synchronization Bridge

A buffer and transfer station between the two machines adjusts its speed to the blister machine’s real-time output, so the cartoner follows the blister machine rather than the other way round.

Full-Servo Precise Stacking

The blister counting and stacking module uses high-speed servo motors to accurately group 1–10 blister plates per carton, allowing for instant format changes via the HMI.

Separated Drive Frame, Modular Tooling

Drives sit behind the working area on both machines. Format tooling is modular across the line — but note that changing over a linked line means changing both machines together, which is longer than changing one.

A Rejected Blister Means No Carton

When the vision system rejects a blister upstream, the cartoner receives that signal and skips the cycle — no carton drawn, no leaflet folded. On a line running 300 cartons a minute, that’s the difference between wasting one blister and wasting a blister, a carton and a printed leaflet.

Industry Applications

A linked line pays back on long runs of one or two formats. These are the packs it’s built for:

30-day and 60-day supplement packs

Multiple blister plates in one carton — 30-day packs usually run three to five plates, 60-day packs six to ten. Stacking count is set on the HMI, so the same line runs both.

Single-plate retail cartons

One plate, one leaflet, one carton at full line speed. This is where 300 cartons a minute is actually reachable.

Cold-formed Alu-Alu packs

The transfer bridge lifts blisters with vacuum cups rather than pushing them, so there’s no sliding friction on the foil surface.

Multi-SKU contract packing

Several counts and carton sizes across a week. Recipe recall handles the timing; the tooling still changes by hand.

What changing over involves

A linked line changes over as one unit. That’s the trade-off you’re buying.

What changed

What you adjust

Roughly

Plates per carton (3 → 5)

Stacking count on the HMI

Minutes

Carton size changes

Cartoner tooling, plus the transfer bridge

15–45 minutes

Blister format changes

Blister tooling and the stacker and the cartoner

15–45 minutes

Alu-PVC → Alu-Alu

Blister tooling and feeder

Not a changeover

On two separate machines you can change one while the other keeps running. On a linked line you can’t. If you switch format more than once a week, that’s worth weighing against the operator you save between the two stations.

What to check before you buy

01

The tooling, not the machine

A format set covers four synchronized stations. Ask any supplier who designs the pocket layout, how long a new format takes to make, and what it costs. That's where a blister project succeeds or fails.

02

The feeder, before you order

An Alu-PVC universal feeder cannot run cold-formed Alu-Alu, and it cannot be converted afterwards. Ask which feeder you're being quoted and what it locks you out of.

03

Installation and training

Ask what's included and what costs extra. The answer varies more between suppliers than the machine price does.

Why Choose AIPAK?

One Point of Contact

One project engineer handles your machine from proposal to commissioning, so you’re not chasing five suppliers for one answer.

We Design the Pocket Around Your Product

Send us your tablet or capsule samples and tell us your foil. We design the pocket layout and specify the feeder before we quote, because an Alu-PVC universal feeder can’t be converted to Alu-Alu later.

A U.S. Number, Answered by Us

+1 (213) 526-8644, answered by our engineers 9 AM–7 PM China time, Monday to Friday. That’s evening and overnight in the U.S., so leave a message or send a WhatsApp anytime and we’ll pick it up first thing.

Spare Parts and Lead Time, in Writing

A kit of wear parts ships with your machine. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.

High-Speed Integrated Blister Cartoning Line FAQ

What happens when a blister is rejected upstream?

The cartoner skips that cycle. When the camera on the blister machine rejects a plate, for example for an empty pocket, the KDZ300H receives the signal through a shift register and doesn’t draw a carton or a leaflet for it. You lose one blister, not a blister, a carton and a printed leaflet.

How does the vacuum transfer bridge protect the delicate surface of ALU/ALU blisters?

Conventional “push-style” transfers can scratch the aluminum foil or cause micro-cracks due to friction. Our line features a “Pick-and-Place” Vacuum Manifold equipped with silicone suction cups. It lifts the blisters vertically and deposits them into the stacking magazine. There’s no sliding on the foil, preserving the aesthetic and structural integrity of your high-end ALU/ALU or Tropical Blister packs.

Can this line handle complex "Leaflet-First" or "Blister-First" insertion requirements?

Yes. The KDZ300H cartoning unit is equipped with a synchronized insertion arm. The software allows you to calibrate the insertion sequence so that the leaflet can be wrapped around the blister stack or placed on top, depending on your market’s regulatory requirements. This is all adjustable via the HMI without mechanical re-timing.

How does the line deal with "Heat Accumulation" during long high-speed shifts?

The forming molds and the sealing drum are cooled by an external chiller, which keeps the blister web from deforming at full speed. You’ll need space and power for the chiller next to the line.

What's my actual output?

Take the plates the blister machine cuts a minute — punches times plates per punch — and divide by your plates per carton. At 180 punches and two plates a punch, ten plates a carton is 36 cartons a minute, not 300. The 300 figure is the cartoner’s ceiling, and you only get near it on single-plate cartons. Tell us your plate layout and count per carton and we’ll give you your number before you go any further.

Does it run on US power?

Yes. We build to your U.S. supply at 60 Hz and confirm the voltage with your quote.

How do spare parts work?

A kit of wear parts ships with your machine. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.

Customers Also Interested In...

Send Us Your Plate, Your Carton and Your Room Size

A linked line is sized around three things: your blister plate, your carton and your room. Send us all three, plus your count per carton. We’ll lay out the line, tell you your real cartons-per-minute figure, and tell you if two separate machines would serve you better.

  • Direct from our factory
  • Lead time confirmed in your quote
  • Installation and training available
  • Spare parts listed in your quote
Scroll to Top