Home » Tablet Counting and Bottling Lines for Supplements
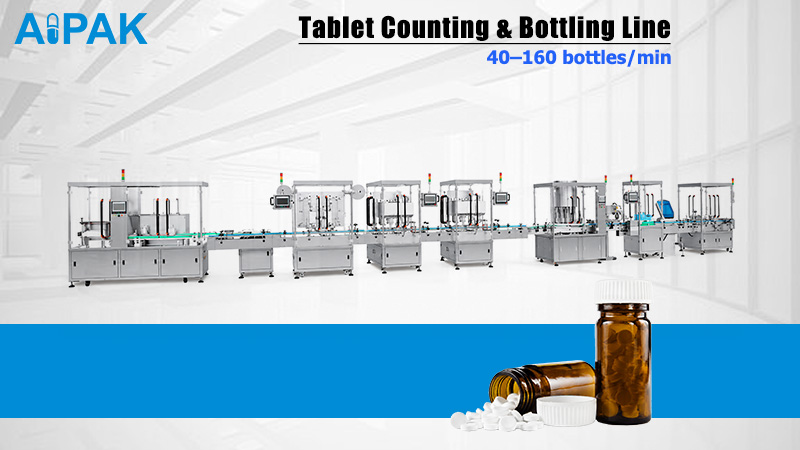
Tablet Counting & Bottling Line
You’re filling 60, 90 and 120-count bottles, and count accuracy still gets verified by hand. This line counts, fills, caps, induction-seals and labels in one pass.
- Output: 40 – 160 bottles / min
- Count accuracy: ≥98% infrared, ≥99.7% photoelectric
- Bottle diameter: Φ30 – 90 mm
- Changeover: 20–30 min
- Footprint: Under 30 m², 3 operators
We run your tablets, your bottles and your caps at FAT before the line ships — and you sign off before it leaves.
U.S. line: +1 (213) 526-8644 · 9 AM–7 PM China time, Mon–Fri
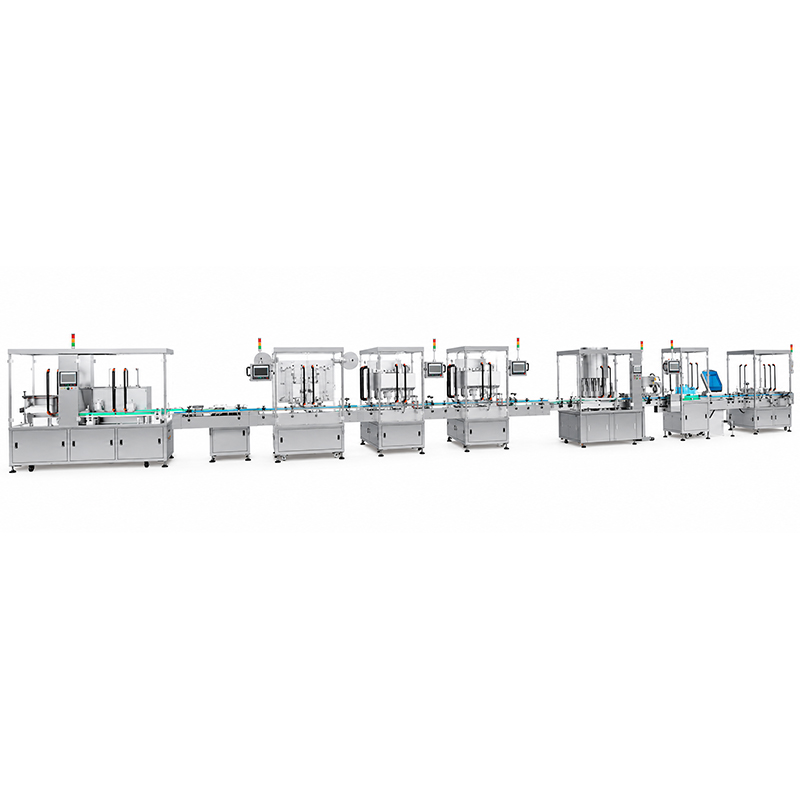
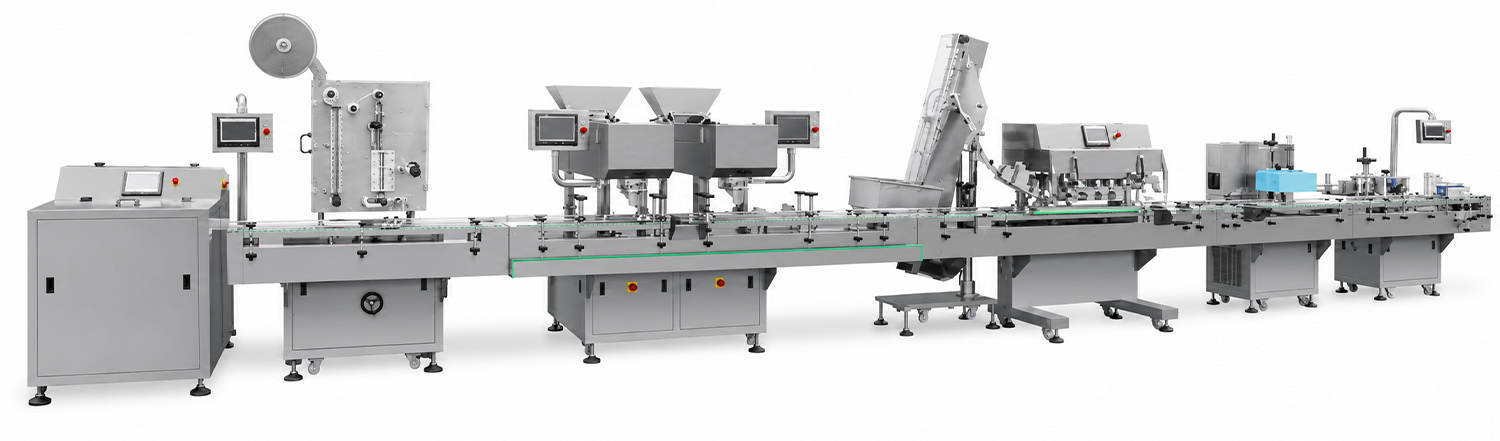
Five stations. Three operators.
A counting line is not one machine — it’s a chain, and the chain runs at the speed of its slowest station. Below is the standard configuration. Any station can be dropped if you already own it.
Bottle unscrambler
Bulk bottles in, upright and single-file out. Sets the pace for everything downstream.
Five models cover 15 to 750 ml at 20 to 160 bottles per minute. Which one your line gets depends on your bottle — its volume, its shape, and whether it’s glass. Round plastic bottles run on any of them; square and irregular shapes need the model built for that, and glass containers need the operator-fed feeder rather than an automatic one.
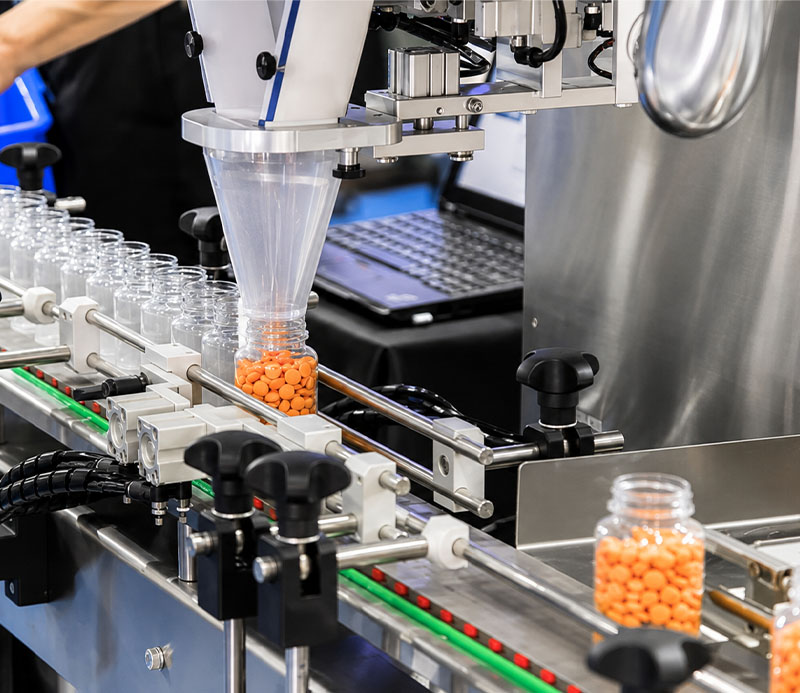
Counter & filler
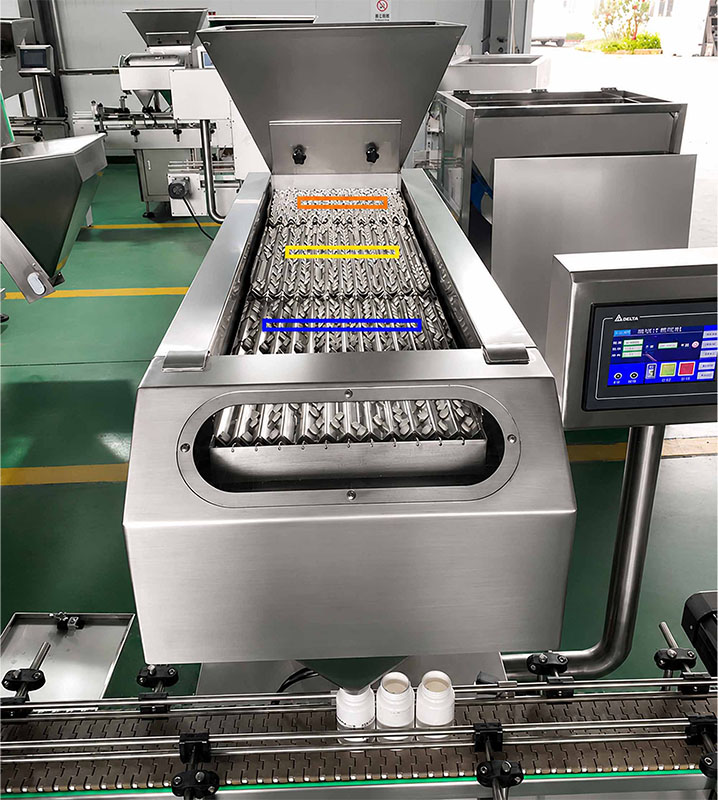
Electronic counting into the bottle. This is the station your QA will ask about.
Eight channel configurations from 8 to 48, covering 10 to 150 bottles per minute. Channel count is what sets your line speed — and it is the one decision on this line that cannot be revisited later, because every station after it is timed to the counter.
Infrared scanning holds ≥99.98% count accuracy; photoelectric detection ≥99.7%. Which sensing your line gets depends on your product, not on your budget.
Desiccant & capping
Desiccant insertion, then cap feeding and torque-controlled tightening.
Two machines, running back to back. The desiccant inserter places the absorber on top of the product at 50 to 200 bottles per minute depending on outlet configuration. The capper then applies the closure — by rotation for threaded caps, by vertical press for snap-on caps, or by press-and-rotate for child-resistant closures. Those are three different machines; your closure decides which.
The capper also does something the sealer downstream cannot: it detects bottles arriving without a foil liner in the cap. Once the cap is on, nothing further down the line can see inside it.
Induction sealing
Foil seal to the bottle land. Rejects at this station are usually a cap or land problem, not a sealer problem.
That sentence is worth reading twice, because it is where most seal troubleshooting goes wrong. The sealer bonds a liner that is already inside the cap — it does not add one. If the seal fails, the cause is usually the liner specification, a contaminated or nicked bottle land, or capping torque, before it is the sealer.
Two models: air-cooled for bottle mouths 15 to 50 mm at up to 120 bottles per minute, water-cooled for mouths up to 150 mm at up to 200. Above 120 bottles per minute on a continuous shift, air cooling drifts.
Labeling
Wrap-around or front-and-back, with date and lot coding.
Four models, chosen by container shape rather than by speed. Round bottles roll under the roller and take a wrap-around label. Square containers are indexed face by face, two to four faces. Flat surfaces are labeled from above. Small vials are laid horizontally.
This is the last station, and the only one whose output your customer reads before they open the product.
Two stations most lines don't need — and some do
Bottle air cleaner: Sits between the unscrambler and the counter. Ionised air neutralises static and a sealed vacuum draws moulding dust and transit debris out of the empty bottle. Worth adding if your bottles arrive in bulk bags rather than sealed cases, or if a visible particle in a finished bottle would be a complaint rather than an annoyance.
Cotton or rayon inserter: Sits alongside the desiccant station. Fill material stops tablets moving in a part-filled bottle — without it, a half-full bottle arrives with chipped edges and dust at the bottom. One number to know before you plan around it: our cotton inserter runs at 30 to 50 bottles per minute, which is slower than every other station on this line. If your line target is above that, the answer is rayon at up to 160, a second station in parallel, or a lower line speed. All three are workable; all three are cheaper to choose now.
The numbers your engineer will check first
Line-level figures below. Station-level detail is in the spec sheet — ask and we’ll send the full document.
| Parameter | Mid-speed line | High-speed line |
| Output | 40 – 100 bottles / min | 70 – 160 bottles / min |
| Counting channels | 16 | 32 |
| Count accuracy | ≥99.9% (IR ≥99.98%, photoelectric ≥99.7%) | ≥99.9% (IR ≥99.98%, photoelectric ≥99.7%) |
| Bottle diameter range | Φ30 – 90 mm | Φ30 – 90 mm |
| Bottle height range | Under 180 mm | Under 180 mm |
| Bottle volume range | 50 – 300 ml | 15 – 500 ml |
| Bottle material | HDPE, PET | HDPE, PET |
| Bottle shapes | Round | Round, square, flat-square, irregular |
| Product forms | Tablets, hard capsules 00–5, softgels, pills, gummies | Same |
| Product size range | Φ5.5 – 22 mm tablets, Φ3 – 20 mm pills | Same |
| Changeover time | 15-45 min | 15-45 min |
| Line footprint (L × W) | 10,000 × 2,500 mm | 11,500 × 2,500 mm |
| Packing room required | Under 30 m² | Under 30 m² |
| Operators | 3 | 3 |
| Total power | 4.5 kW | 8.0 kW |
Power supply | Wired for your U.S. supply, 208 V or 480 V, 60 Hz | Wired for your U.S. supply, 208 V or 480 V, 60 Hz |
| Compressed air | 1.0 m³/min | 1.5 m³/min |
| Cooling water | Not required | Not required |
| Control system / HMI | Touchscreen with PLC | Touchscreen with PLC |
| Product-contact materials | 304 stainless steel | 304 stainless steel |
What this line handles — and when it's the wrong machine
Most of the bad purchases we see aren’t bad machines. They’re the right machine bought for the wrong job. Read the right-hand column before you read the specs.
This line is built for
- Coated and uncoated tablets, round or oblong
- Hard capsules, sizes #00 to #5
- Softgels — transparent and opaque
- Gummies with the PTFE-lined channel option
- Round HDPE and PET bottles, 15 to 500 ml
- Plants running 2–20 SKUs on one line
Buy something else if
- You're bottling by weight, not by count. Powders and heavy-fill products need a net-weigh filler — this line counts pieces.
- Your bottles are square, oval or glass. The unscrambler and labeler both change, and glass needs an operator-fed unscrambler. Tell us before you quote.
- You need DSCSA serialization. That's a prescription-drug requirement. This line is built for dietary supplements — ask us before you assume.
- You're under 2,000 bottles a day. A semi-automatic counter plus manual capping will cost you far less and pay back faster.
- Your gummies are uncoated and tacky. They bridge in a standard channel feeder. Send us a sample before you buy anyone's line.
If you run more than five SKUs, this is the number that decides
Throughput sells machines. Changeover time decides what a line actually produces in a week. Four questions we ask before quoting yours.
If only the count changes, it’s a recipe change on the HMI — 15-45 minutes. If the bottle changes, you’re changing unscrambler tooling, guide rails, the capping chuck and the label recipe. Those are four different jobs at four different stations, and they should be quoted differently. A supplier who quotes you one number for both has not thought about it.
Tool-free matters more than it sounds. A wrench in the room means the changeover time depends on who’s holding it.
One thing we will not claim: the counting station’s change parts are not tool-free on every configuration. Ask us which stations are and which aren’t, and we’ll tell you before you order rather than after.
Our standard HMI can store up to 100 different recipes locally. This is usually more than enough to cover various combinations of bottles and products for daily production.
Yes. Change parts are machined in our own CNC shop, which is why a new bottle format doesn’t mean a new supplier. Lead time for an added format is written into your quote.
What your QA gets in the box
- Every line ships with the documents your QA team will ask for.
- IQ / OQ / PQ protocols
- Calibration records for the counting and torque devices
- Operating and maintenance manuals, in English
- Electrical schematics and pneumatic diagrams
- Spare parts list with part numbers and prices
- FAT protocol and signed FAT report
- CE Declaration of Conformity
- Material certificates to EN 10204 3.1 for product-contact parts
If your QA team needs another document, ask before you order. It’s easier to add it to the package than to produce it later.
Who picks up when the line stops
We’re not going to tell you we have a warehouse in New Jersey. We don’t. Here’s what we actually do, and you can hold us to it.
A U.S. number, answered by us
+1 (213) 526-8644, answered by our engineers 9 AM–7 PM China time, Monday to Friday. That's evening and overnight in the U.S., so leave a message or send a WhatsApp anytime and we'll pick it up first thing.
A wear-parts kit ships with the line
The wear parts you'll go through in year one, listed and priced in your quote before you sign.
Spare parts and lead times, in writing
Every part in the kit, and the lead time for anything outside it, is written into your quote — so you know before you have an emergency, not during one.
Change parts for new formats
Send us the bottle drawing and a sample of your product. We machine the change parts for the new format — funnels, bottle clamps and capping chucks — and test them before they ship.
Electrical spares sourced locally
Most electrical components on the line are international brands, which means many electrical spares can be bought in North America rather than shipped from China. We'll list which parts those are in your spare parts document.
Already own part of the line?
Any station can be bought on its own and integrated into what you’re running now. Tell us what’s already on the floor.
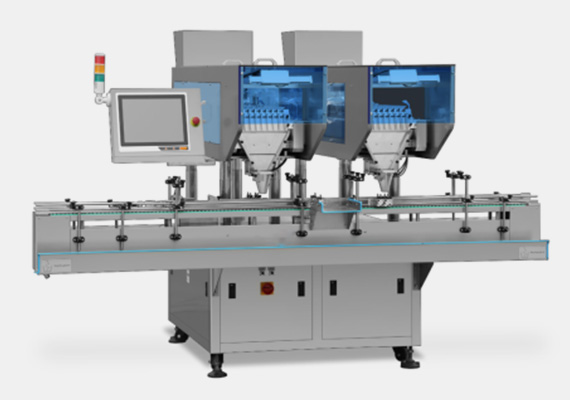
Tablet Counting Machine
Standalone counter · integrates with your existing line Eight models, 8 to 48 channels. The station most customers buy first.
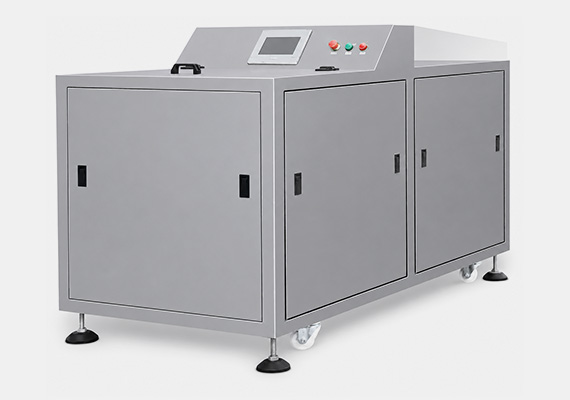
Bottle Unscrambler
Five models · 15 to 750 ml, plastic and glass The station most customers buy second, when hand-feeding becomes the constraint.
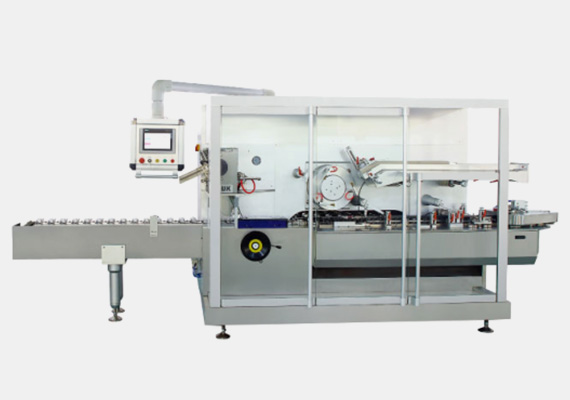
Cartoning Machine
The next machine most plants buy after this one Bottles into retail cartons.
Send us your bottle and your target rate
We’ll come back with a line configuration, a layout drawing and a price. If this line isn’t right for your product, we’ll tell you that instead.
- We reply within one business day.
- Free layout drawing with every quote
- We keep your formula and specs confidential.