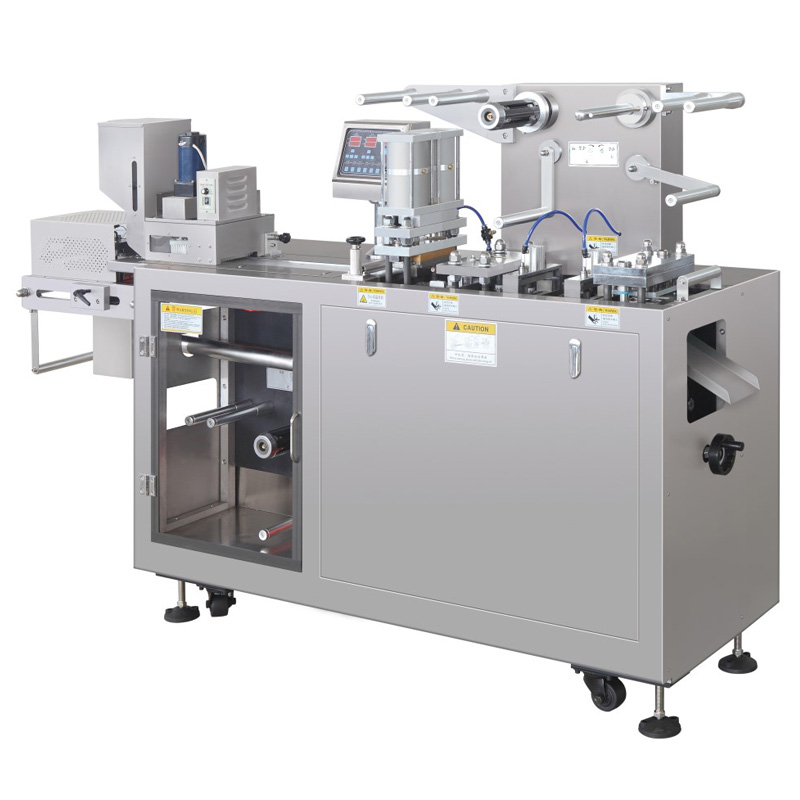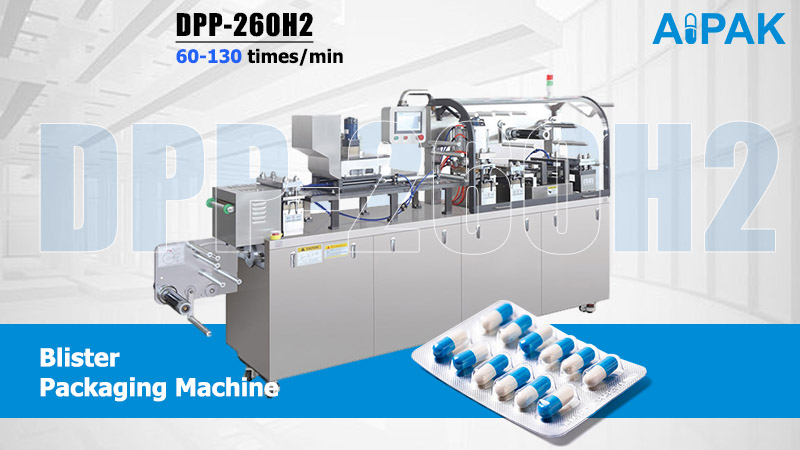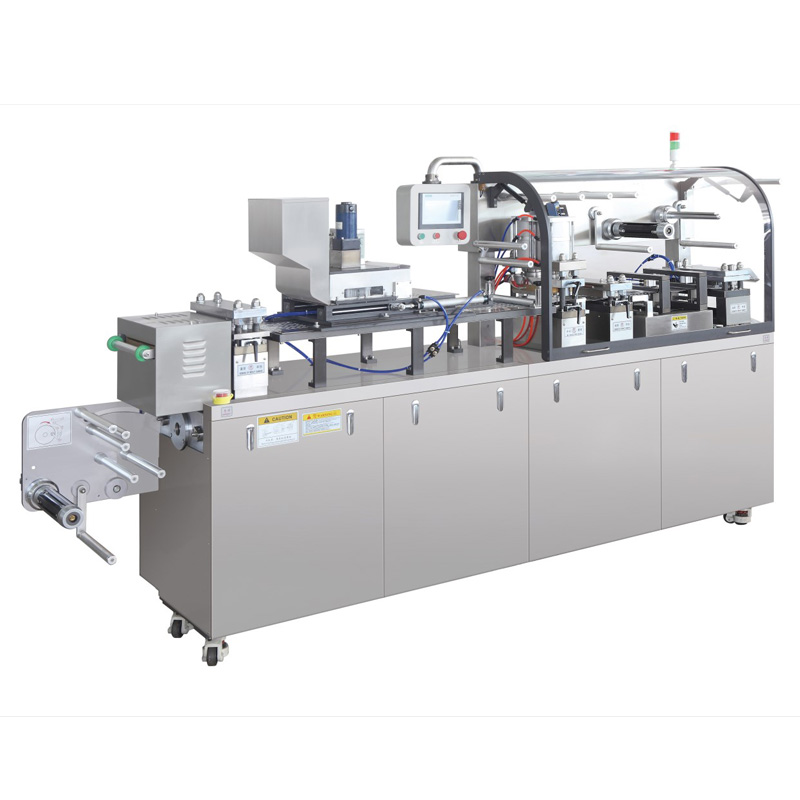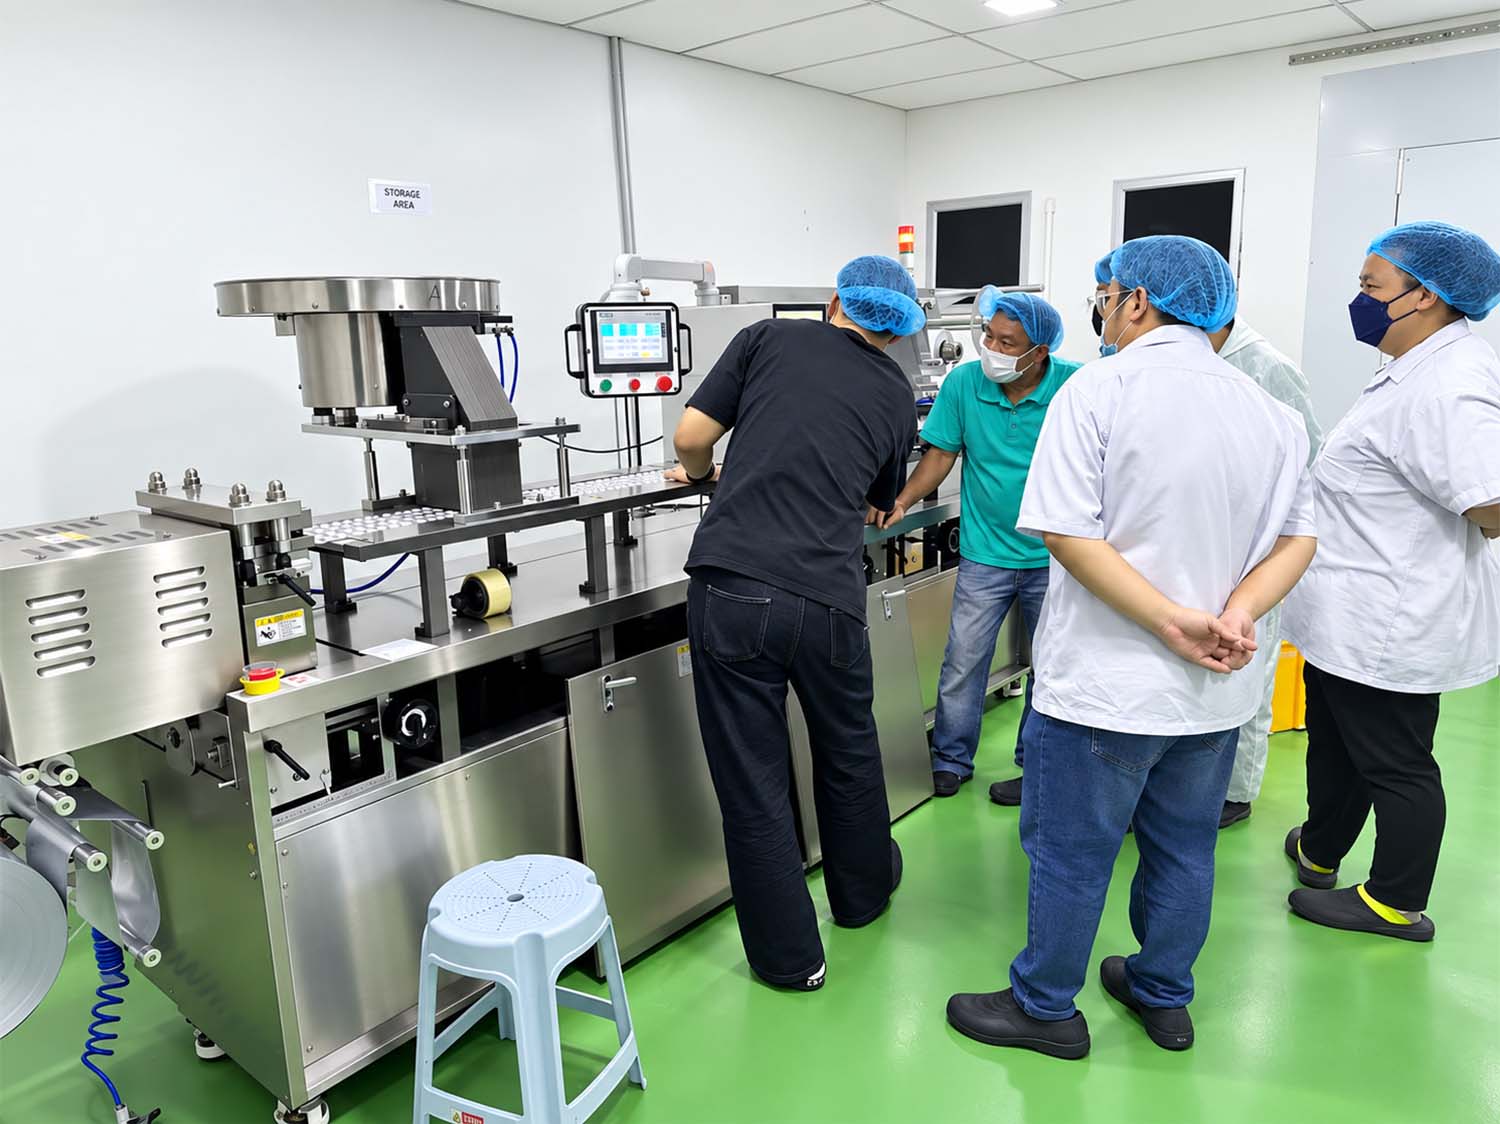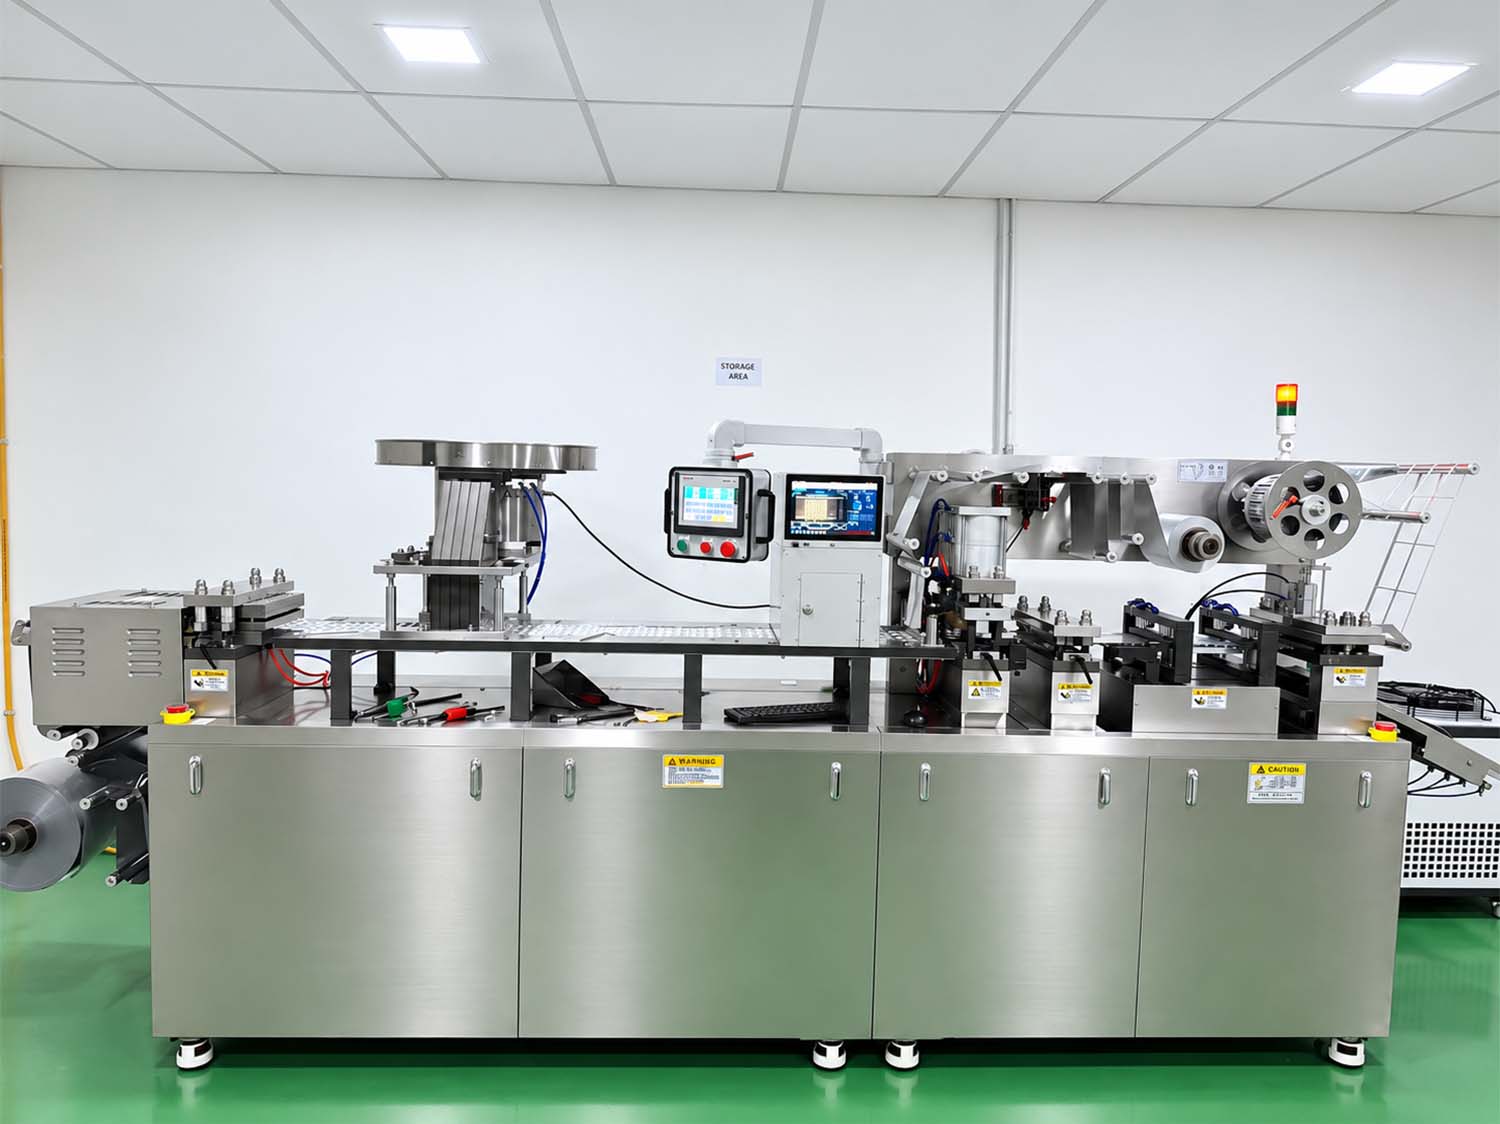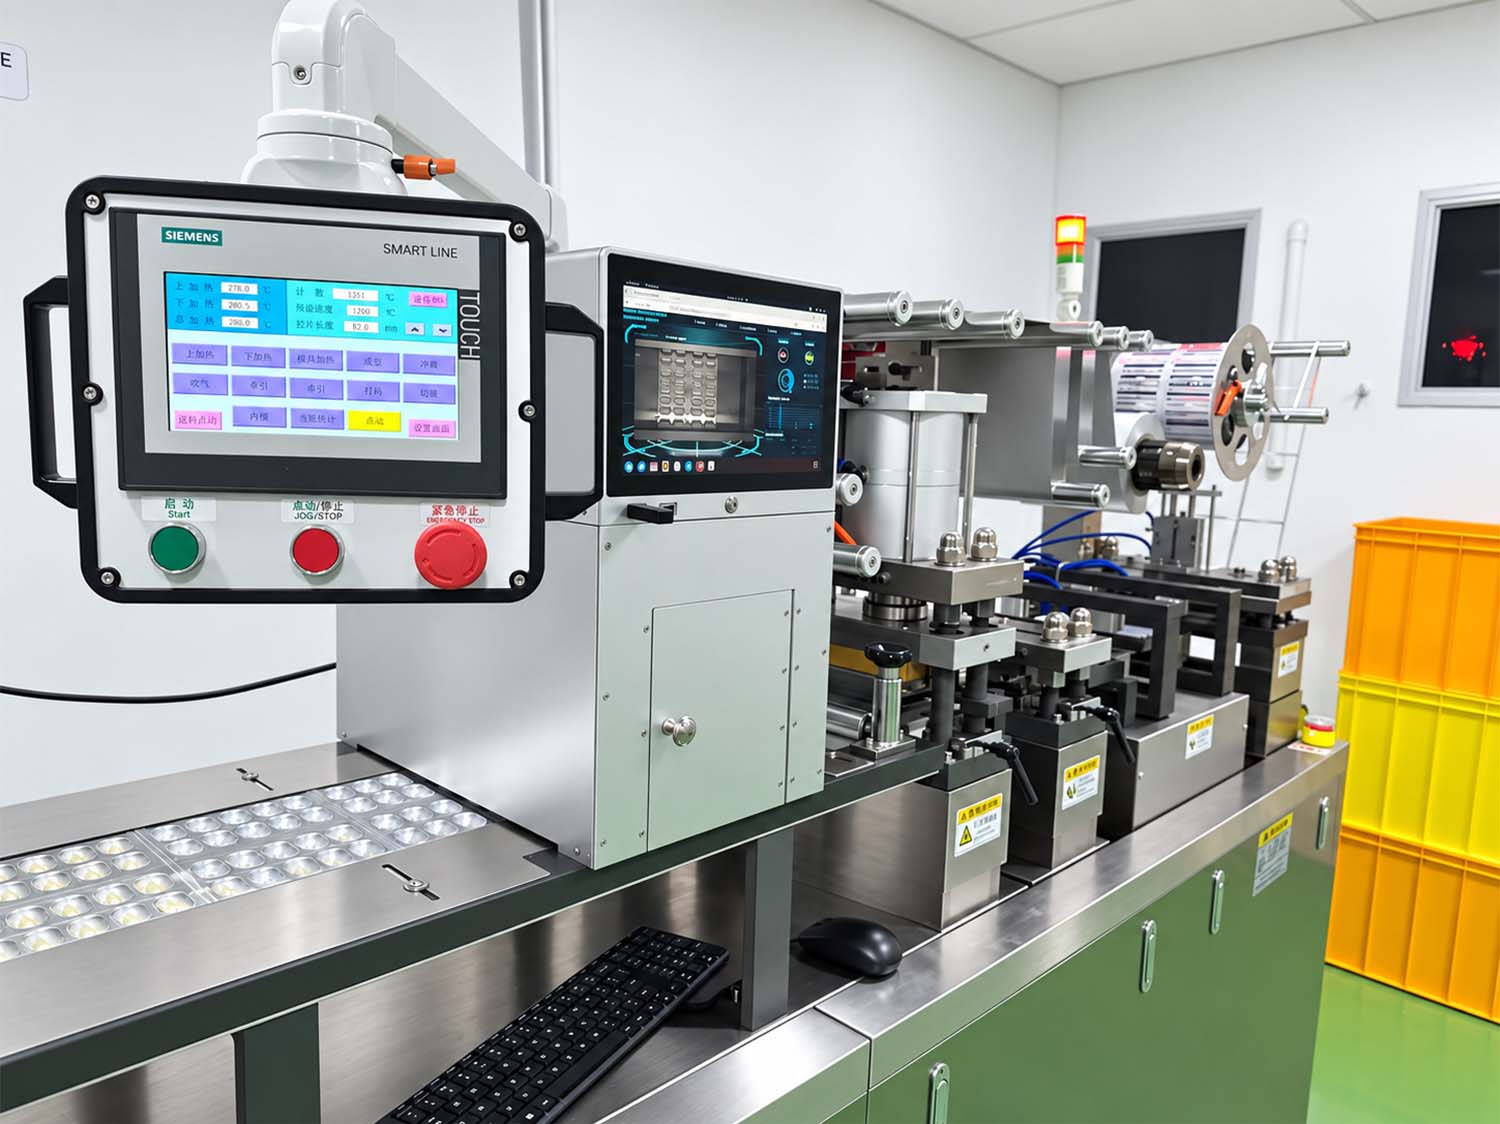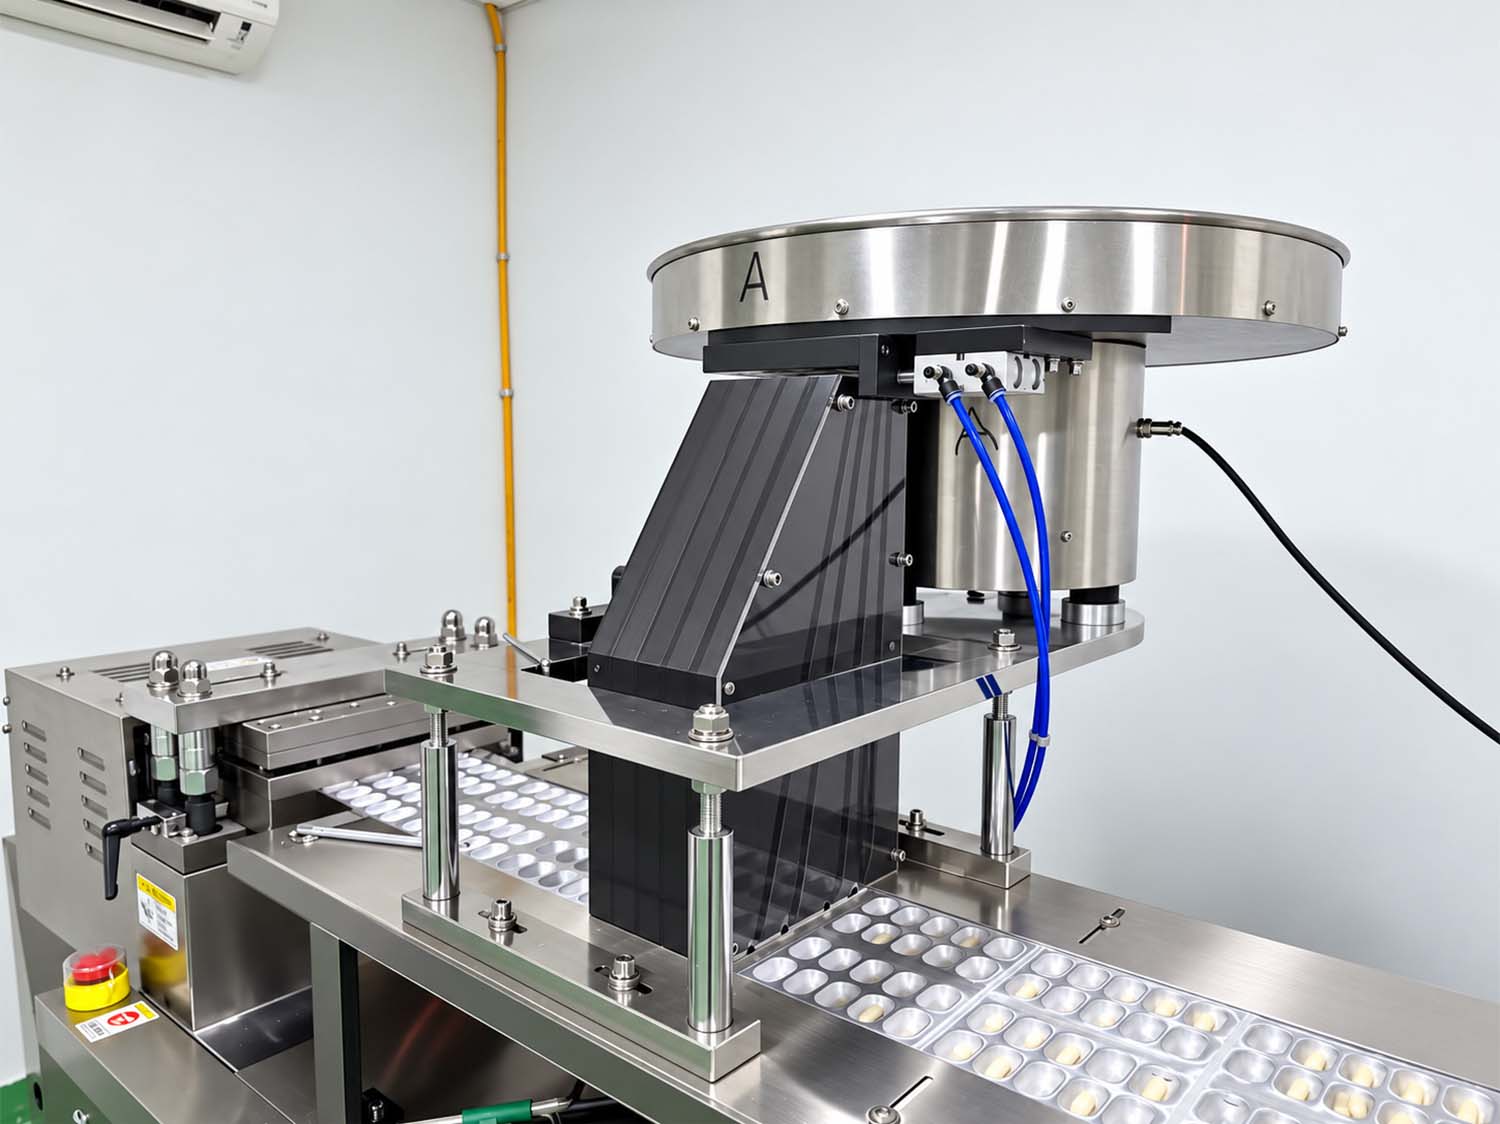
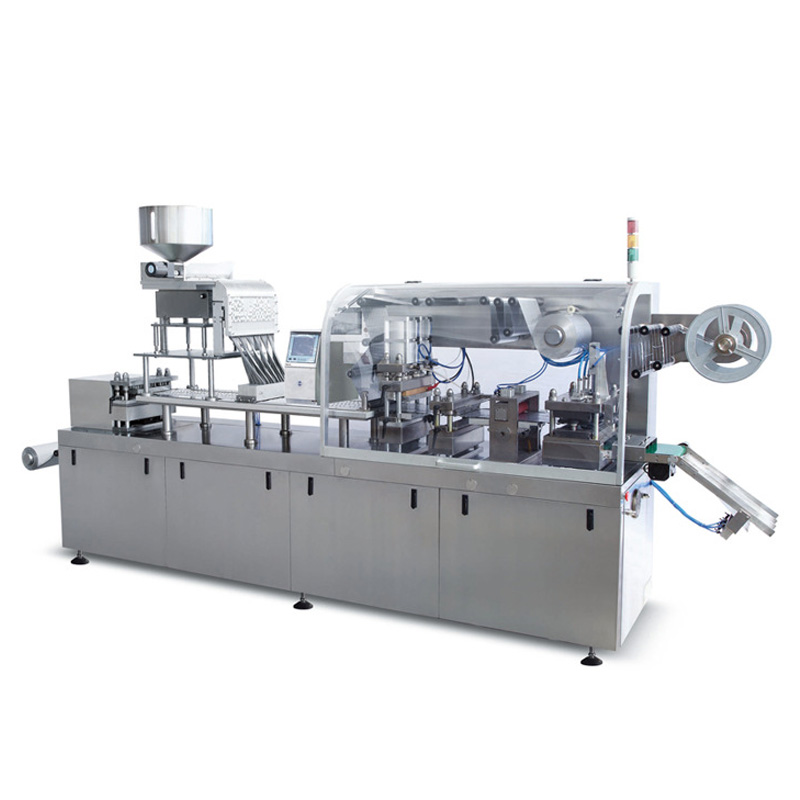
DPP-260H2 Rotary-Seal Blister Packaging Machine
Continuous roller sealing, 60 to 130 punches a minute, 28,800 plates an hour
Same 260 mm class as the DPP-260H1, but a different machine. This one seals with a continuously rotating knurled roller instead of a pneumatic platen. That’s what takes it to 130 punches a minute and 28,800 plates an hour. It also forms to only 12 mm — so it’s faster, and it’s not the machine for deep pockets.
1. Punch frequency: 60 to 130 times a minute
2. Output: 28,800 plates an hour (at an 80 × 57 mm plate)
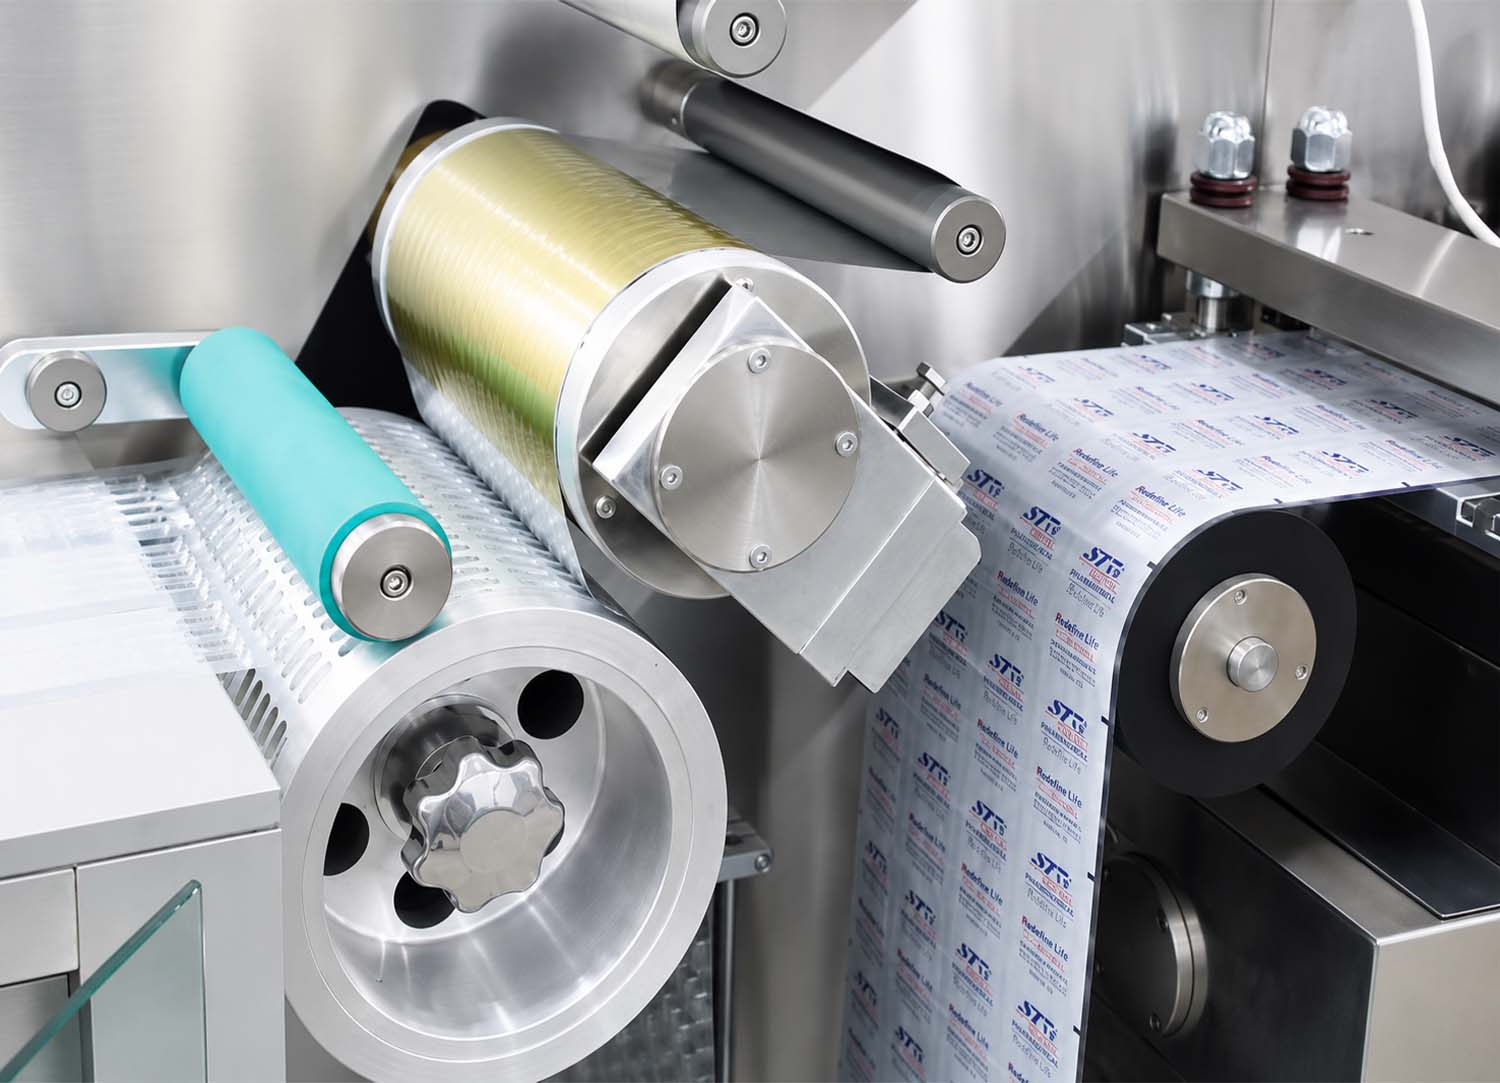
3. Continuous roller sealing: not intermittent platen sealing
4. Forming depth: 12 mm. Deeper items need the DPP-260H1
5. Power: 15 kW, twin 2 kW servo drives
Is this the right machine for you?
✓ Yes, if…
- You need more than 12,000 plates an hour
- Your pocket depth is 12 mm or less
- You run one or two formats continuously
- You have 4.5 m of line length and three-phase at 15 kW
- Foil cost matters — continuous forming leaves less waste between plates
✕ Buy something else if…
- Your item needs more than 12 mm of depth → large softgels and caplets need a flat-plate machine like the DPP-260H1. Send us the item height
- You need under 12,000 plates an hour → the DPP-260H1 costs less, draws less power and takes less floor
- You change format weekly → a gear-shift ratio change is more involved than swapping tooling on a flat-plate machine
- Your floor can't take 2,600 kg → check your floor loading before you order
Technical specification
| Feature | DPP-260H2 | What does it mean to you? |
|---|---|---|
| Punch frequency | 60–130 times/min | Roughly double the flat-plate machines |
| Output | 28,800 plates/hour | At 80 × 57 mm plate. Your plate size changes this |
| Sealing | Continuous knurled-roller | Not intermittent platen sealing — that’s where the speed comes from |
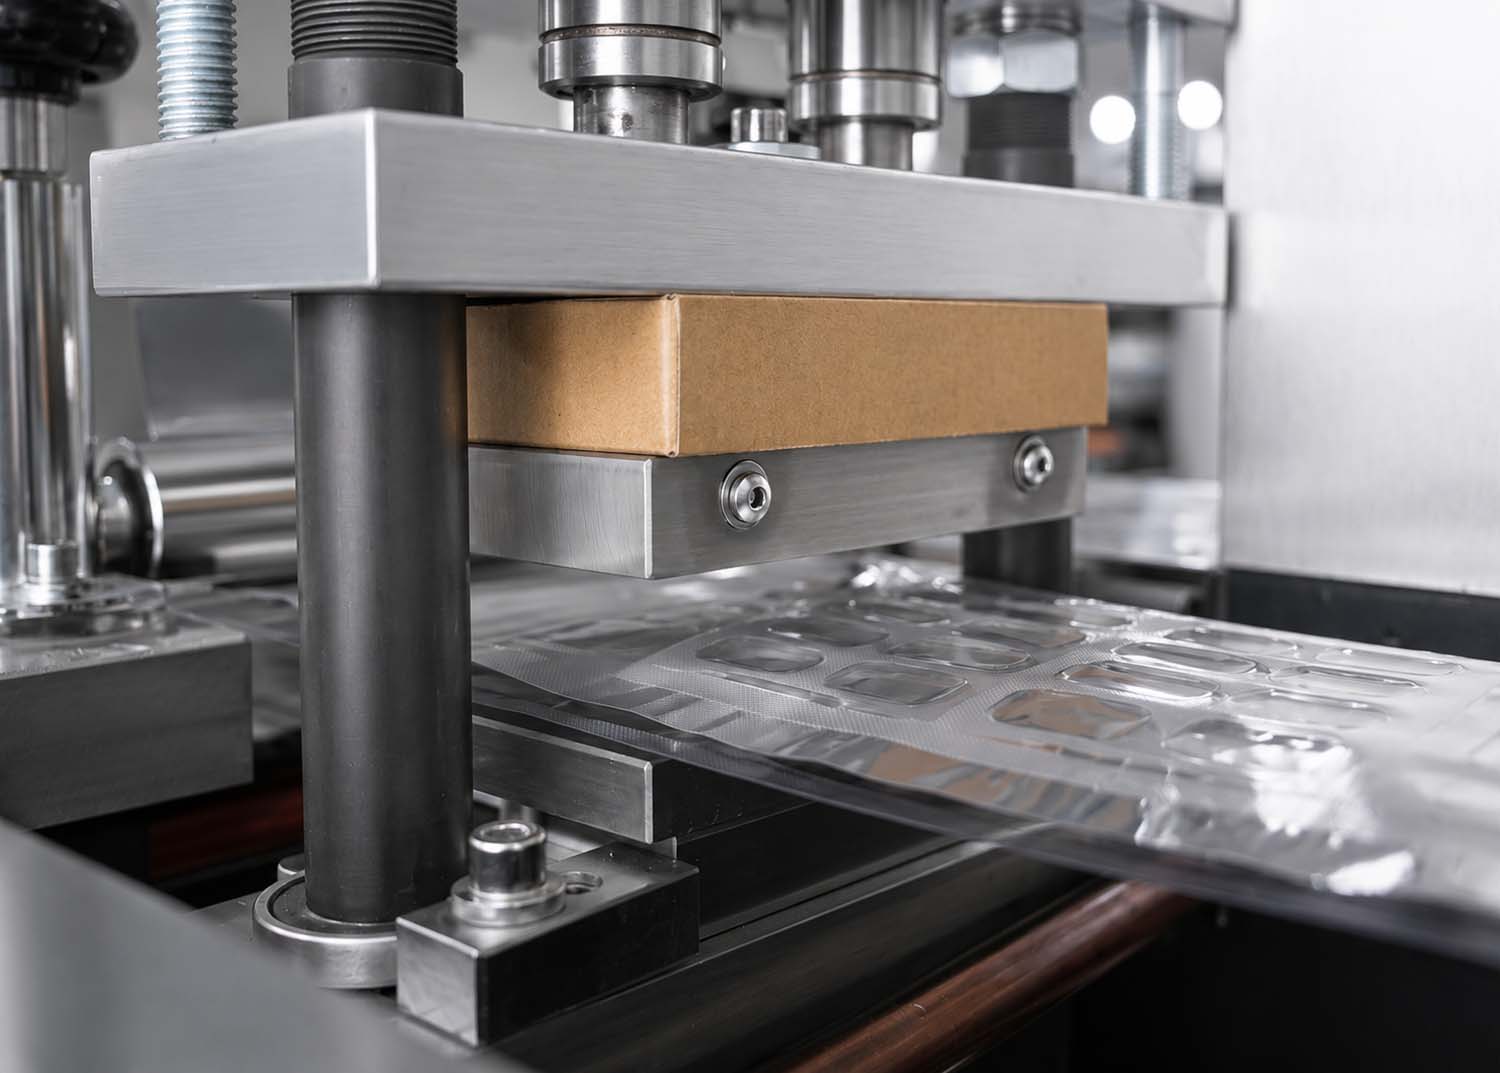
| Forming | Positive pressure against plate, 120 °C | Lower forming temperature than conventional platen forming |
| Forming area & depth | 240 × 240 × 12 mm | Half the depth of the DPP-260H1. Check your item height first |
| Forming traction stroke | 100–250 mm | — |
| Cutting traction stroke | 20–100 mm | — |
| Main servo motors | 2 + 2 kW | — |
| Total power | 15 kW, three-phase, 60 Hz. Built to your U.S. supply; we confirm the voltage with your quote | — |
| Air pressure | 0.5–0.7 MPa | Higher than the flat-plate range |
| Air consumption | 20 L/min | — |
| PVC film | 0.25–0.50 × 260 mm | Max roll diameter Φ400 |
| PTP foil | 0.02–0.035 × 260 mm | Max roll diameter Φ280 |
| Dimensions | 4,500 × 950 × 1,620 mm (L×W×H) | — |
| Weight | 2,600 kg | Check your floor loading |
Model comparison
Model | Type | Punch freq. | Output | Forming area | Power |
DPP-80 | Flat plate | 10–33 times/min | 1,980 plates/hour | 80 mm | 2.4 kW |
DPP-120H | Flat plate | 10–35 times/min | 2,400–4,200 plates/hour | 120 mm | 4.5 kW |
DPP-150E | Flat plate | 10–40 times/min | 3,600–7,200 plates/hour | 150 mm | 6.5 kW |
DPP-180H | Flat plate | 10–50 times/min | 4,800–9,600 plates/hour | 180 mm | 8.5 kW |
DPP-260H1 | Flat plate | 10–50 times/min | 6,000–12,000 plates/hour | 260 mm | 9.5 kW |
DPP-260H2 | Rotary seal | 60–130 times/min | Up to 28,800 plates/hour | 260 mm | 15 kW |
DPH-260H | Rotary | 80–150 times/min, 200 max | 6,000–18,000 plates/hour | 260 mm | 24 kW |
DPH-380H | Rotary | 40–180 times/min, 200 max | Up to 45,000 plates/hour | 380 mm | 28 kW |
Flat plate and rotary are two different machines, not two speeds of one. Flat plate stretches the film against a mold with positive air pressure and a mechanical punch. Rotary forms and seals on a drum with line contact. The difference shows up in material waste, changeover time and what the machine costs you per plate — the table above shows where each one fits.
Gear-Shift Forming-to-Cutting Ratio
A shiftable gear transmission changes how many forming strokes happen per cutting stroke. Form three plates lengthwise and the ratio is 1:3; form four and it’s 1:4. That’s where 28,800 plates an hour comes from — not from punching faster, but from forming more per stroke.
Continuous Roller Sealing
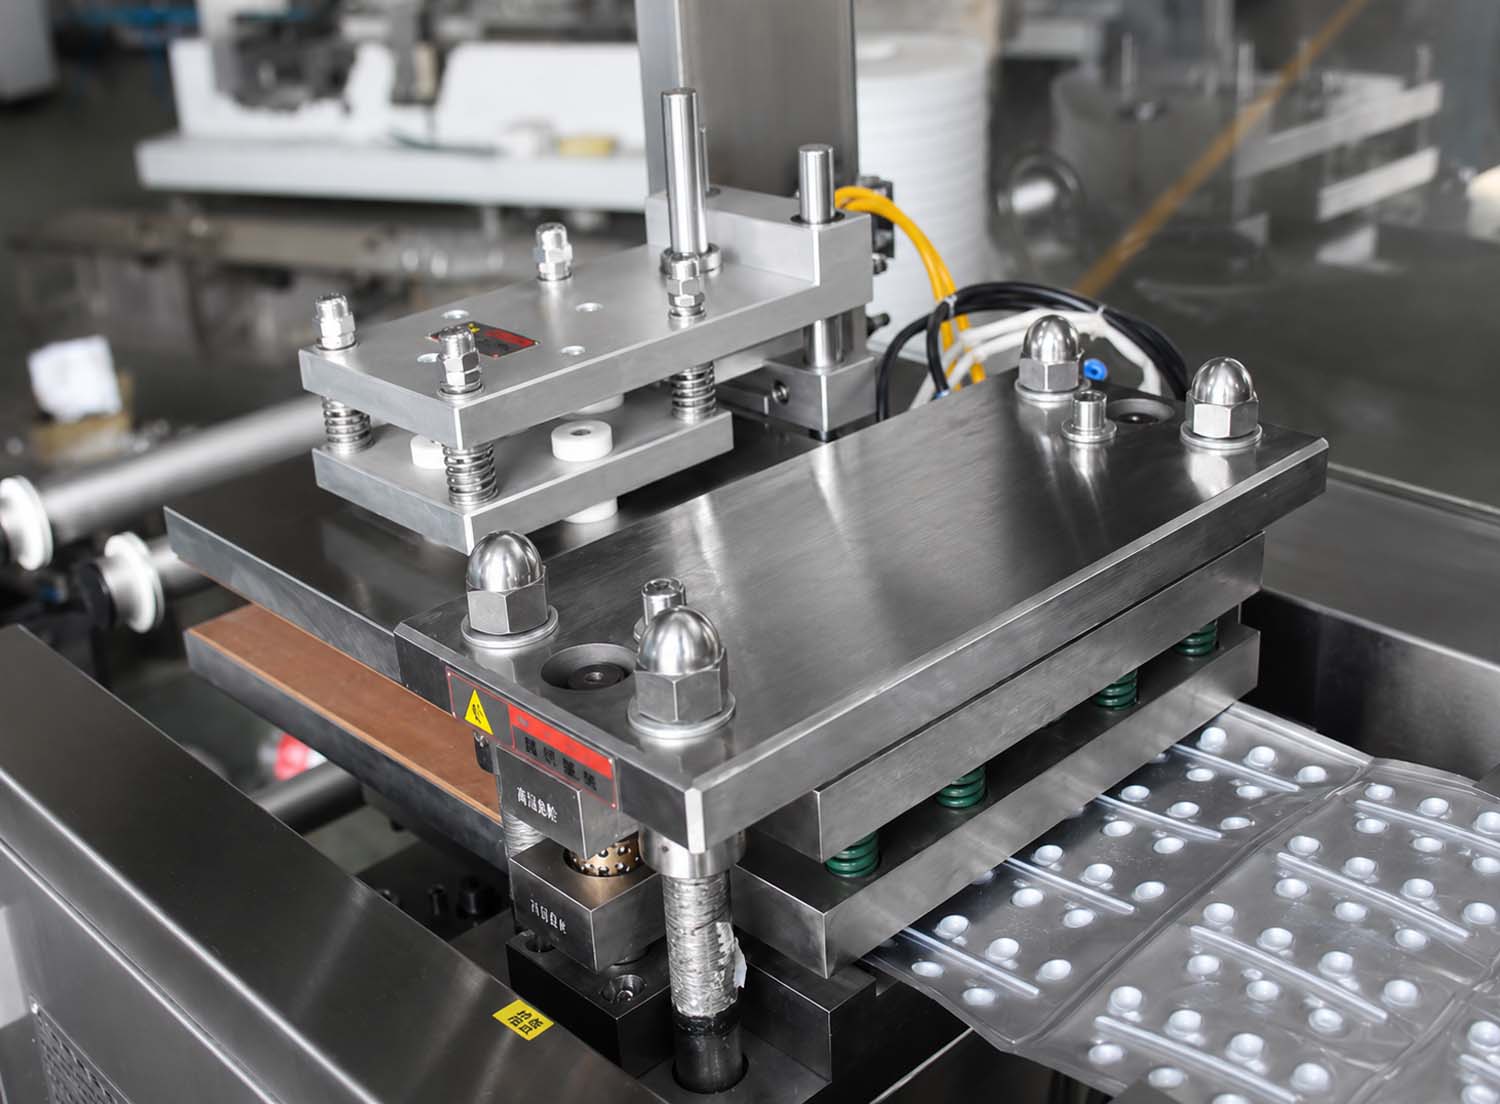
A knurled roller rolls across the seam continuously instead of a platen pressing down and lifting. Line contact rather than area contact, and no dwell-and-release cycle. It’s the main reason this machine runs at up to double the rate of a flat-plate machine.
Positive-Pressure Forming at 120 °C
Pockets are formed by air pressure against a plate at 120 °C. Lower forming temperature than a conventional platen machine, which means less energy and a crisper pocket wall.
Less Waste Between Plates
Continuous forming and sealing leave a narrower margin between plates than an intermittent machine does. On cold-formed Alu-Alu, where the foil costs several times what Alu-PVC does, that margin is where the money is.
Twin Servo Drives
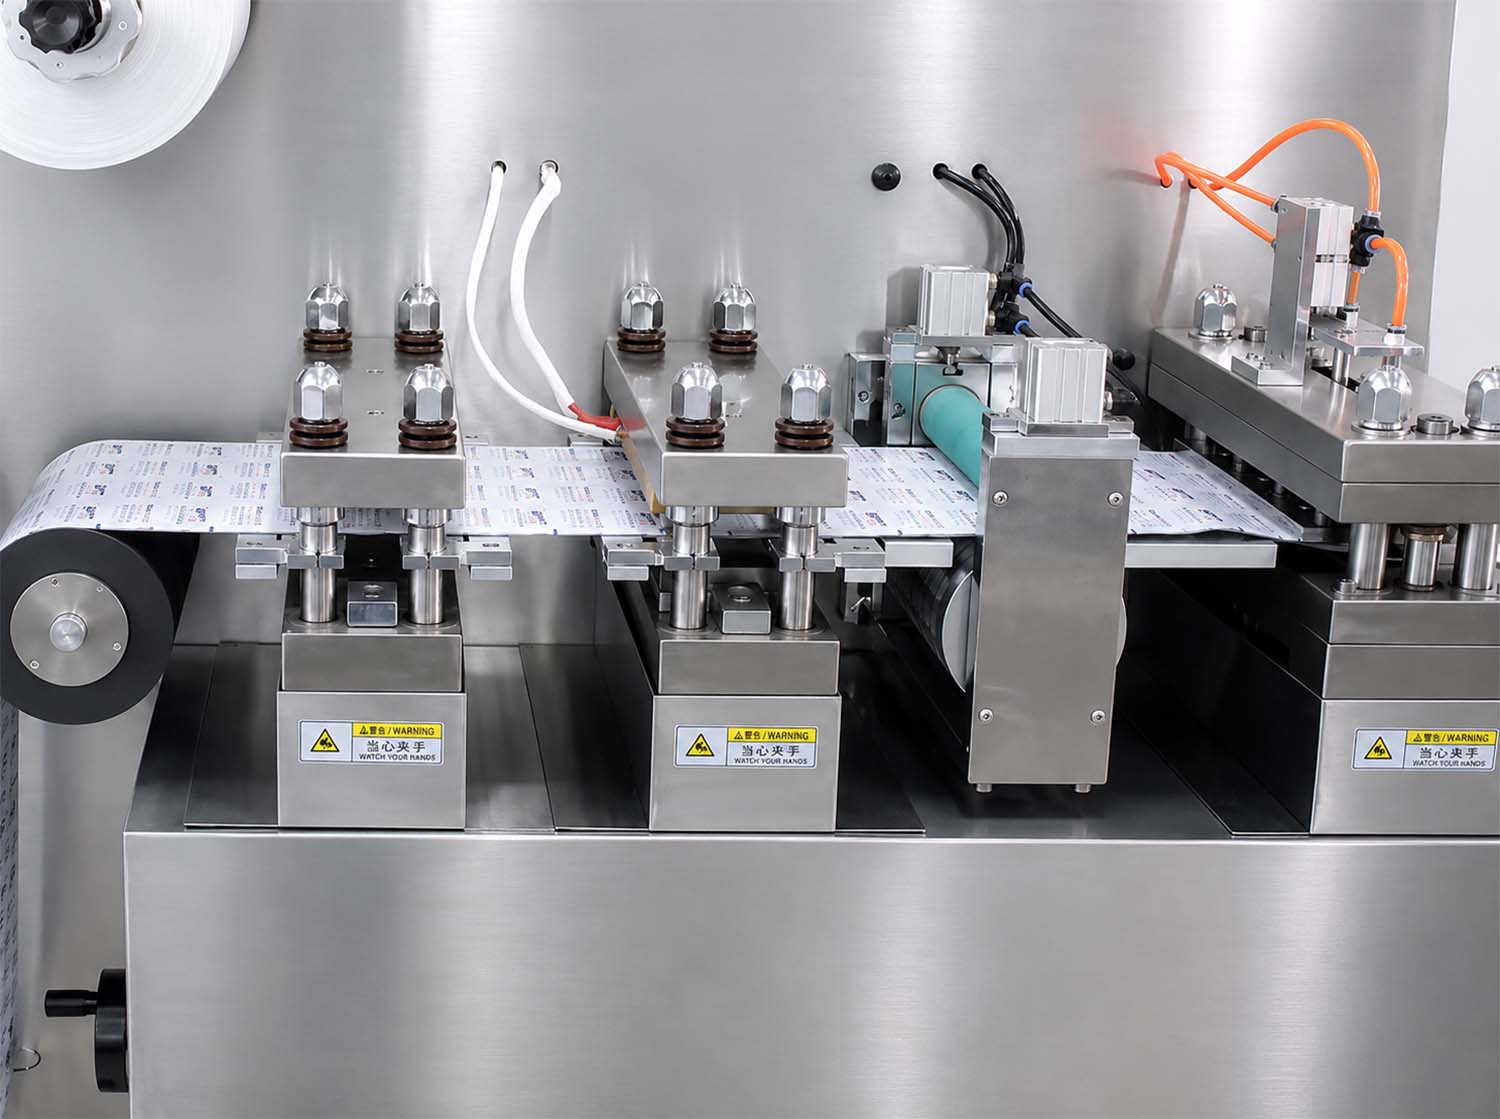
Two 2 kW servo motors drive forming and cutting independently. At 130 punches a minute a single-motor machine accumulates timing error across a shift; independent drives don’t.
12 mm Forming Depth
This is a limit, not a feature, and it’s worth stating plainly. Continuous roller forming trades depth for speed. If your item is taller than 12 mm, the flat-plate DPP-260H1 is the machine.
Industry Applications
A rotary-seal machine pays back on long runs of shallow items. These are the products it’s built for:
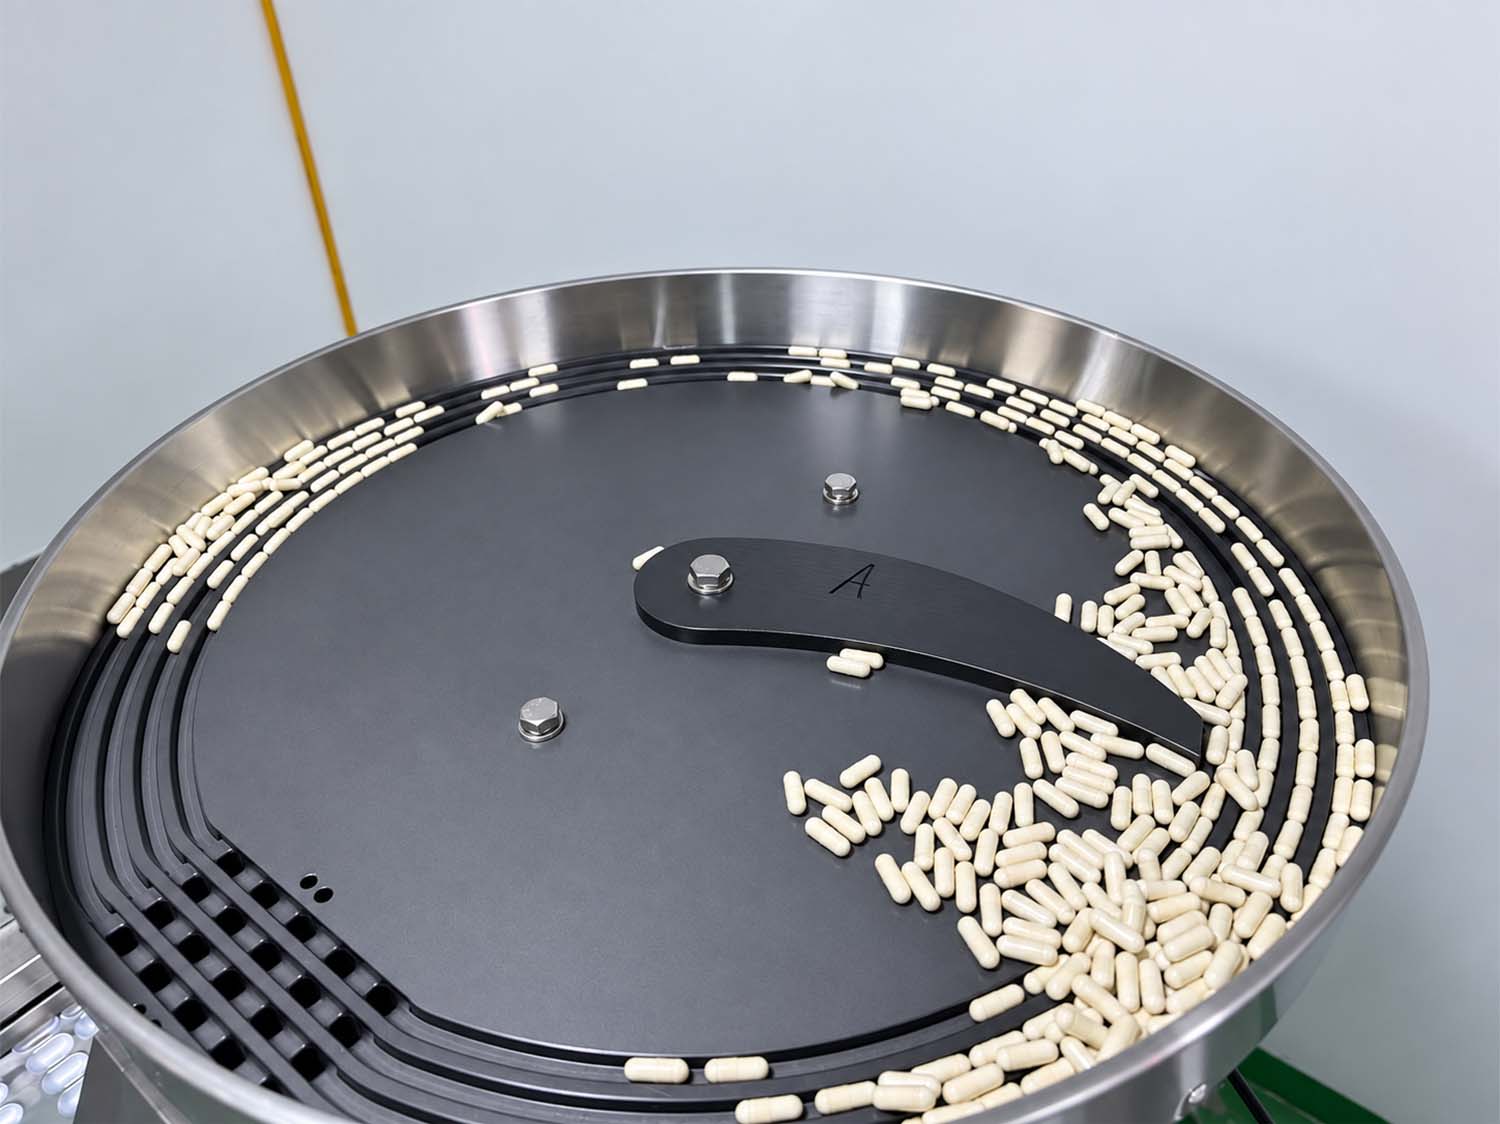
Flat tablets and standard capsules at volume
Items under 12 mm tall in continuous production. This is what the machine is built for.
Cold-formed Alu-Alu at high output
Alu-Alu costs several times what Alu-PVC does. At 28,800 plates an hour the narrower plate margin is a real line item, not a rounding error.
Single-SKU continuous runs
One format running across shifts. A gear-ratio change is more involved than swapping flat-plate tooling, so this machine pays back on long runs rather than frequent changes.
Chewable and effervescent tablets
Flat chewables and effervescent tablets in long runs. Shallow pockets, high volume, and the same 12 mm ceiling applies.
What changing over involves
A format set is four stations, not one part.
What changed | What you adjust | Roughly |
Same format, new batch | Nothing | — |
Plate layout changes | Forming, sealing, embossing and cutting tooling | 15–45 minutes |
Plates per forming stroke changes (1:3 → 1:4) | Gear ratio on the shift transmission, plus tooling | 15–45 minutes |
Alu-PVC → Alu-Alu | Tooling and feeder. Punch rate drops to ≤40 | Not a changeover |
A rotary machine trades changeover speed for running speed. If you switch format more than once a week, the flat-plate DPP-260H1 will cost you less in downtime than this machine saves you in output.
What to check before you buy
The tooling, not the machine
A format set covers four synchronized stations. Ask any supplier who designs the pocket layout, how long a new format takes to make, and what it costs. That's where a blister project succeeds or fails.
The feeder, before you order
An Alu-PVC universal feeder cannot run cold-formed Alu-Alu, and it cannot be converted afterwards. Ask which feeder you're being quoted and what it locks you out of.
Installation and training
Ask what's included and what costs extra. The answer varies more between suppliers than the machine price does.
Why Choose AIPAK?
One Point of Contact
One project engineer handles your machine from proposal to commissioning, so you’re not chasing five suppliers for one answer.
We Design the Pocket Around Your Product
Send us your tablet or capsule samples and tell us your foil. We design the pocket layout and specify the feeder before we quote, because an Alu-PVC universal feeder can’t be converted to Alu-Alu later.
A U.S. Number, Answered by Us
+1 (213) 526-8644, answered by our engineers 9 AM–7 PM China time, Monday to Friday. That’s evening and overnight in the U.S., so leave a message or send a WhatsApp anytime and we’ll pick it up first thing.
Spare Parts and Lead Time, in Writing
A kit of wear parts ships with your machine. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.
DPP-260H2 Blister Packaging Machine FAQ
Not by punching faster than the gears allow. A shiftable transmission sets how many forming strokes happen per cutting stroke — form four plates lengthwise and cut them in one pass, and the ratio is 1:4. Combined with continuous roller sealing instead of an intermittent platen, that’s where the rate comes from.
Continuous roller forming trades depth for speed. The film has less dwell time against the mould, so it stretches less far. If your item is taller than 12 mm — large softgels or caplets — the flat-plate DPP-260H1 is the machine. We’d rather tell you now than at the factory acceptance test.
Yes, with the right tooling and feeder. Note that Alu-Alu forms more slowly than Alu-PVC on any machine — plan your output on the Alu-Alu figure, not the headline one.
Different machines, same width class. The H1 seals with a pneumatic platen and forms deeper pockets. This one seals with a continuous roller, forms to 12 mm, runs to 130 punches a minute and draws 15 kW. Depth and changeover frequency usually decide it before speed does.
4,500 × 950 mm, 2,600 kg, 15 kW three-phase, 0.5 to 0.7 MPa compressed air.
Yes. We build to your U.S. supply at 60 Hz and confirm the voltage with your quote.
A kit of wear parts ships with your machine. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.
Customers Also Interested In...
Send us your item height first
This machine forms to 12 mm. That one number rules out more enquiries than speed or budget does — and it’s the one buyers check last.
Send us a sample tablet or capsule, or just its height in millimetres. If it’s over 12 mm we’ll point you at the flat-plate machine instead, and say so in the first email rather than the fifth.
- Direct from our factory
- Lead time confirmed in your quote
- Installation and training available
- Spare parts listed in your quote