APC-GM600Q Gummy Production Line — 600 kg/h
The largest line we build
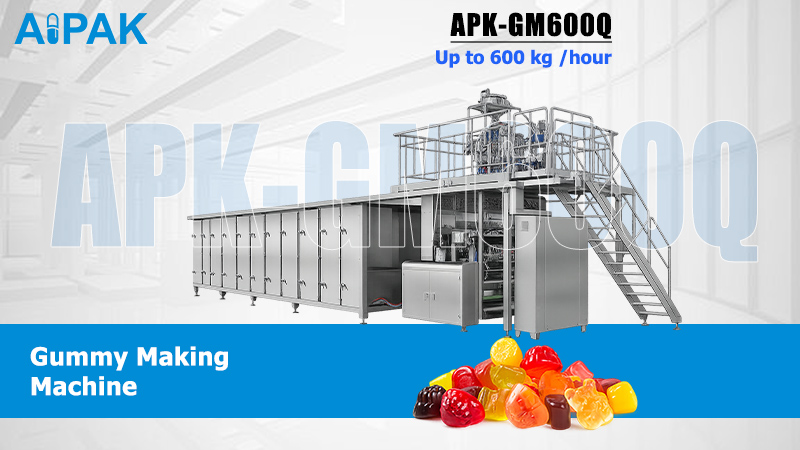
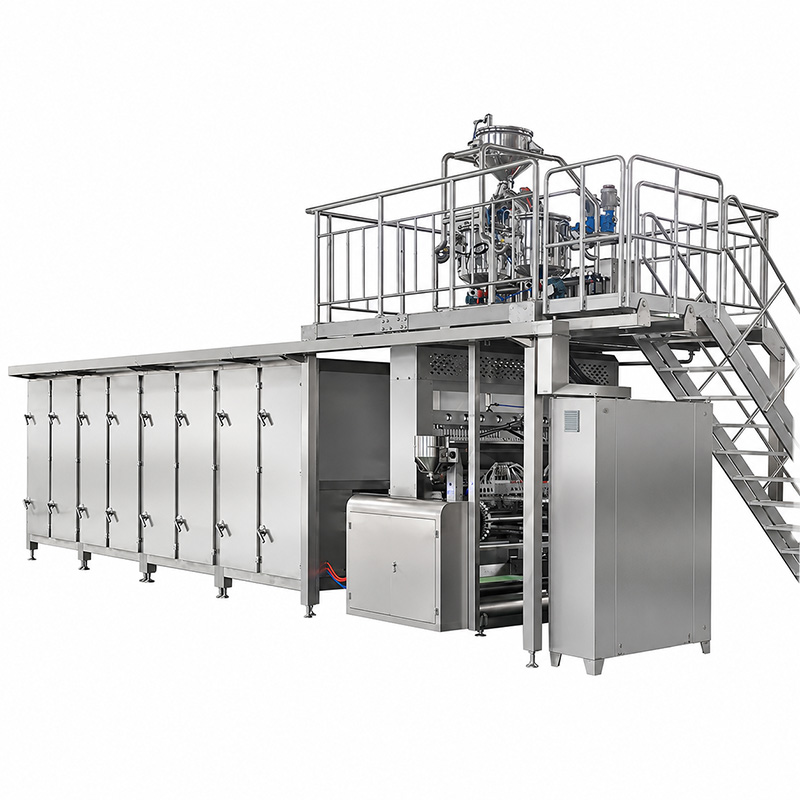
One product running continuously, where the line is what limits your month. The GM600Q runs 600 kilograms an hour — twice the GM300Q — in 20 meters of floor. It also asks the most of your plant: 85 kW and 500 kg/h of steam at 1.6–1.8 MPa.
1. Output: 600 kg/h, the highest we build
2. Line length: 20 m, only 2 m more than the GM300Q for twice the output
3. Utilities: 85 kW, 500 kg/h steam at 1.6–1.8 MPa, 0.3 m³/min air
4. Weight: 5,000 kg. Check your floor loading
Is this the right line for you?
✓ Yes, if…
- You run one or two products at mass-market volume
- You need more than 300 kg an hour
- You have steam at 1.6–1.8 MPa — the highest pressure in the range
- Your floor takes 5,000 kg and 20 meters
✕ Buy something else if…
- You change shapes weekly → more capacity means more molds to swap. The GM300Q is built around changeover
- Your volume is under 400 kg an hour → the GM300Q costs less and won't sit idle
- Your boiler can't reach 1.6 MPa → this is the binding constraint on this line, more often than floor space is
- You can't hold the room conditions across a bigger footprint → the bigger the line, the harder the humidity is to hold. Send us your room and your current HVAC and we'll tell you honestly
Full-Servo Screw-Driven Depositing
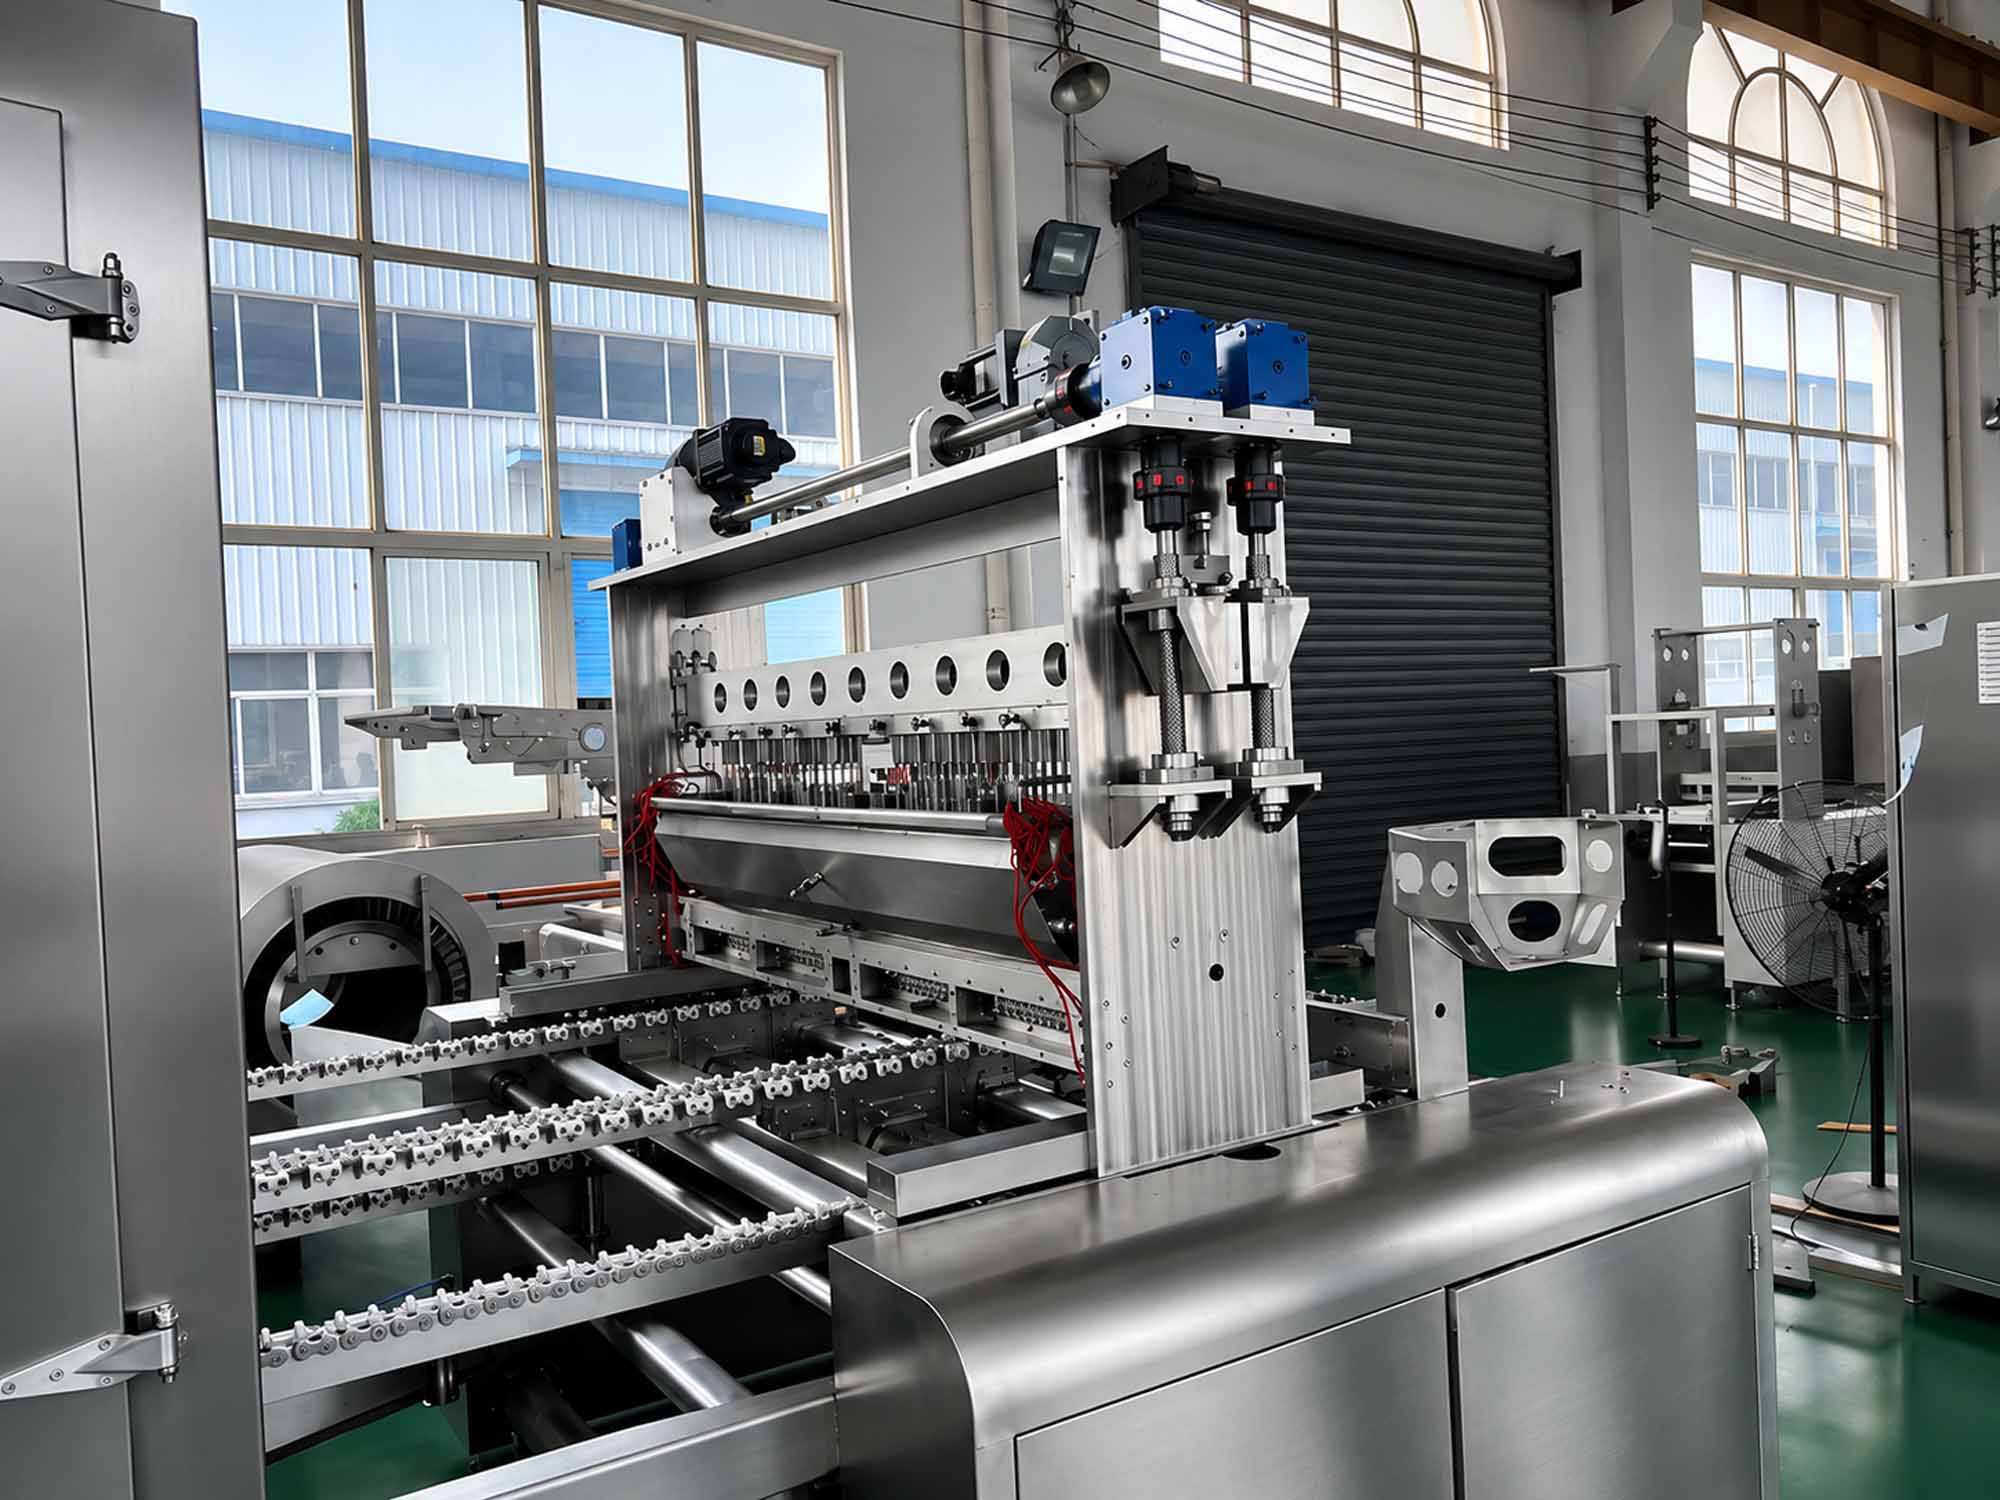
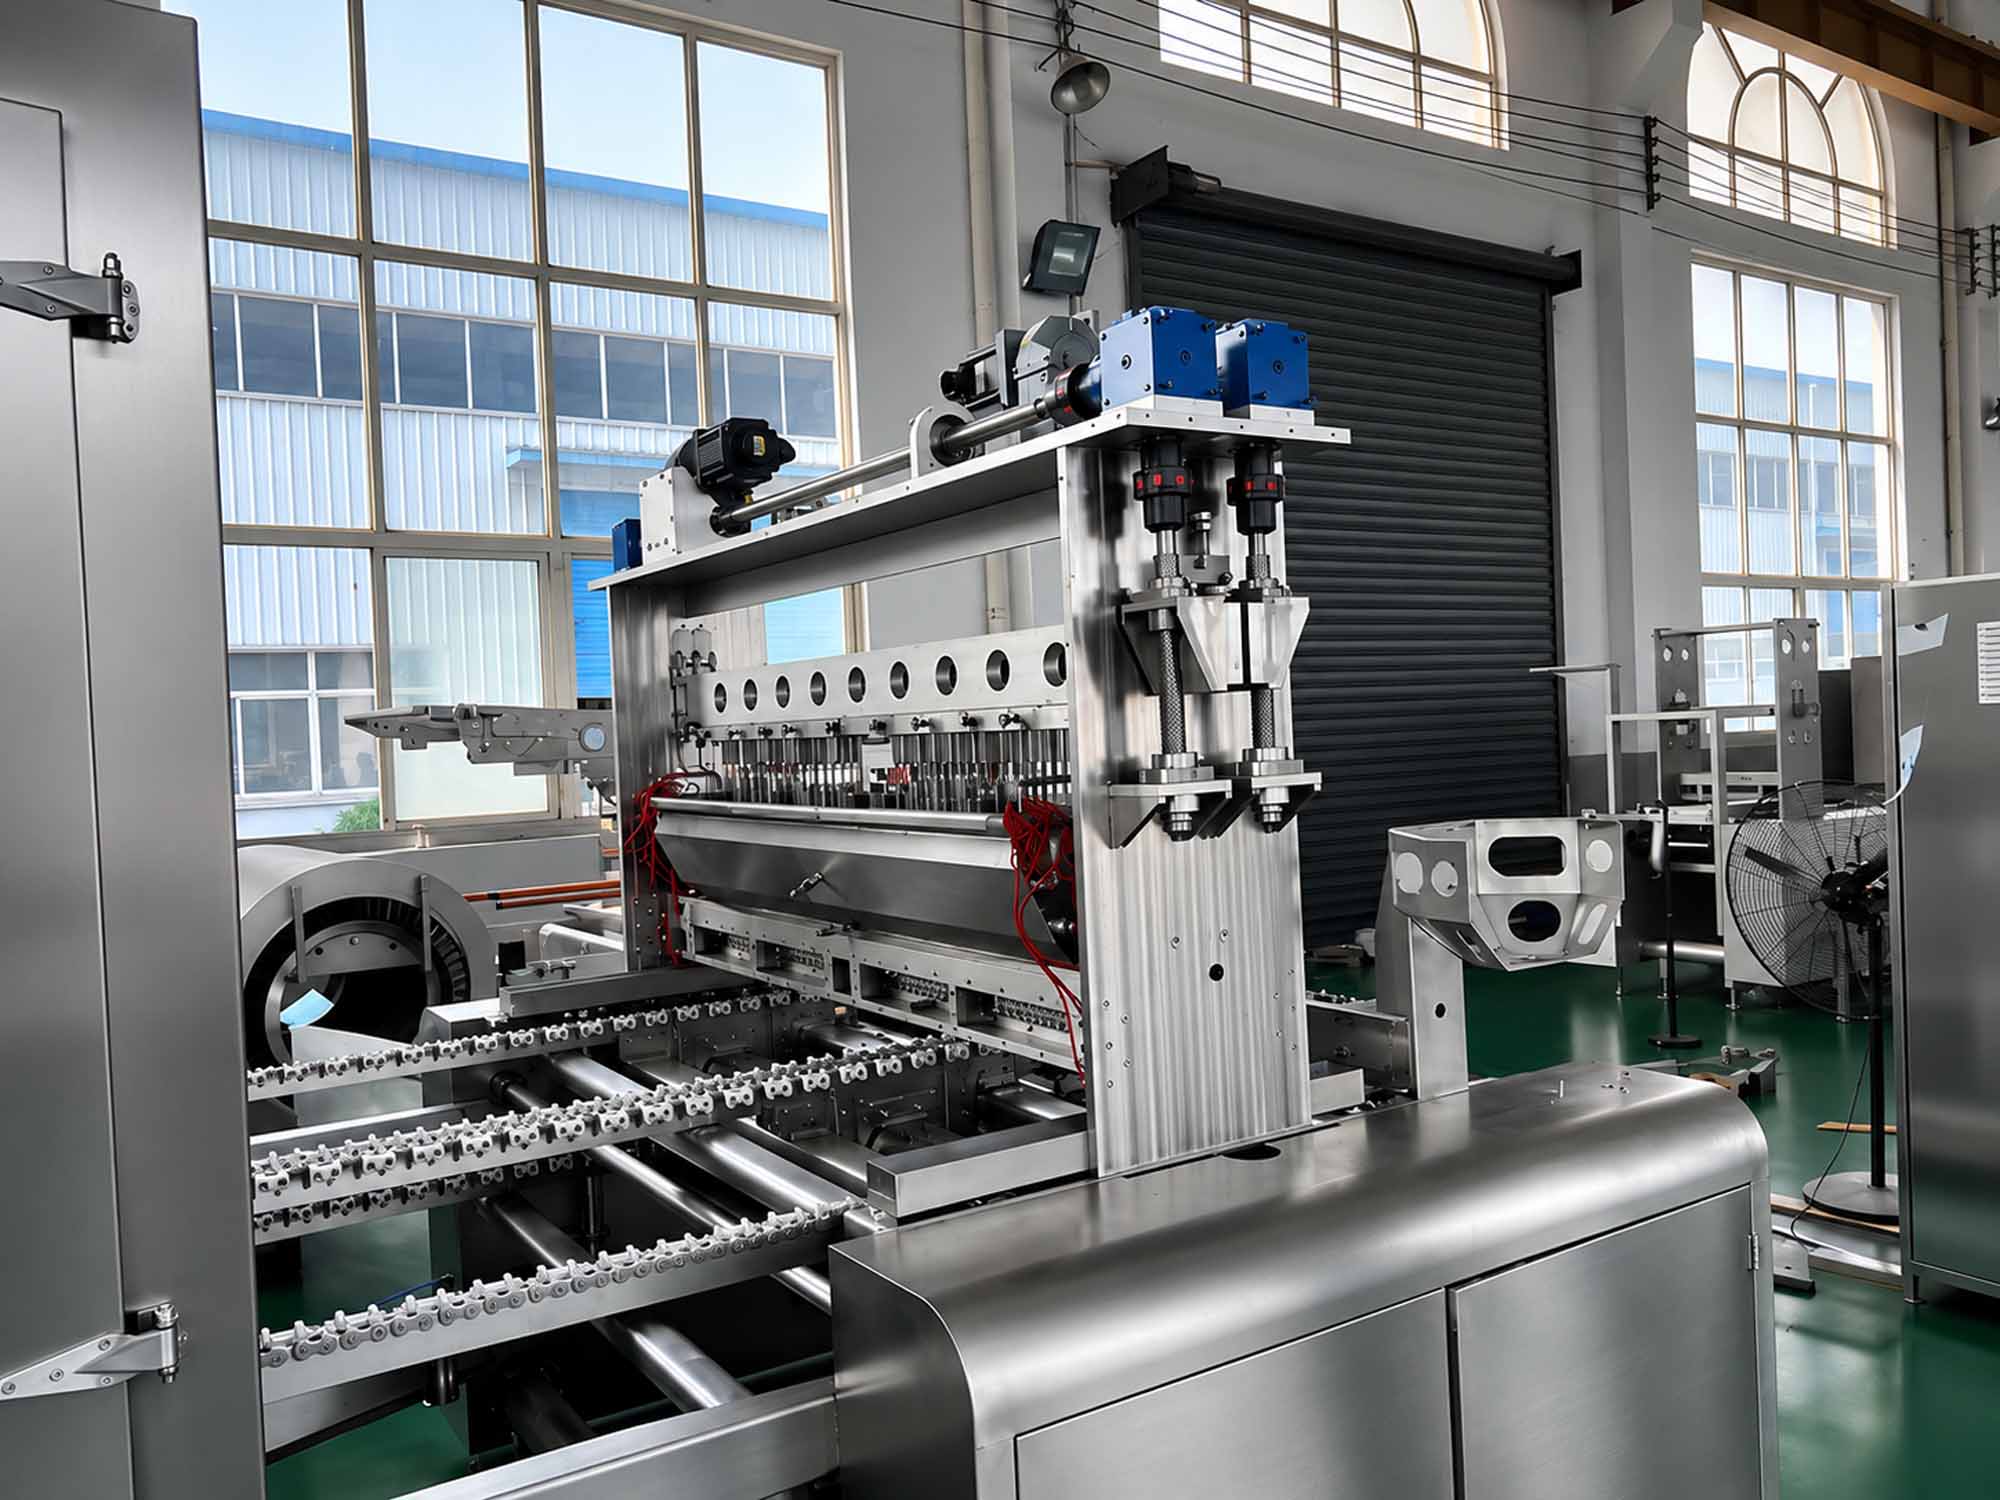
The depositing pistons run on servo motors with solid screw rods and linear guides. Chain-driven depositors are the common alternative — the chain stretches, and fill weight drifts after a few months. That’s a difference you see in your weight checks a year in, not on day one.
Full-Plate Demolding
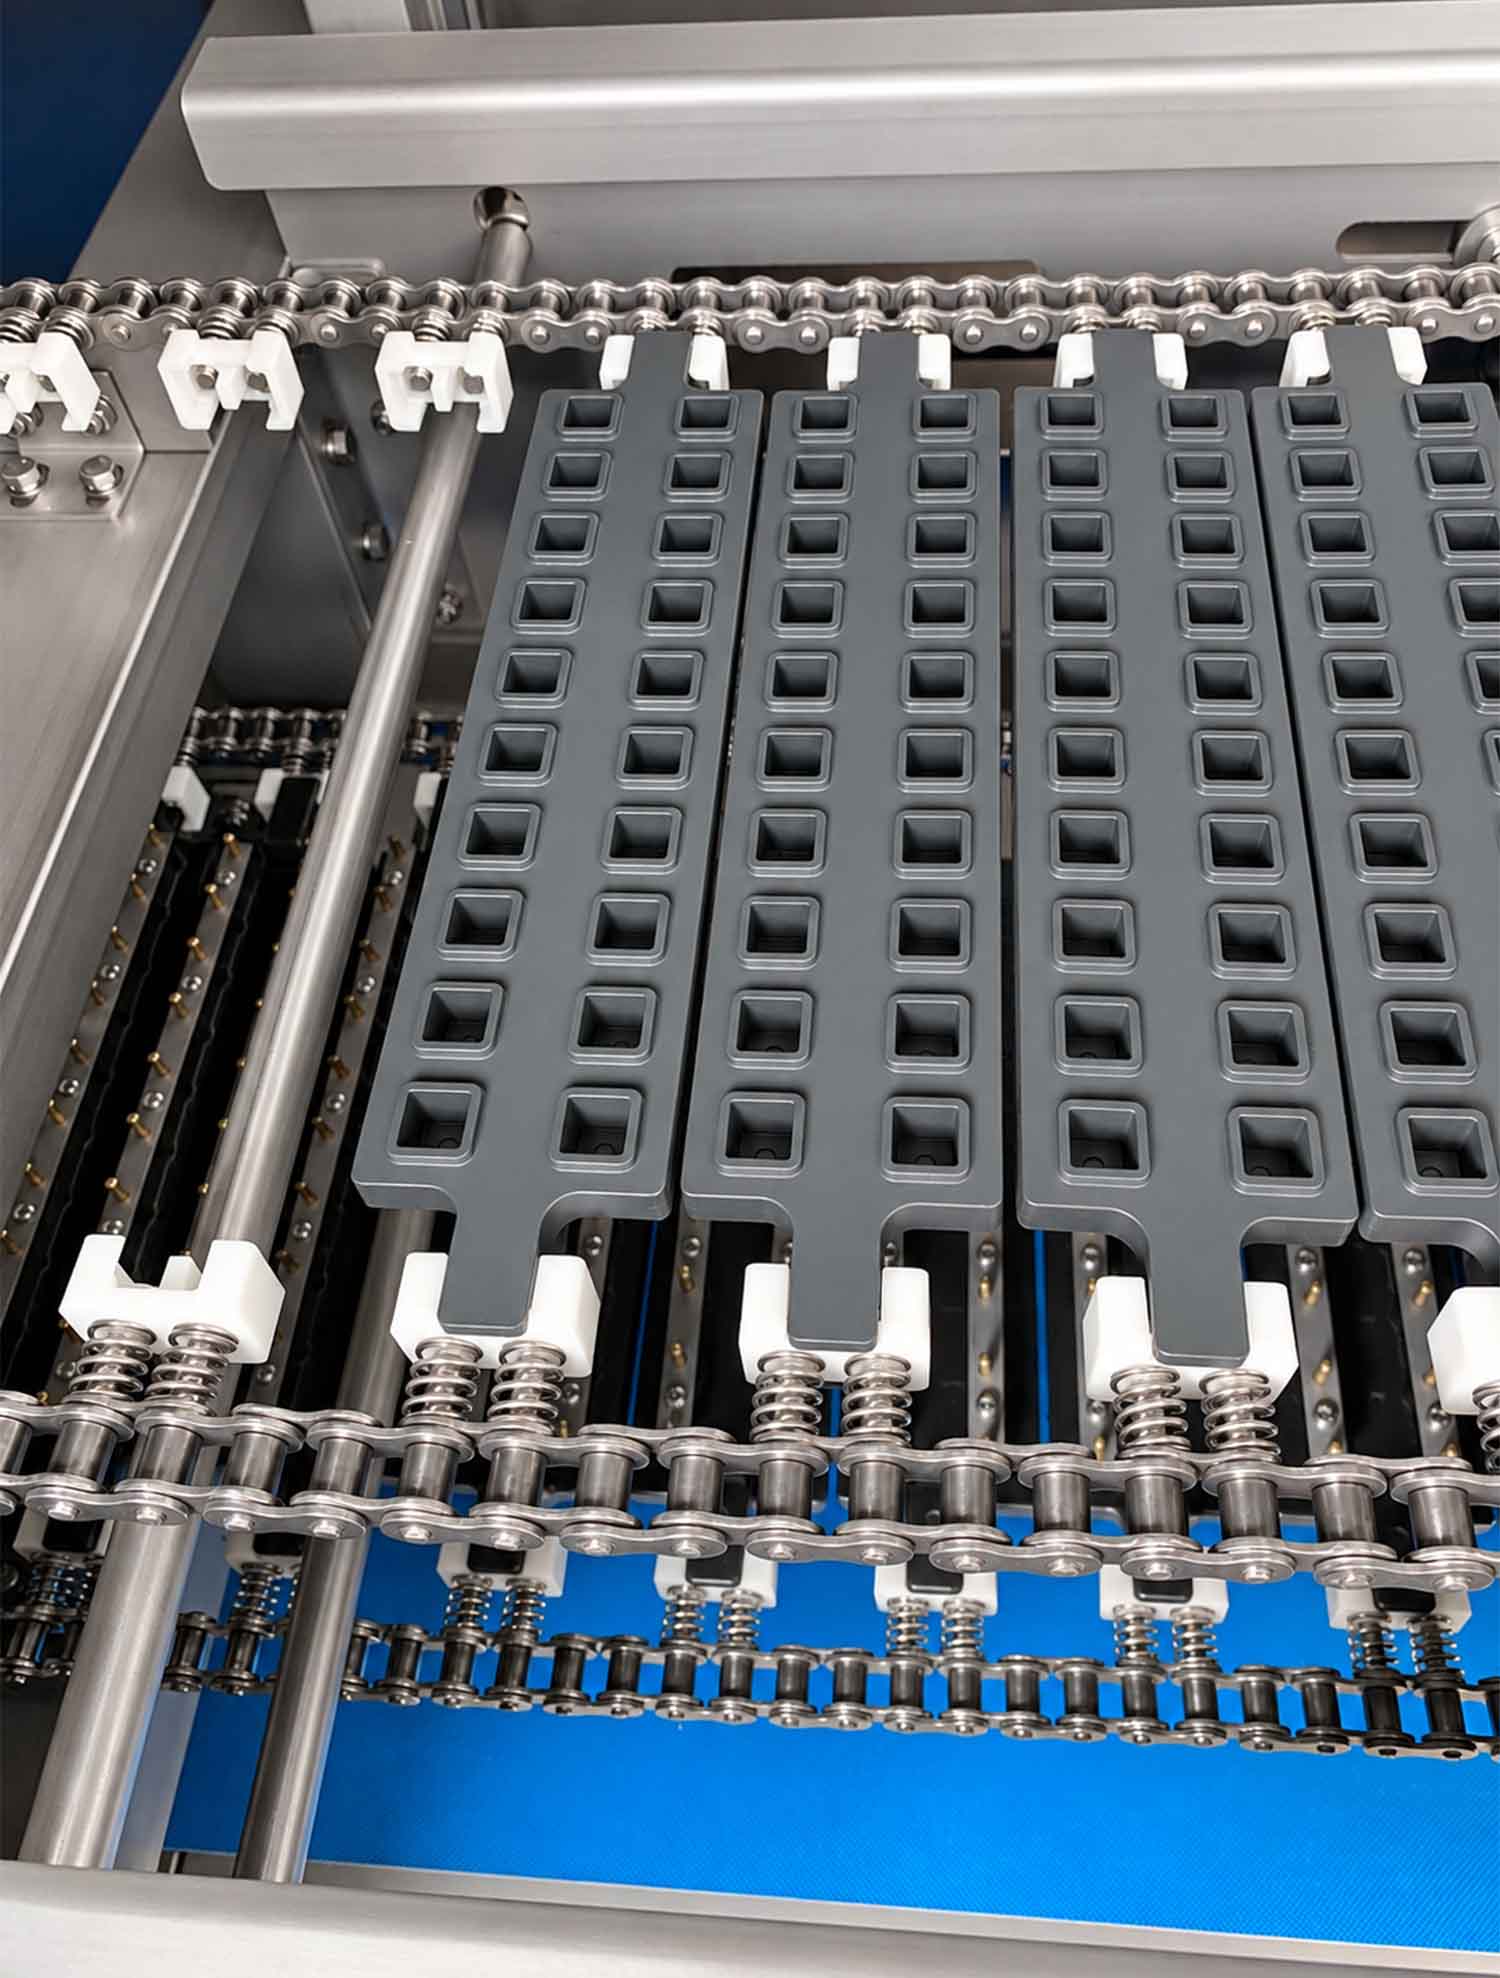
Dual pneumatic cylinders drop the whole tray face at once, evenly. The alternative is plate-chain demolding, which grips the frame edges and twists the tray over time — it chips the coating and eventually damages the mold. Two soft rotating brushes finish the release without touching the mold surface.
Quick-Release Molds on a Guide Rail
Molds are fully Teflon-coated and held by fast-release buckles on a guide rail. The alternative is screw-fixed molds with a half coating — an operator, a spanner, and an uncoated area where sticking starts.
Suspended Belt with Cylinder Tensioning
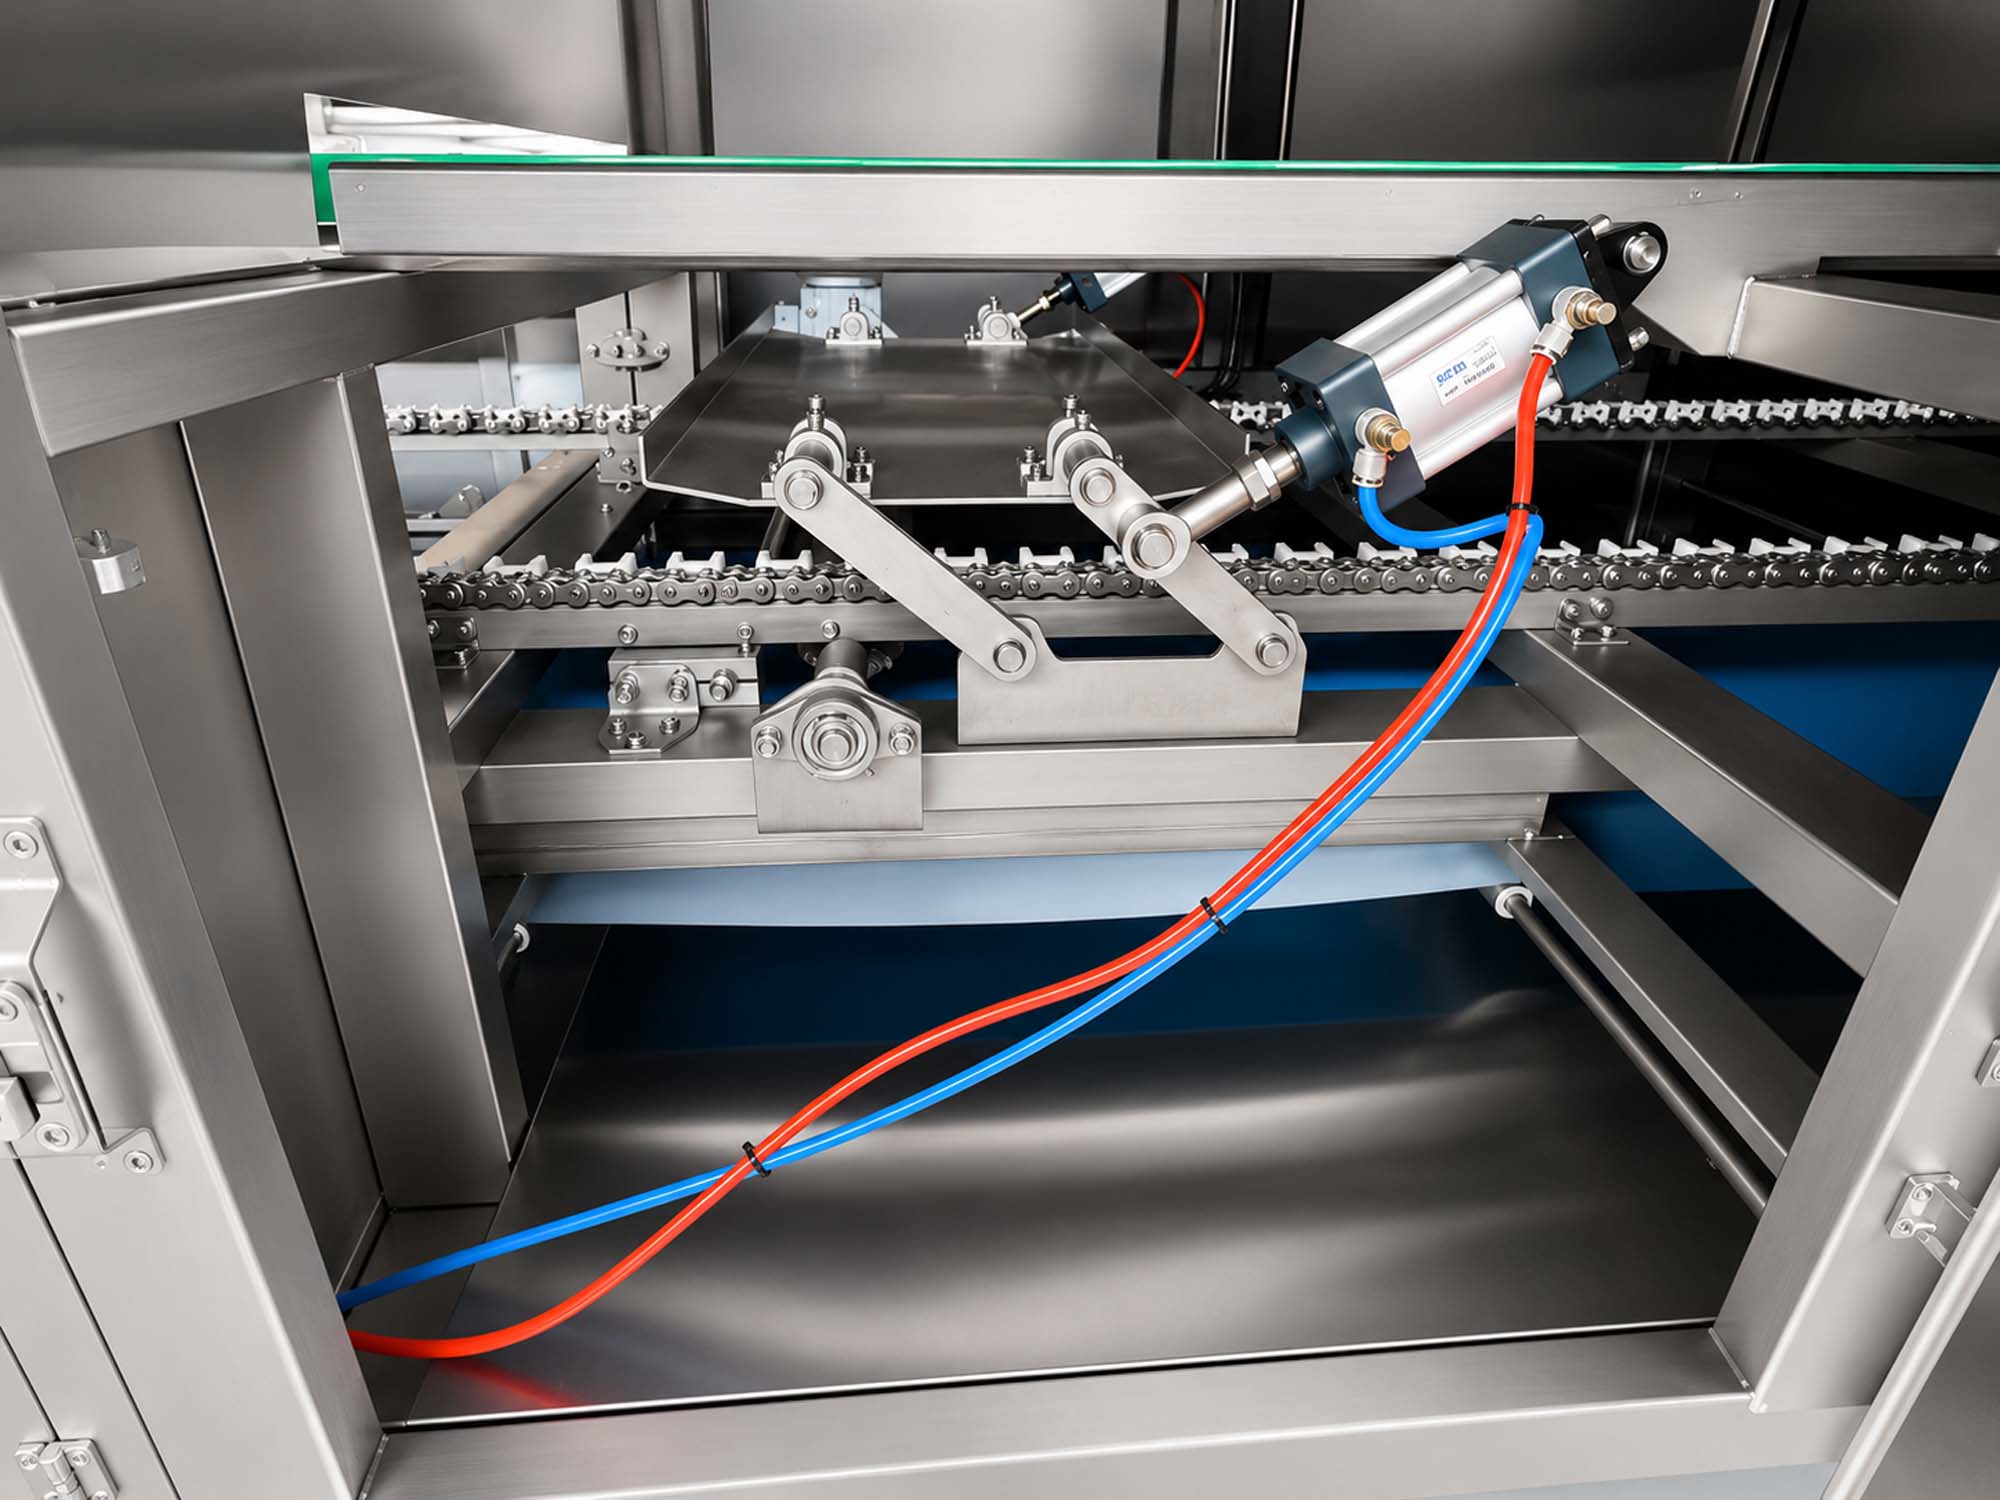
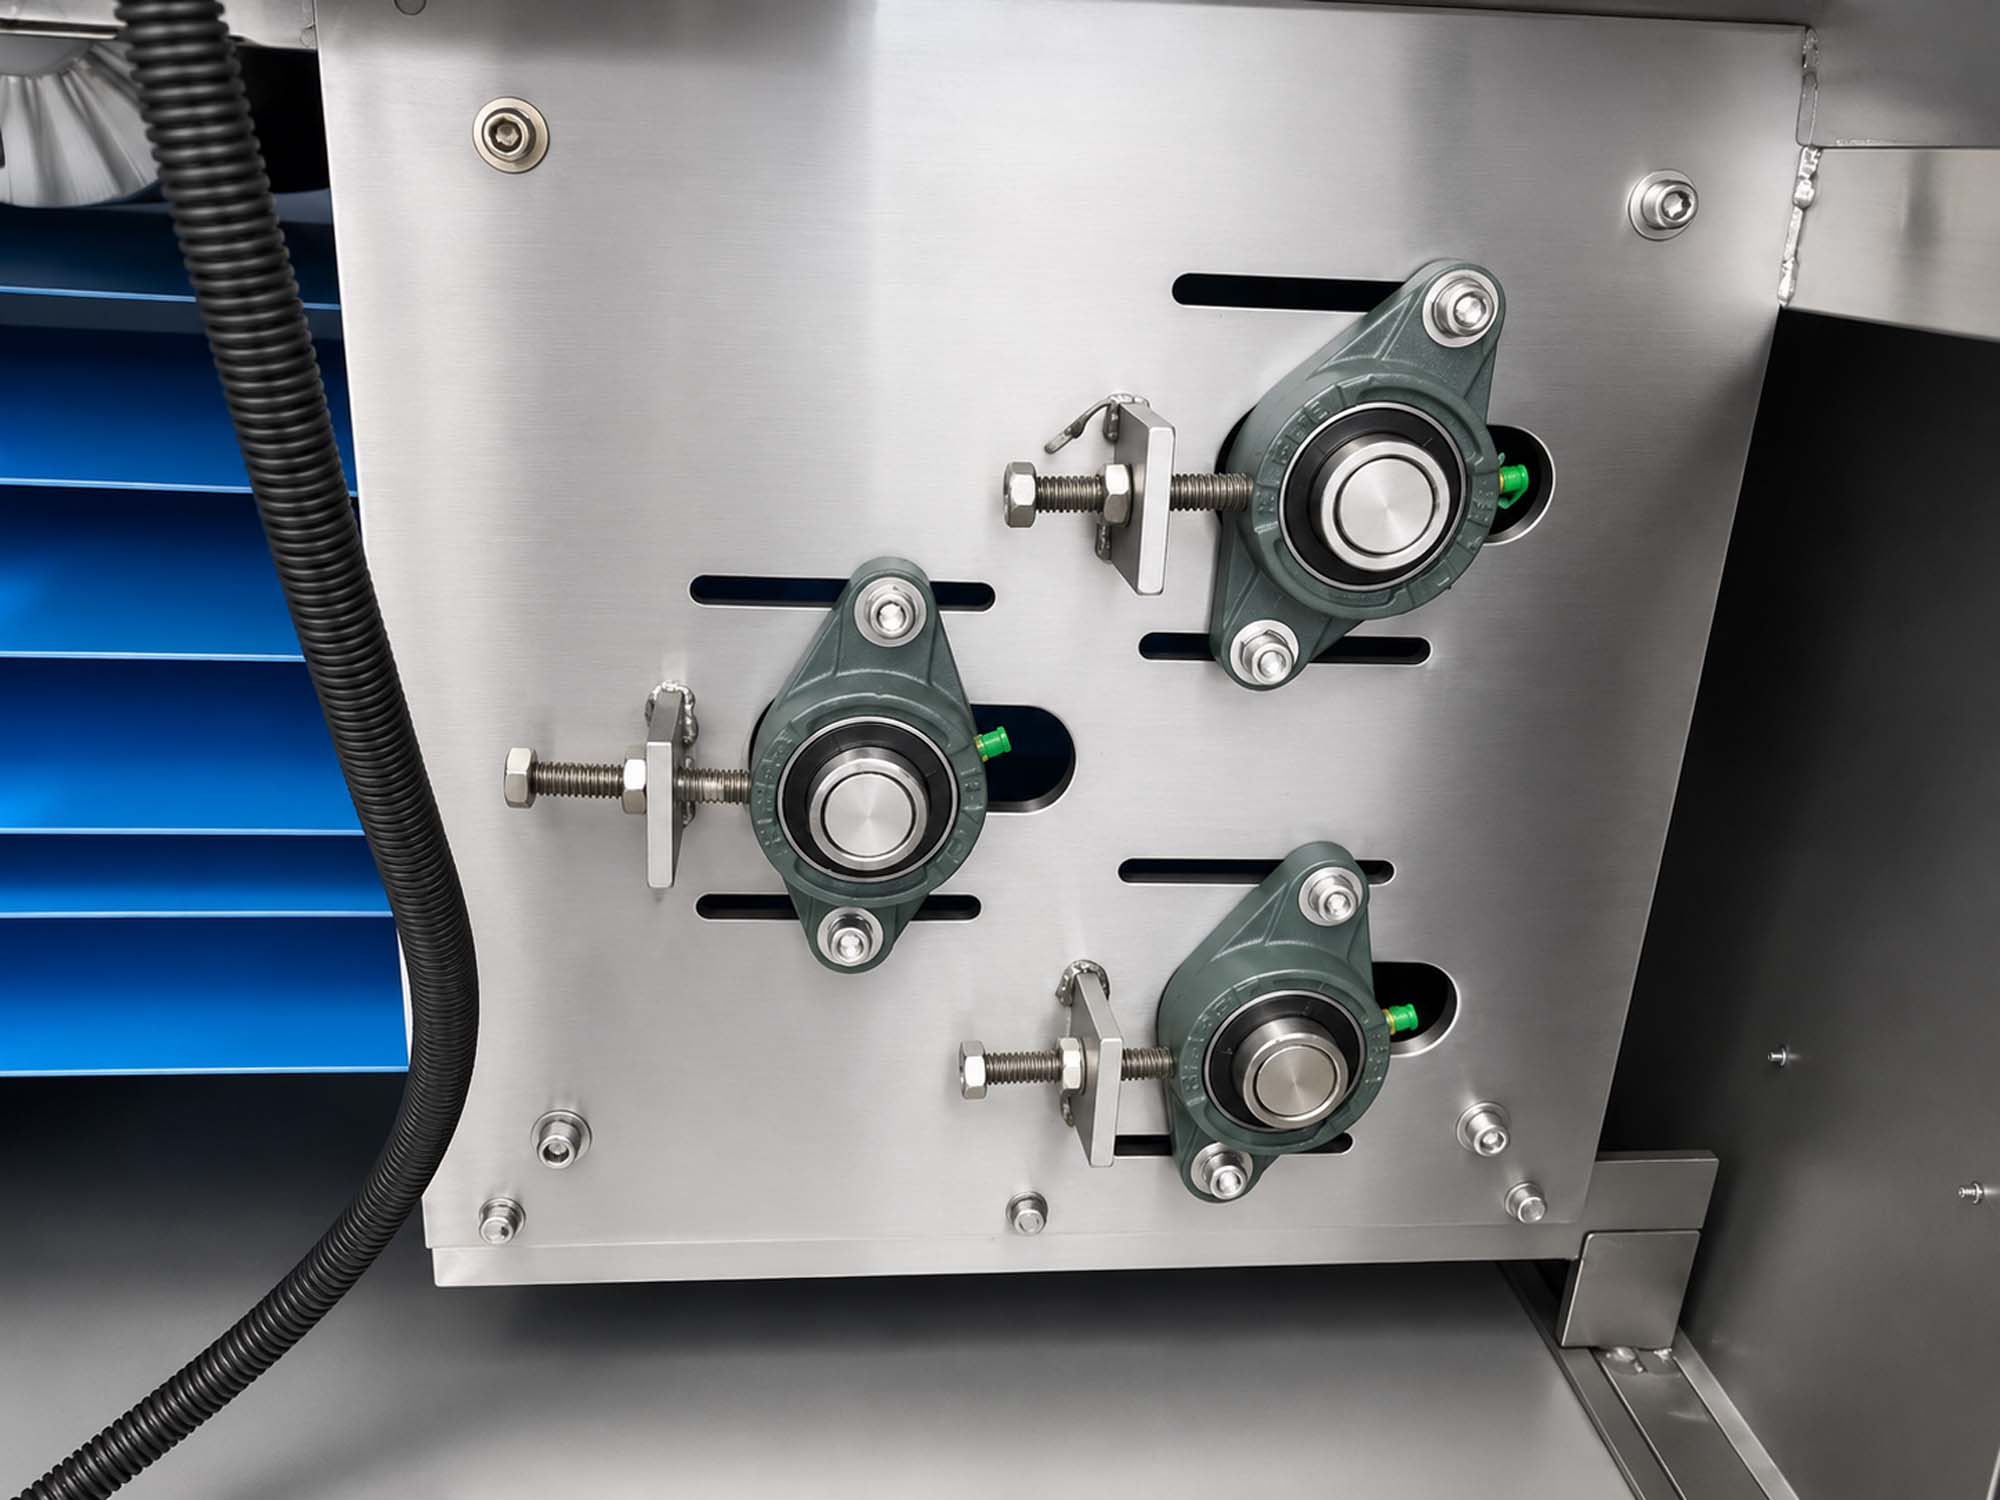
The blue PU belt runs suspended off the tunnel floor with a pneumatic cylinder holding tension automatically. Belts that sit flush against the tunnel trap spilled syrup underneath — they glue down and they’re hard to clean. Mechanical tensioners wear the belt out faster.
Motor at the Tunnel Exit, Not at the Depositor
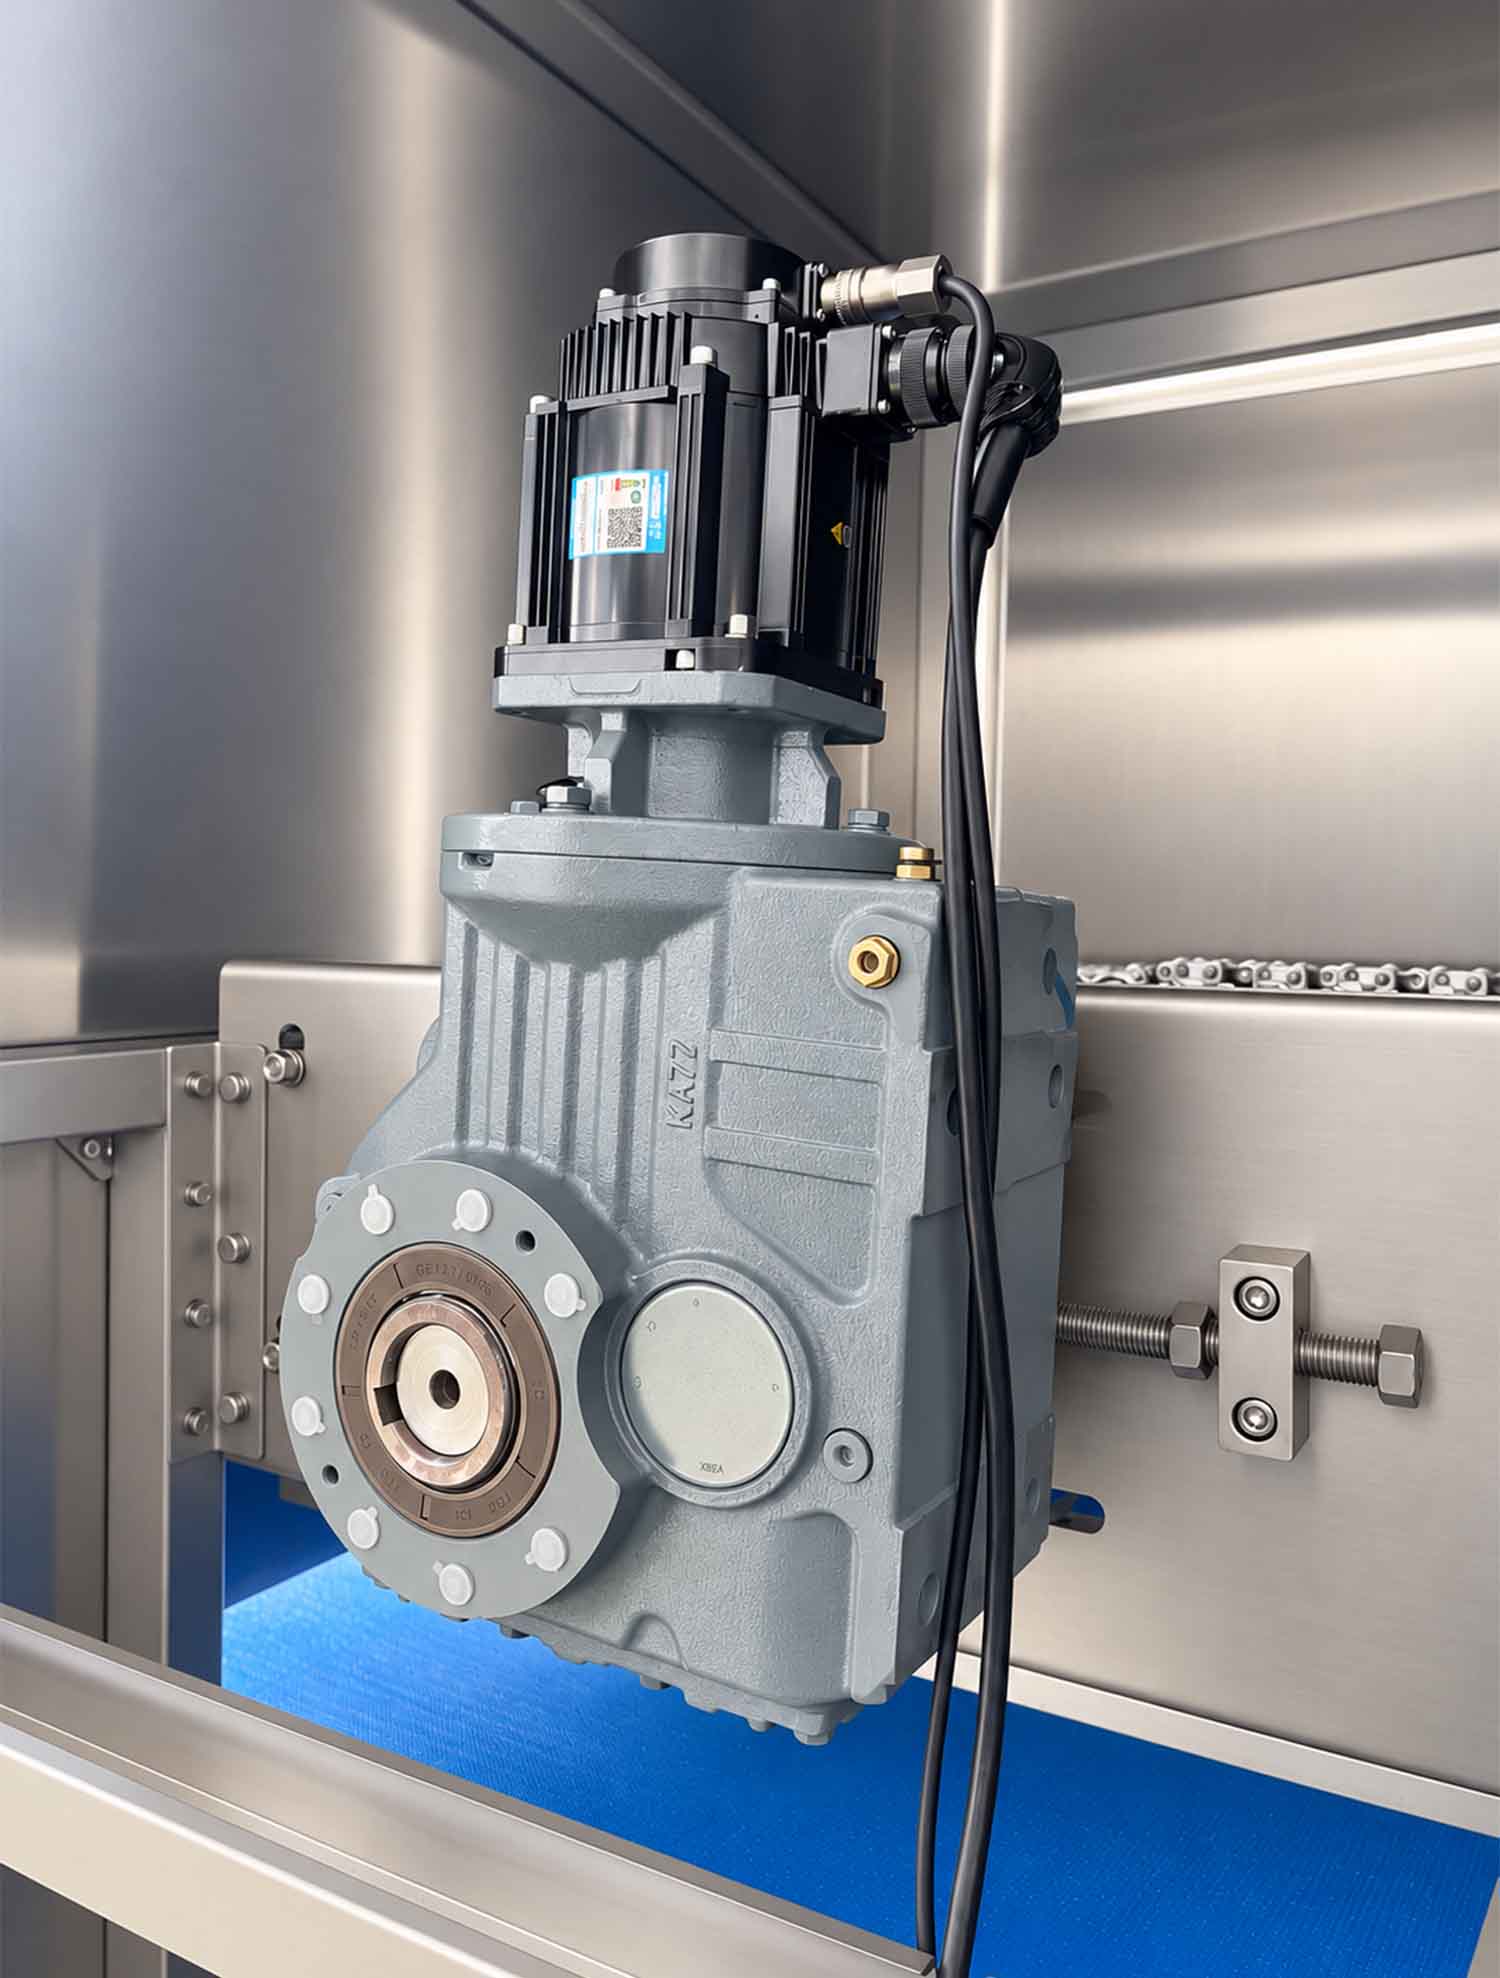
The drive motor sits at the cooling tunnel exit and pushes the mold chain rather than pulling it from the front. Front-mounted motors pull the chain unevenly, so over time the chain no longer runs level — and the depositing station loses accuracy because of it.
Vertical Dynamic Mixing
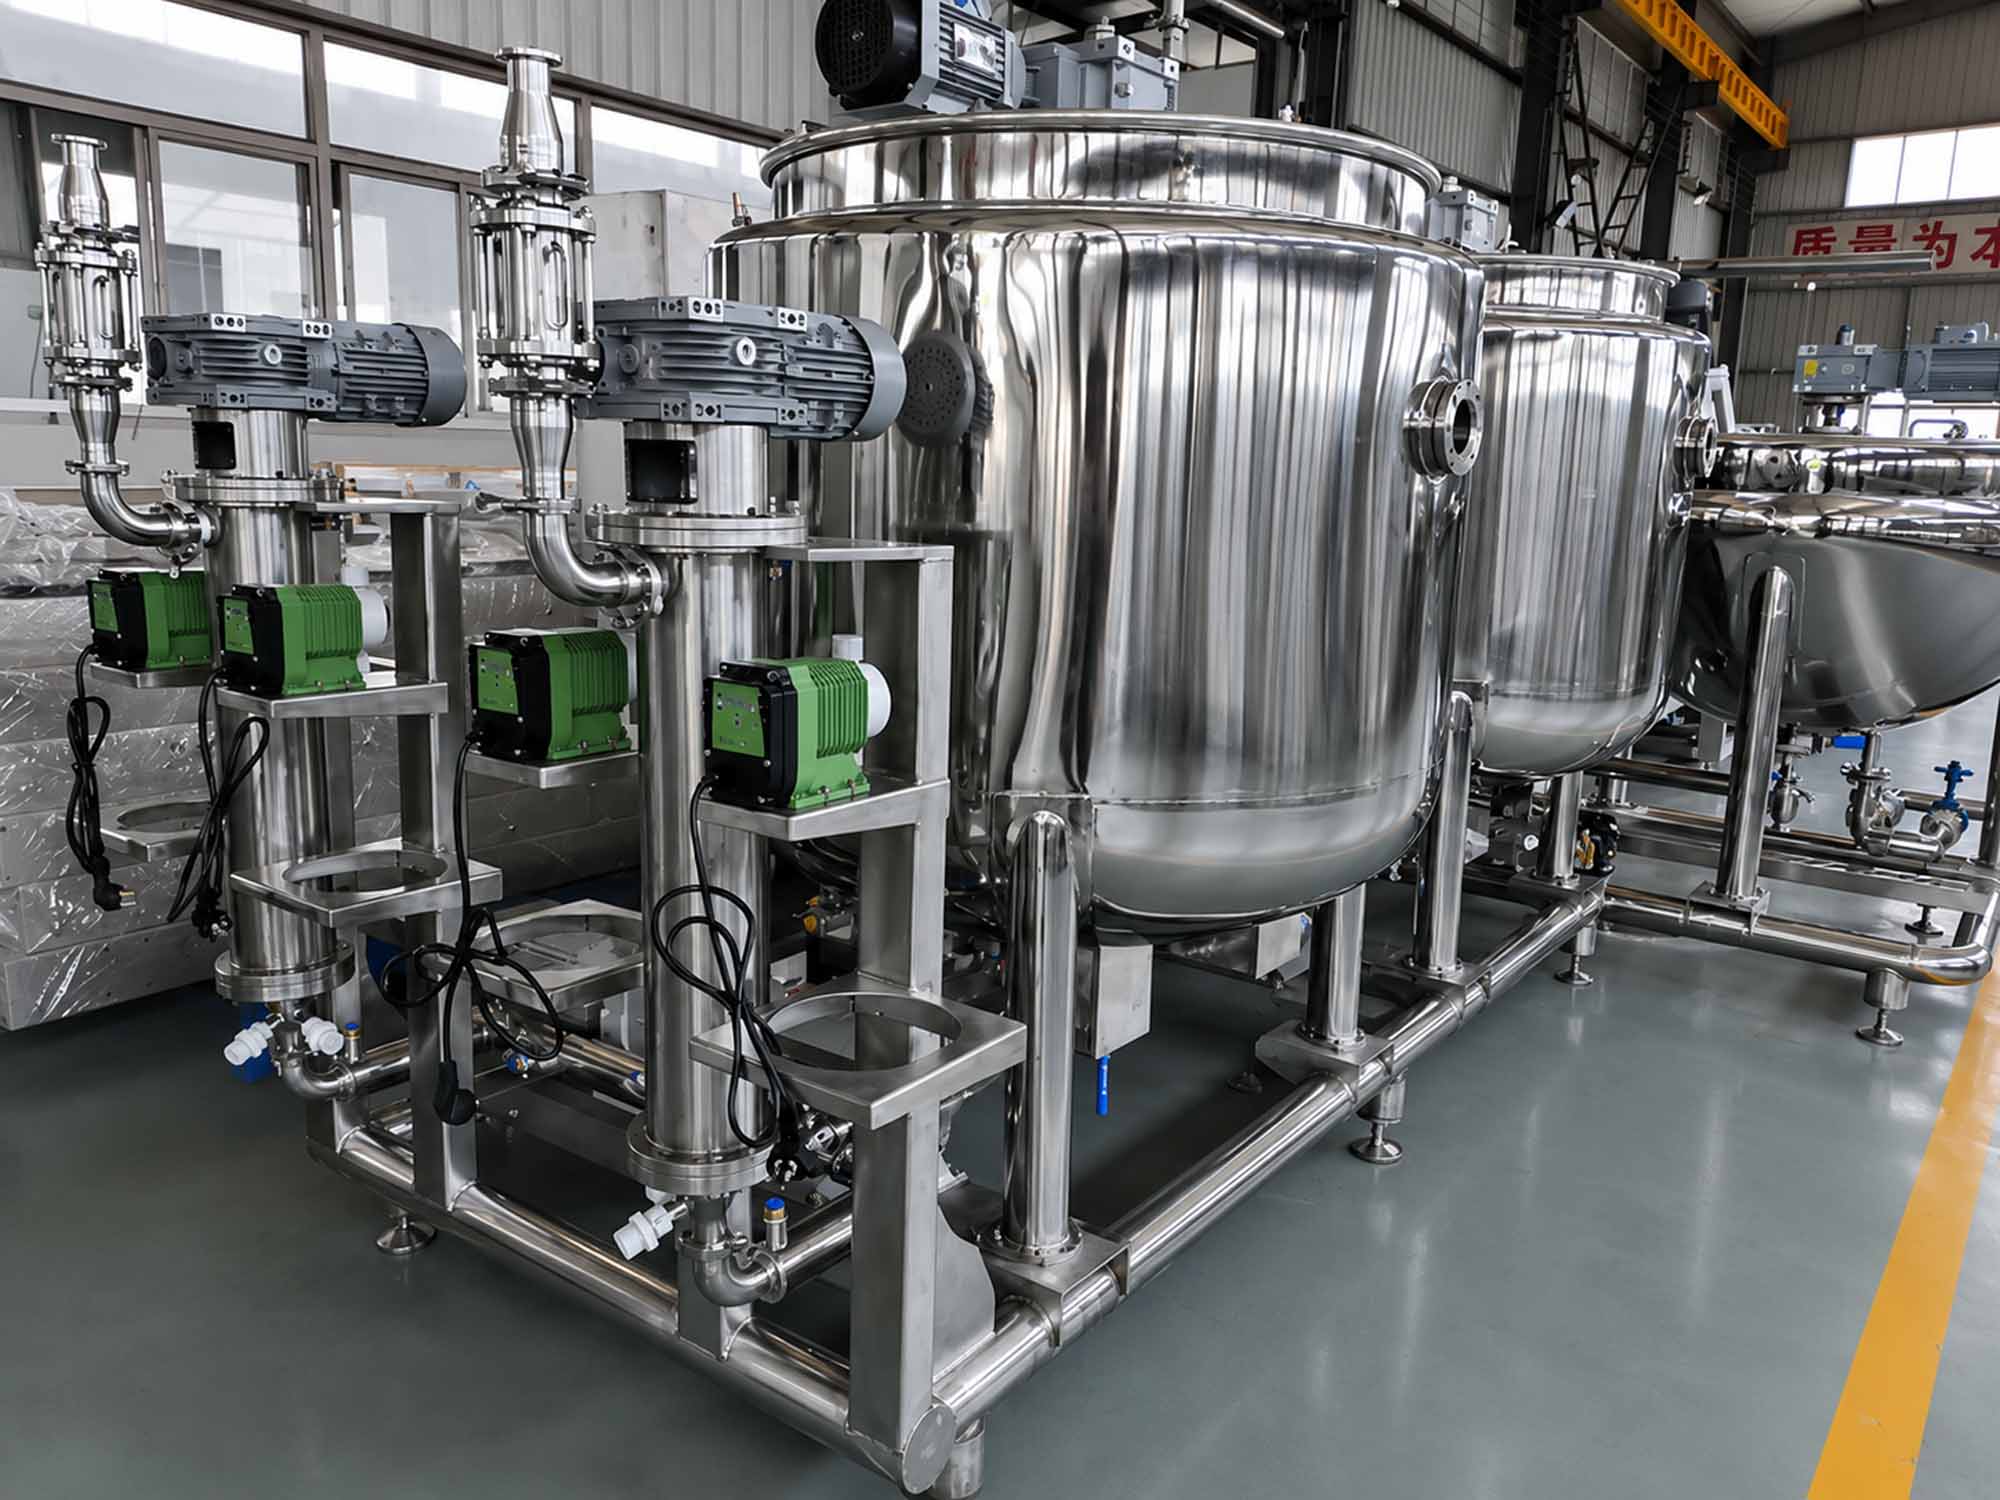
Flavor, color and actives are blended in a vertical mixer rather than a horizontal one. Horizontal mixing lets dense material — mineral powders, botanical extracts, organic acids — settle at the bottom of the pipeline. The vertical design forces the mass upward, and there’s a window so the operator can see it.
Technical specification
Specification | APK-GM600Q | What it means for you |
Output | 600 kg/h | — |
Depositing speed | 25–45 strokes/min | — |
Dosing accuracy | ≤ ±2% | Same servo depositing as every line we build |
Steam | 500 kg/h at 1.6–1.8 MPa | The highest steam pressure in our range. This is the constraint that stops most buyers, more often than floor space is. |
Compressed air | 0.3 m³/min | — |
Installed power | 85 kW, 60 Hz | The highest in the range. Built to your U.S. supply; we confirm the voltage with your quote |
Room conditions | 25–30 °C, humidity ≤45% | Same at every scale |
Line length | 20 m | Only 2 m more than the GM300Q, for twice the output |
Machine weight | 5,000 kg | Check your floor loading |
Operators | 2–3 | — |
Contact parts | SUS316L | Frame and pipework SUS304 |
Control system | Siemens PLC, UL or CE certified components | — |
Model comparison
Model | Output | Depositing speed | Steam | Power | Line length | Best for |
APC-GM80Q | 80 kg/h | 25–35/min | 80 kg/h, 0.4–0.6 MPa | 55 kW | 8 m | Bringing your first gummy in-house |
APC-GM150Q | 150 kg/h | 25–45/min | 250 kg/h, 0.5–0.8 MPa | 65 kW | 16 m | Growing brands scaling past a co-packer |
APC-GM300Q | 300 kg/h | 25–45/min | 300 kg/h, 0.8–1.2 MPa | 75 kW | 18 m | Multi-shift plants and contract manufacturers |
APC-GM600Q | 600 kg/h | 25–45/min | 500 kg/h, 1.6–1.8 MPa | 85 kW | 20 m | Mass-market confectionery volumes |
Output is in kilograms per hour, not pieces — piece count depends on your gummy weight. Tell us both and we’ll work it back for you.
All four run the same servo depositing, the same full-plate demolding and the same mold system. What changes is throughput, and what that costs you in steam, power and floor.
Industry Applications
Vitamin and mineral gummies
Pectin and vegan formulations
Functional and botanical gummies
Ashwagandha, elderberry, apple cider vinegar. Dense botanical extracts settle in horizontal mixing lines — that’s what the vertical mixer exists for.
What changing over involves
Changing shape is a mold swap. Changing base is a different conversation.
What changed | What you adjust | Roughly |
Same shape, new flavor or color | Recipe on the screen, flush the mixer | 30–60 minutes |
Different gummy shape | Swap the mold trays — quick-release buckles on a guide rail, no screws | 30–60 minutes |
Gelatin → pectin | Cooling tunnel settings and your drying room. Pectin cures 20–24 hours against 8–12 for gelatin | Not a changeover — a process change |
Different piece weight | Depositing stroke on the servo, and possibly the manifold | 30–60 minutes |
Molds are fully Teflon-coated and held on a guide rail with fast-release buckles. The common alternative is screw-fixed molds with a half coating — those take an operator and a spanner, and the uncoated area is where sticking starts.
What your plant needs to supply
Utilities
Steam — the volume and pressure depend on the line size, listed in the specification table on each model page. Compressed air. Electricity, water inlet and drainage.
Air handling
Two dehumidifiers — one for the cooling area, one for the packing room. Two air conditioners, same two rooms.
Room conditions
Forming area: 25–30 °C, humidity 45% or below. Cooling tunnel: 5–10 °C. Drying room for pectin: 25–30 °C, humidity 25–45%.
What we supply
The line, the layout drawing, installation, operator training — and the formula if you don't have one.
Two things worth raising early. Steam is the one most buyers overlook — if you don’t have a boiler, tell us and we’ll quote the electric heating option instead. And no machine fixes a room that swings: if you can’t hold the forming conditions yet, say so before you order, not at commissioning.
What to check before you buy
Weight consistency, checked over time
A servo depositor and a chain-driven one both hit spec on day one. Ask any supplier what their fill weight looks like after six months of running, and how they verify it at the factory acceptance test. That's the number that decides your giveaway.
The manual
A clear English manual gets your operator running in a week instead of a month. Ask to see a sample page before you order.
Installation and training
Installed, commissioned, and your people taught to run the line. Ask what's included and what costs extra — the answer varies more between suppliers than the machine price does.
Why Choose AIPAK?
One Point of Contact
One project engineer handles your line from layout drawing to commissioning, so you’re not chasing five suppliers for one answer.
Free Formulas, Whether You Buy or Not
Gelatin and pectin production formulas, with ingredient ratios and process steps. Yours whether you buy from us or not.
A U.S. Number, Answered by Us
+1 (213) 526-8644, answered by our engineers 9 AM–7 PM China time, Monday to Friday. That’s evening and overnight in the U.S., so leave a message or send a WhatsApp anytime and we’ll pick it up first thing.
Spare Parts and Lead Time, in Writing
A kit of wear parts ships with your line. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.
Questions About the APK-GM600Q
Horizontal mixing lets dense material — mineral powders, botanical extracts, organic acids — settle at the bottom of the pipeline, so the first and last gummies in a run don’t get the same dose. The vertical mixer forces the mass upward and keeps dense actives in suspension through the run. There’s a window so the operator can see it.
Flexible tubes kink, blister and crack with repeated heating and washdowns. The circulation loop is rigid stainless steel pipe, so it doesn’t degrade and doesn’t leak at the joints when the line is washed down.
Plate-chain demolding grips the edges of the mold tray, which twists it over time and chips the non-stick coating. Full-plate demolding uses two pneumatic cylinders to press the whole tray face evenly, and two soft rotating brushes finish the release without touching the mold surface.
Yes. The electrics are rated IP65, and every sensor and heater connects through a water-resistant aviation plug. Your crew can wash down the frame, the inside of the cooling tunnel and the hopper without covering the electrics first.
An open valve drifts as the pressure changes, so someone has to keep adjusting it, and it keeps dripping if it’s left on after the shift. The sprayer on this line is solenoid-controlled: once the volume is set, it stays the same through the run, and it stops when the line stops.
Yes, free. We’ll send you production formulas for both gelatin and pectin, with ingredient ratios and the process steps. You don’t have to buy from us to have them.
Forming at 25–30 °C with humidity 45% or below. Cooling tunnel at 5–10 °C. For pectin, a drying room at 25–30 °C and 25–45% humidity for 20 to 24 hours. Gelatin cures faster, 8 to 12 hours. If you can’t hold these yet, tell us early — it changes what we’d recommend.
The cooker can be built with electric heating instead. Tell us at enquiry rather than after the quote — it changes the build and the price, and it’s much easier to specify than to retrofit.
The numbers are the same — 25–30 °C forming, 45% humidity or below, 5–10 °C tunnel. What changes is how hard they are to hold across a larger area. Send us your room dimensions and your current HVAC and we’ll tell you honestly whether it’s enough.
Higher output means more syrup to bring up to temperature in the same time. If your boiler tops out below 1.6 MPa, tell us — it’s the one requirement on this line that can’t be worked around at the machine.
Yes. We build to your U.S. supply at 60 Hz and confirm the voltage with your quote.
A kit of wear parts ships with your line. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.
Customers Also Interested In...
Machines that usually sit next to this one:
Not sure which line size?
Tell us your target output in kg per hour and your piece weight. We'll tell you which one, and why.
Send us your formula — or ask us for one
If you have a formula we'll tell you what the line needs to run it. If you don't, we'll send you ours. Free, either way.
Send your floor dimensions
Length, width, height, and where the doors and columns are. We'll draw your line against your actual room.
Reply within one business day. Formulas sent free, whether you buy or not.