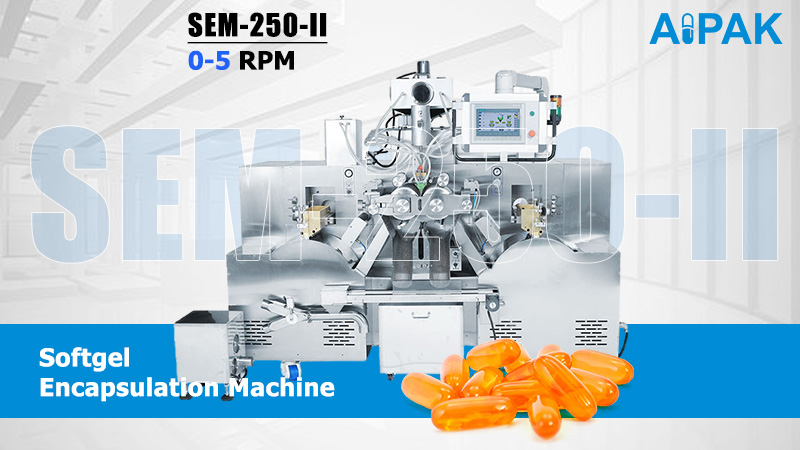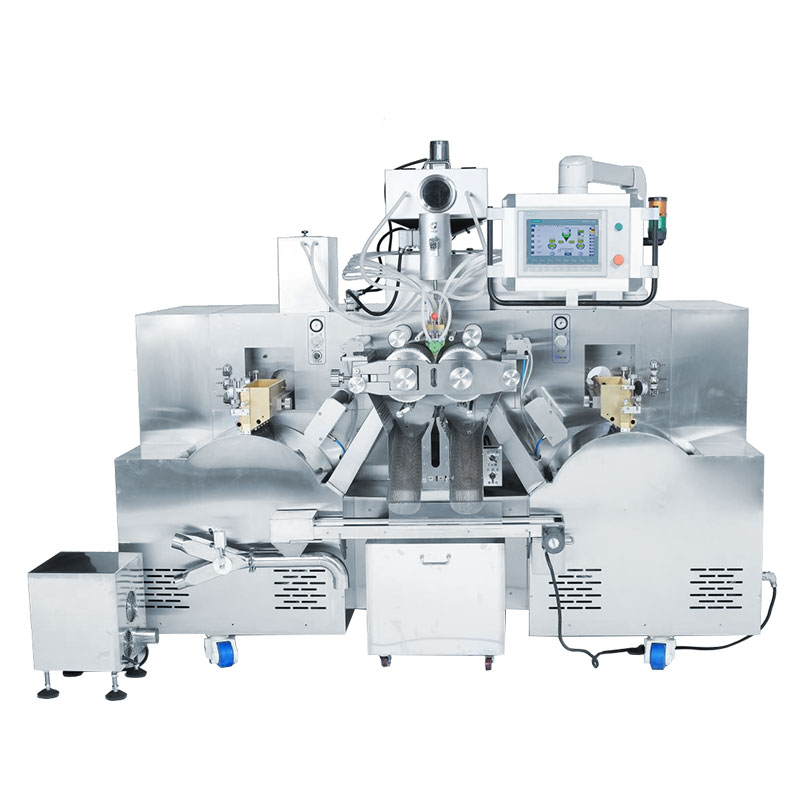
SEM-250-II Softgel Encapsulation Machine
Twenty plungers, Φ150 × 250 die roll, 5 RPM — up to 172,800 capsules an hour
Same 20 plungers, same Φ150 × 250 die roll and the same filling accuracy as our servo flagship. What you give up is die roll speed — 5 RPM against 7 — and automatic die alignment. If you run one or two shapes and your volume sits under 170,000 an hour, this is the machine most of our customers buy.
1. Output: up to 172,800 capsules an hour at 3# oval
2. Filling accuracy: ±0.5% on oils, ±1.5% on suspensions
3. Same die roll as our servo flagship: Φ150 × 250 mm, 20 plungers, at 5 RPM instead of 7
4. Power:12 kW, three-phase, 60 Hz, built to your U.S. supply
Is this the right machine for you?
✓ Yes, if…
- You need up to 172,800 capsules an hour
- You run one or two shapes and rarely change
- You want the 250 die roll and 20 plungers without paying for servo
- You already have drying capacity for this output, or you're buying it with the machine
✕ Buy something else if…
- You change shapes weekly → the 250-IIIA stores digital profiles; here you re-time mechanically
- You need more than 172,000 an hour → the 250-IIIA runs 7 RPM against 5
- You haven't sized your drying → this machine produces more than most plants can dry
Technical specification
| Feature | SEM-250-II Specifications |
| Die Roll Size | Φ150 × 250 mm |
| Die Roll Speed | 0 – 5 RPM (Infinitely Variable) |
| Number of Plungers | 20 Plungers |
| Filling Accuracy | ±0.5% (oil) / ±1.5% (suspension) |
| Total Power | 12 kW |
| Dimensions | 2,100 × 1,000 × 1,900 mm (L×W×H) |
| Machine Weight | 1,500 kg |
| Power Supply | Three-phase, 60 Hz |
Model comparison
Capsule size | SEM-100II | SEM-120-III | SEM-250-II | SEM-250-IIIA |
3# oval | 30,240 | 115,200 | 172,800 | 259,200 |
6# oval | 24,000 | 68,400 | 127,680 | 191,520 |
8# oval | 22,800 | 63,000 | 120,960 | 181,400 |
10# oval | 17,280 | 51,000 | 106,080 | 159,120 |
14# oval | 15,360 | 48,000 | 92,160 | 138,240 |
20# oval | 10,800 | 34,800 | 69,600 | 104,400 |
8# oblong | 18,240 | 49,200 | 109,200 | 163,800 |
10# oblong | 15,120 | 45,600 | 82,080 | 123,120 |
16# oblong | 13,680 | 32,400 | 69,120 | 103,680 |
20# oblong | 8,160 | 30,600 | 57,120 | 85,680 |
5# round | 24,480 | 79,200 | 158,400 | 237,600 |
10# round | 20,160 | 63,000 | 122,400 | 183,600 |
40# round | 5,760 | 27,600 | 66,240 | 99,360 |
Output depends on capsule size more than on anything else. A 3# oval and a 40# round come off the same machine at roughly a four-to-one ratio. Tell us your size and shape and we’ll give you the number for your product, not the headline one.
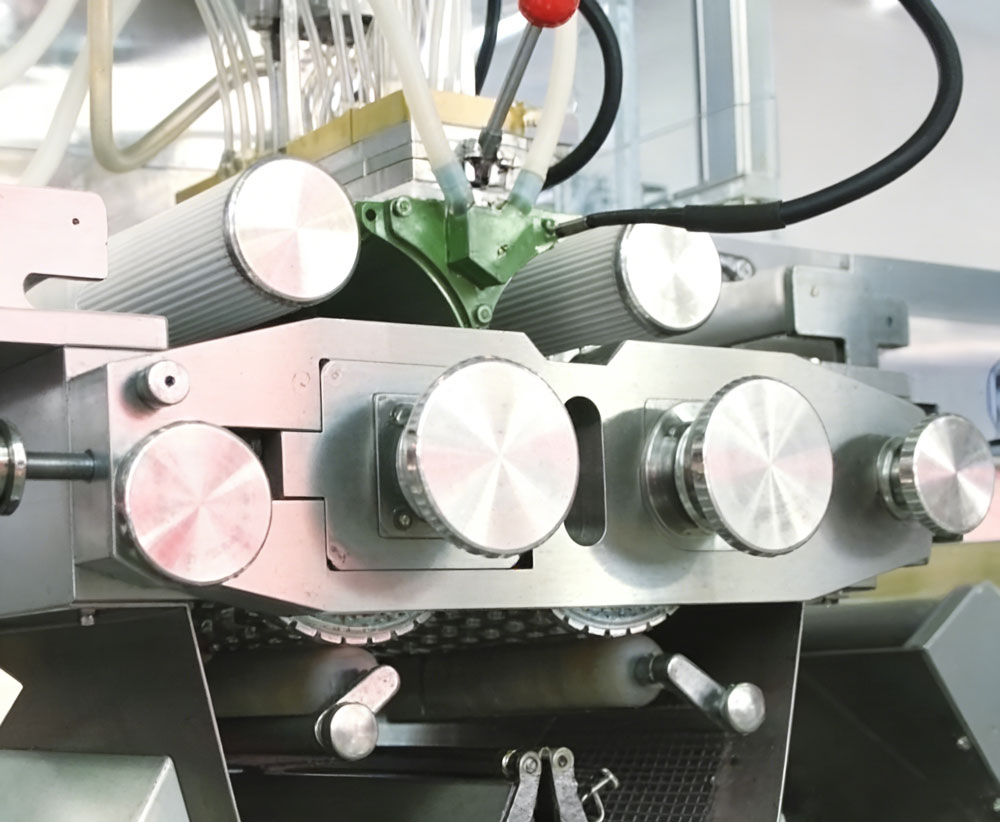
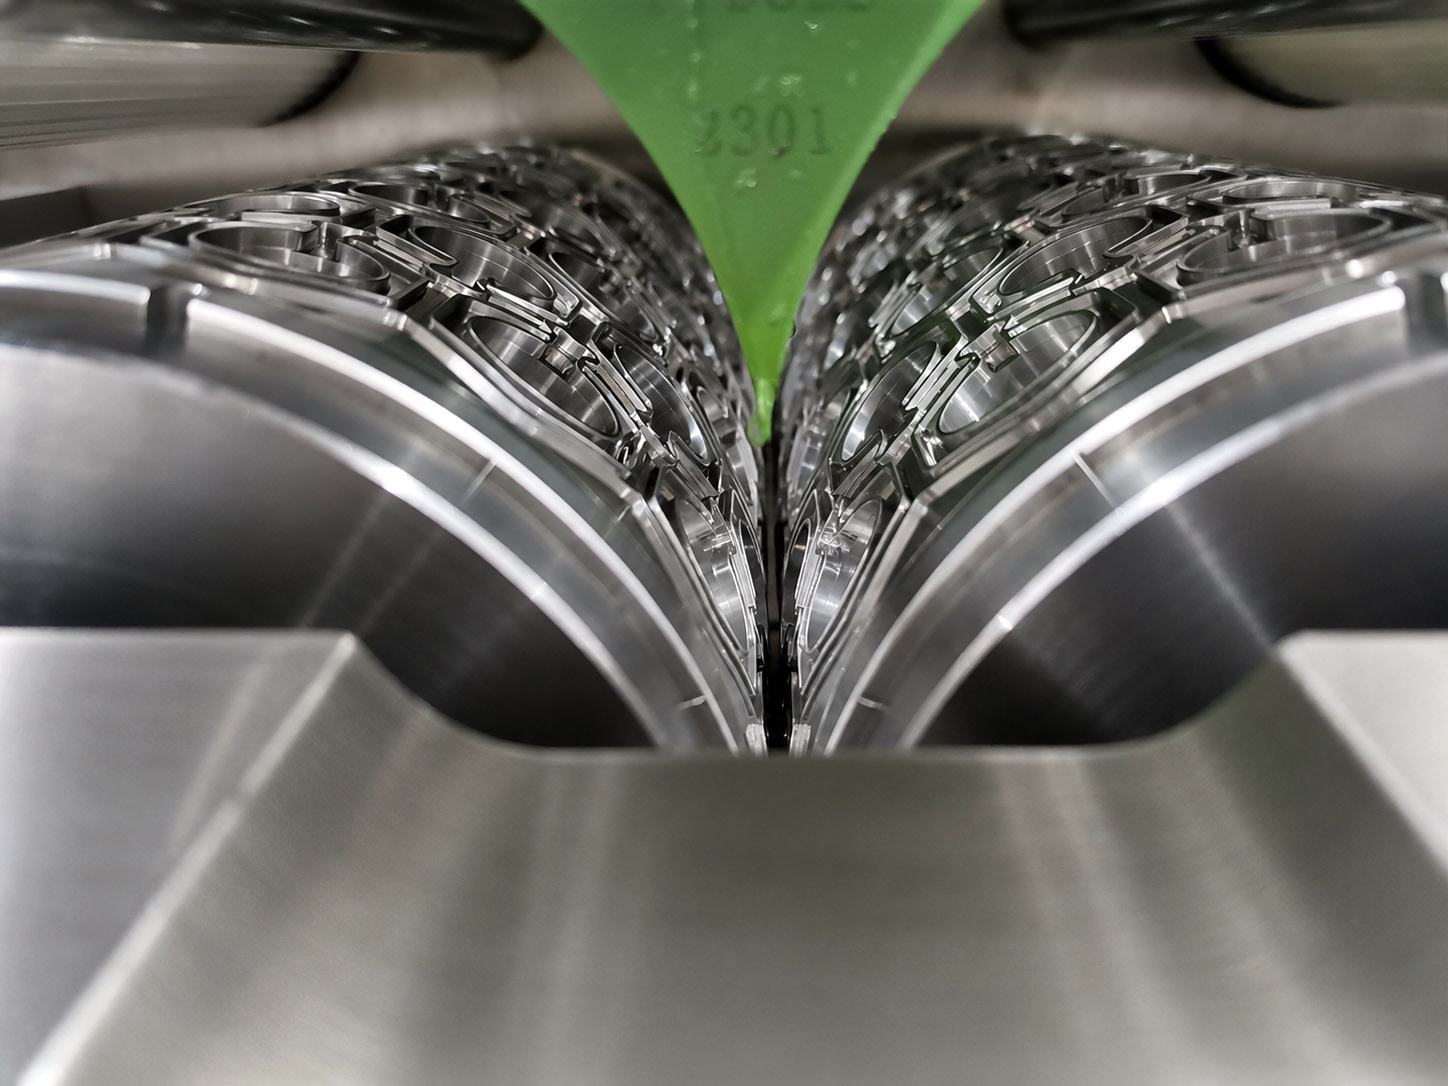
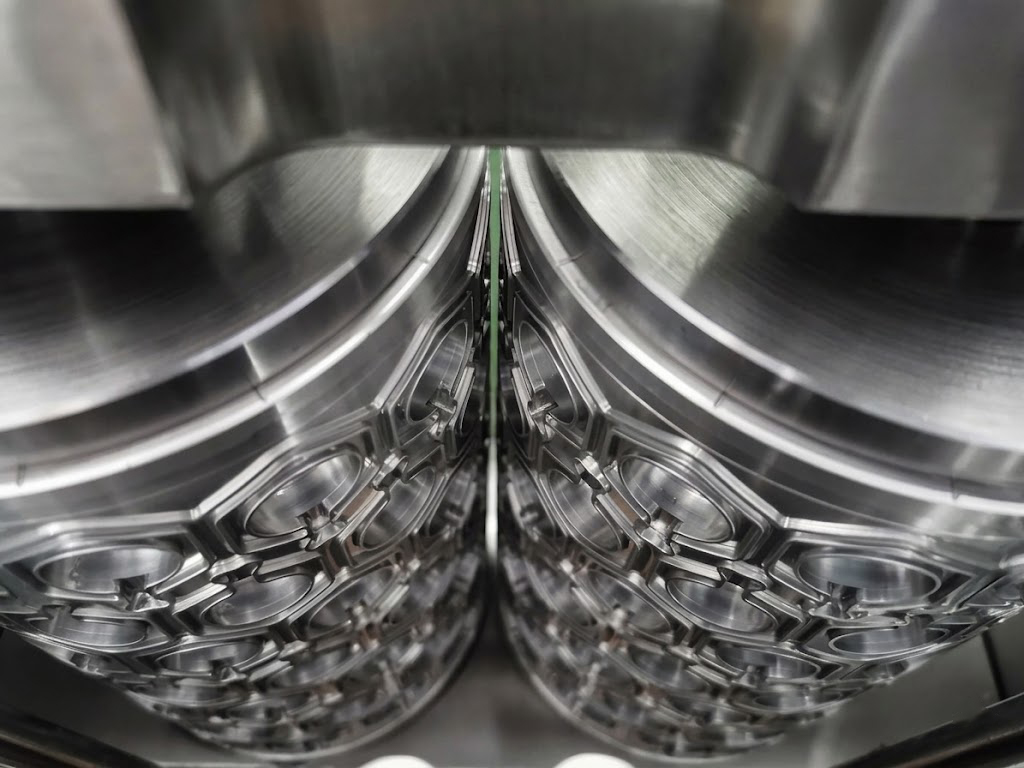
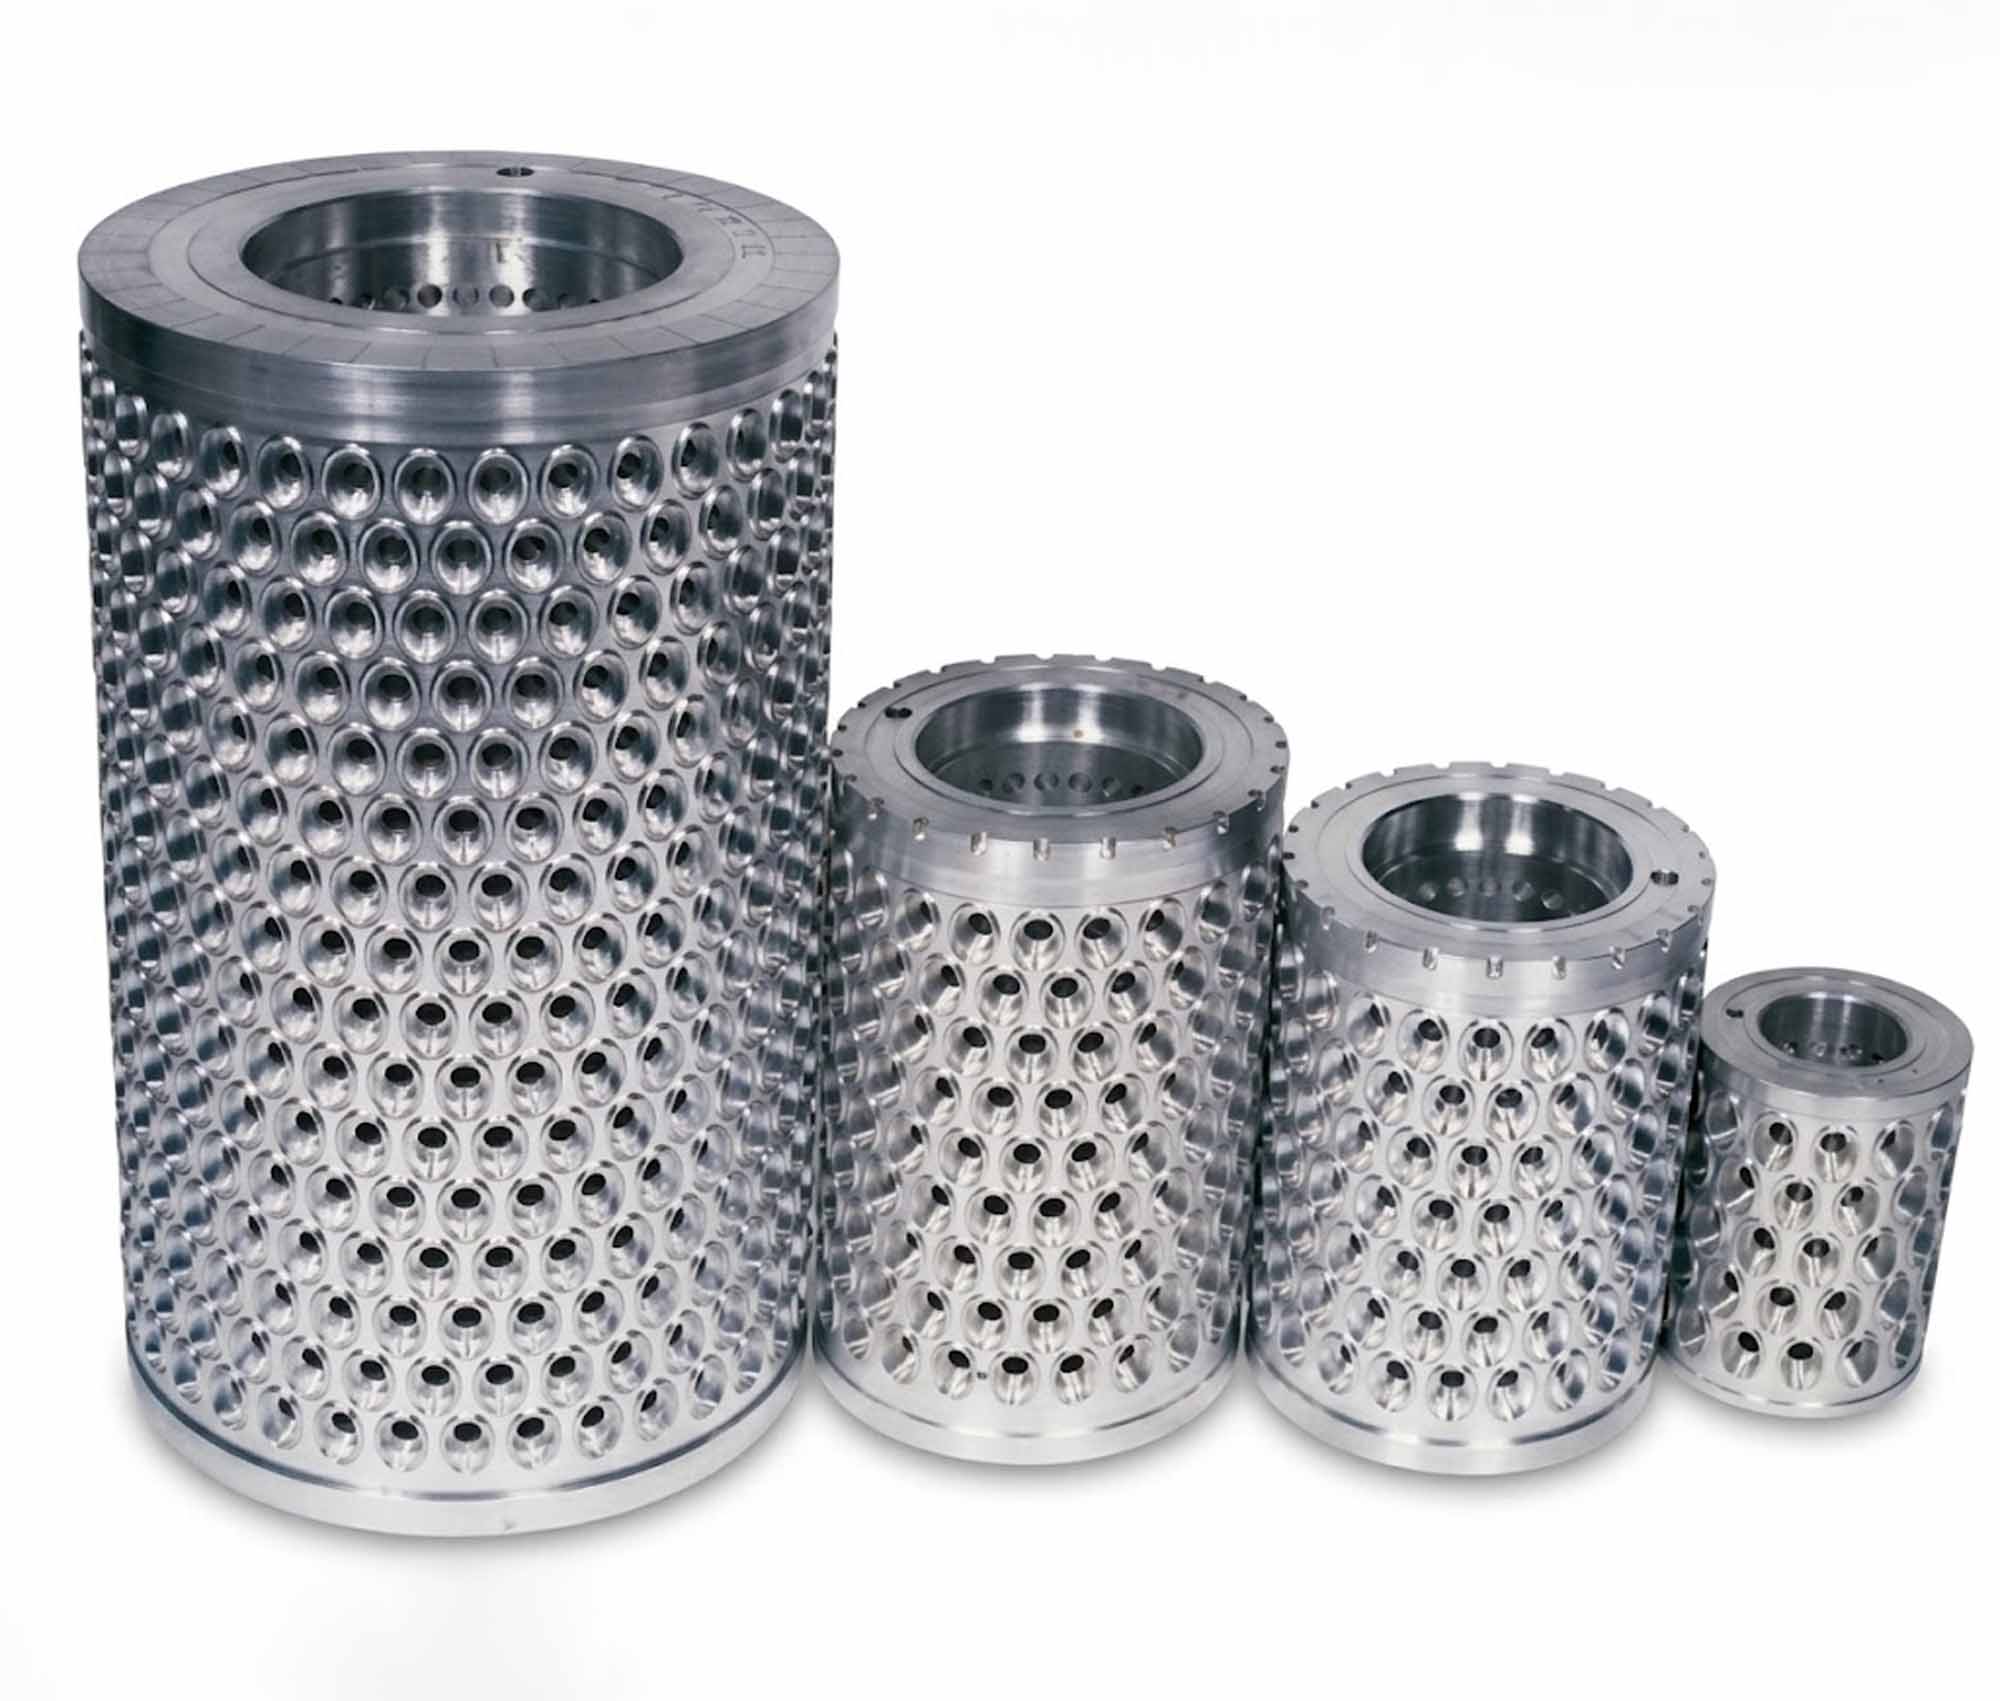
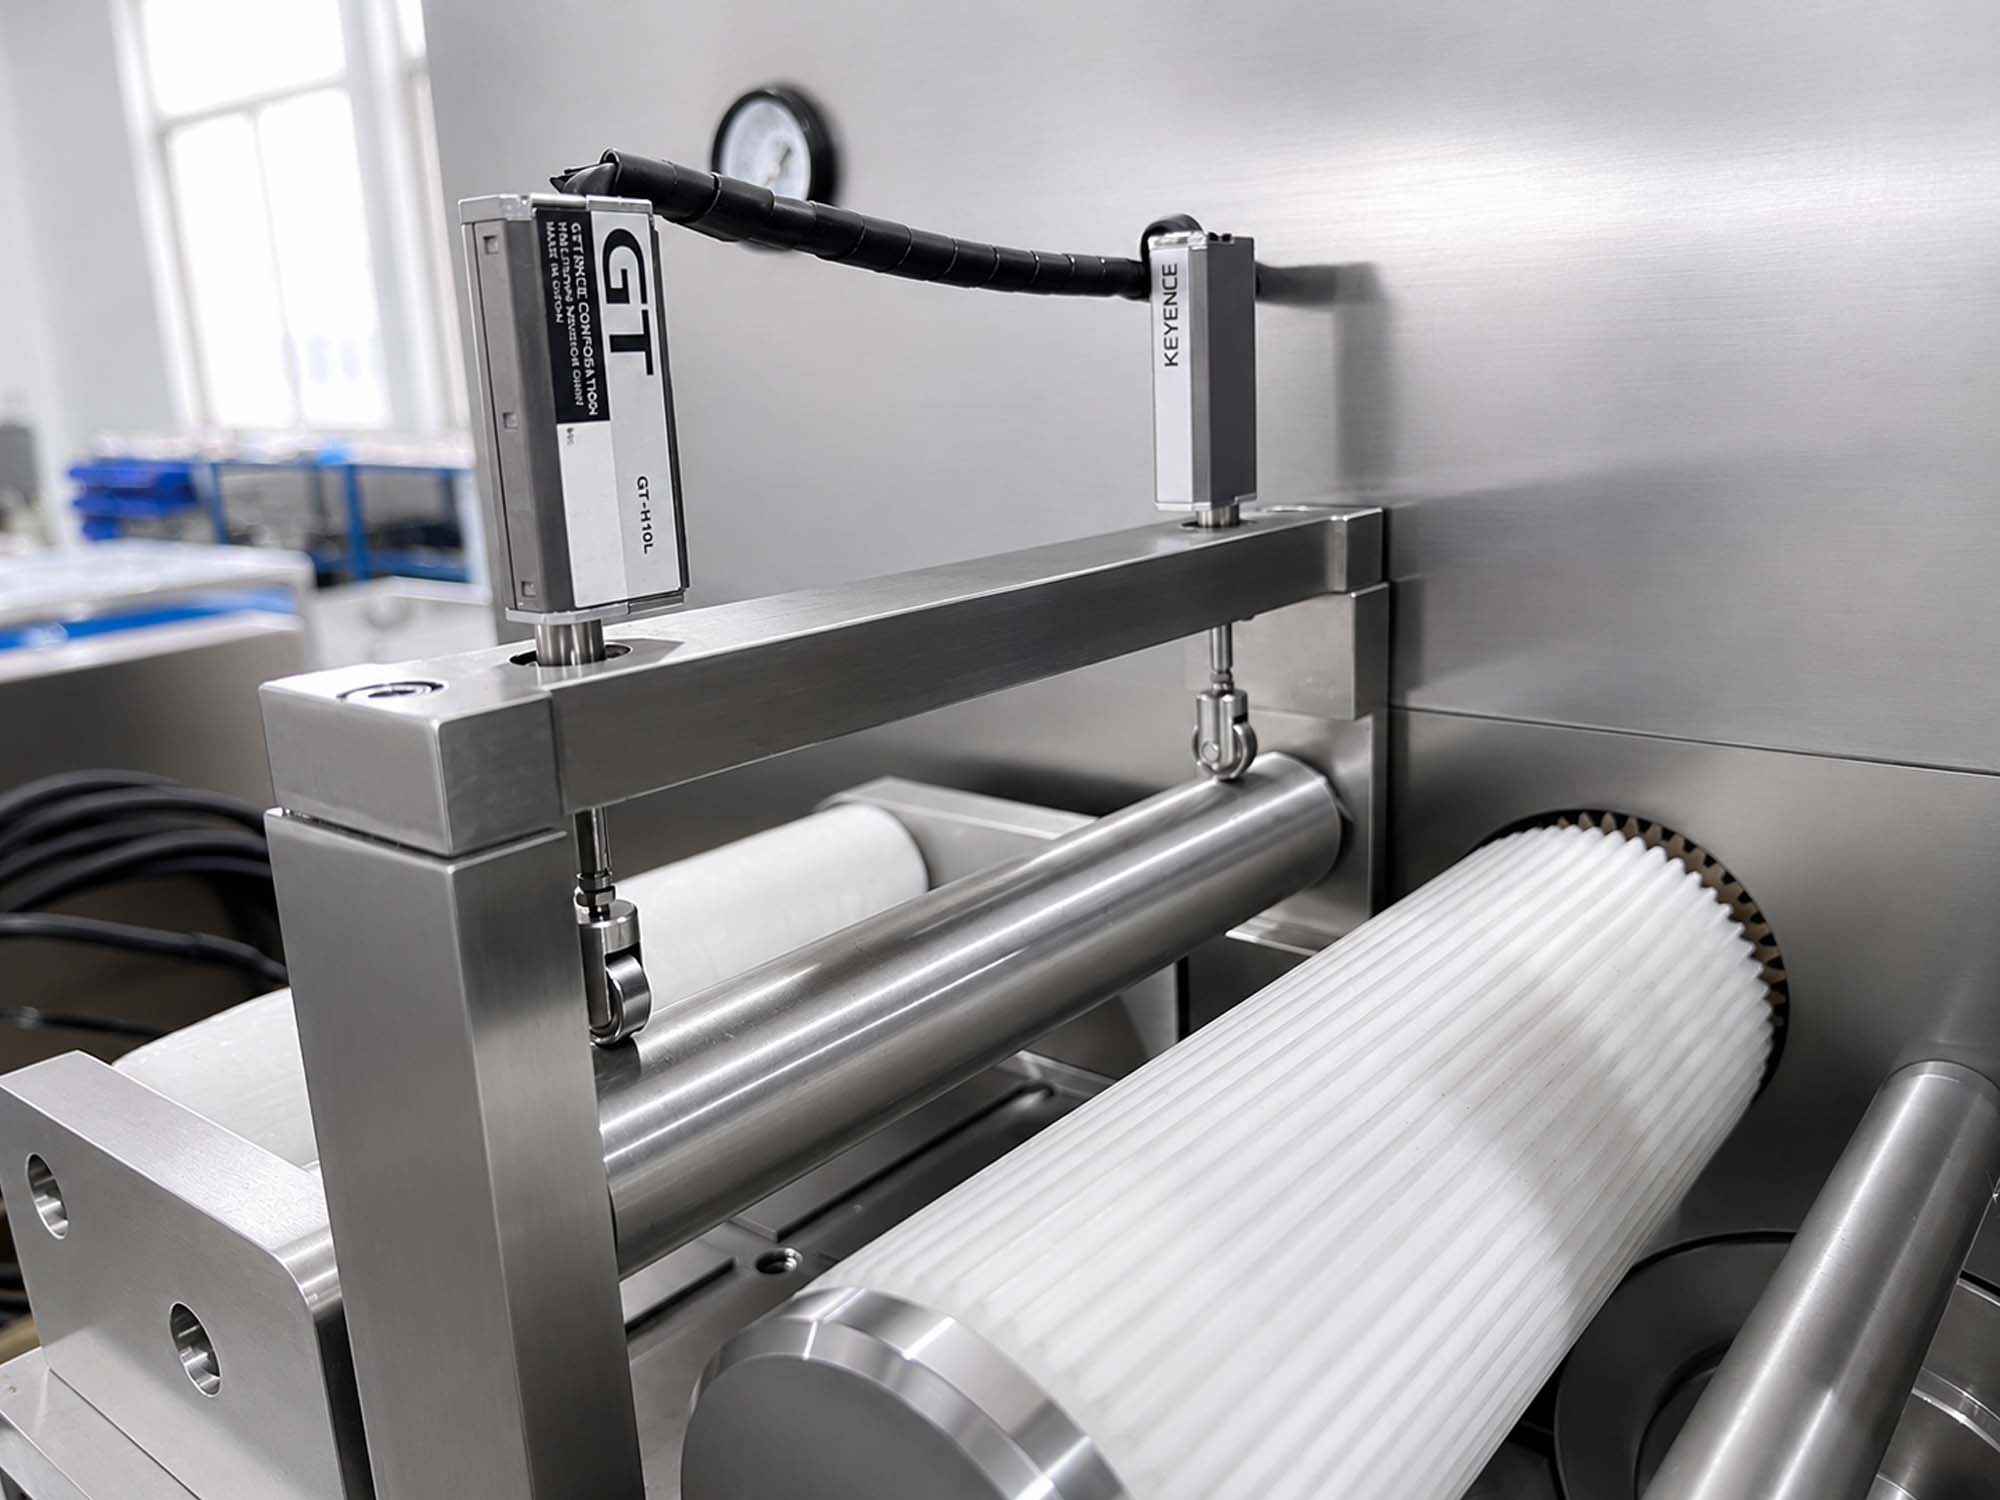
Large-Format Die Roll System (Φ150 x 250mm)
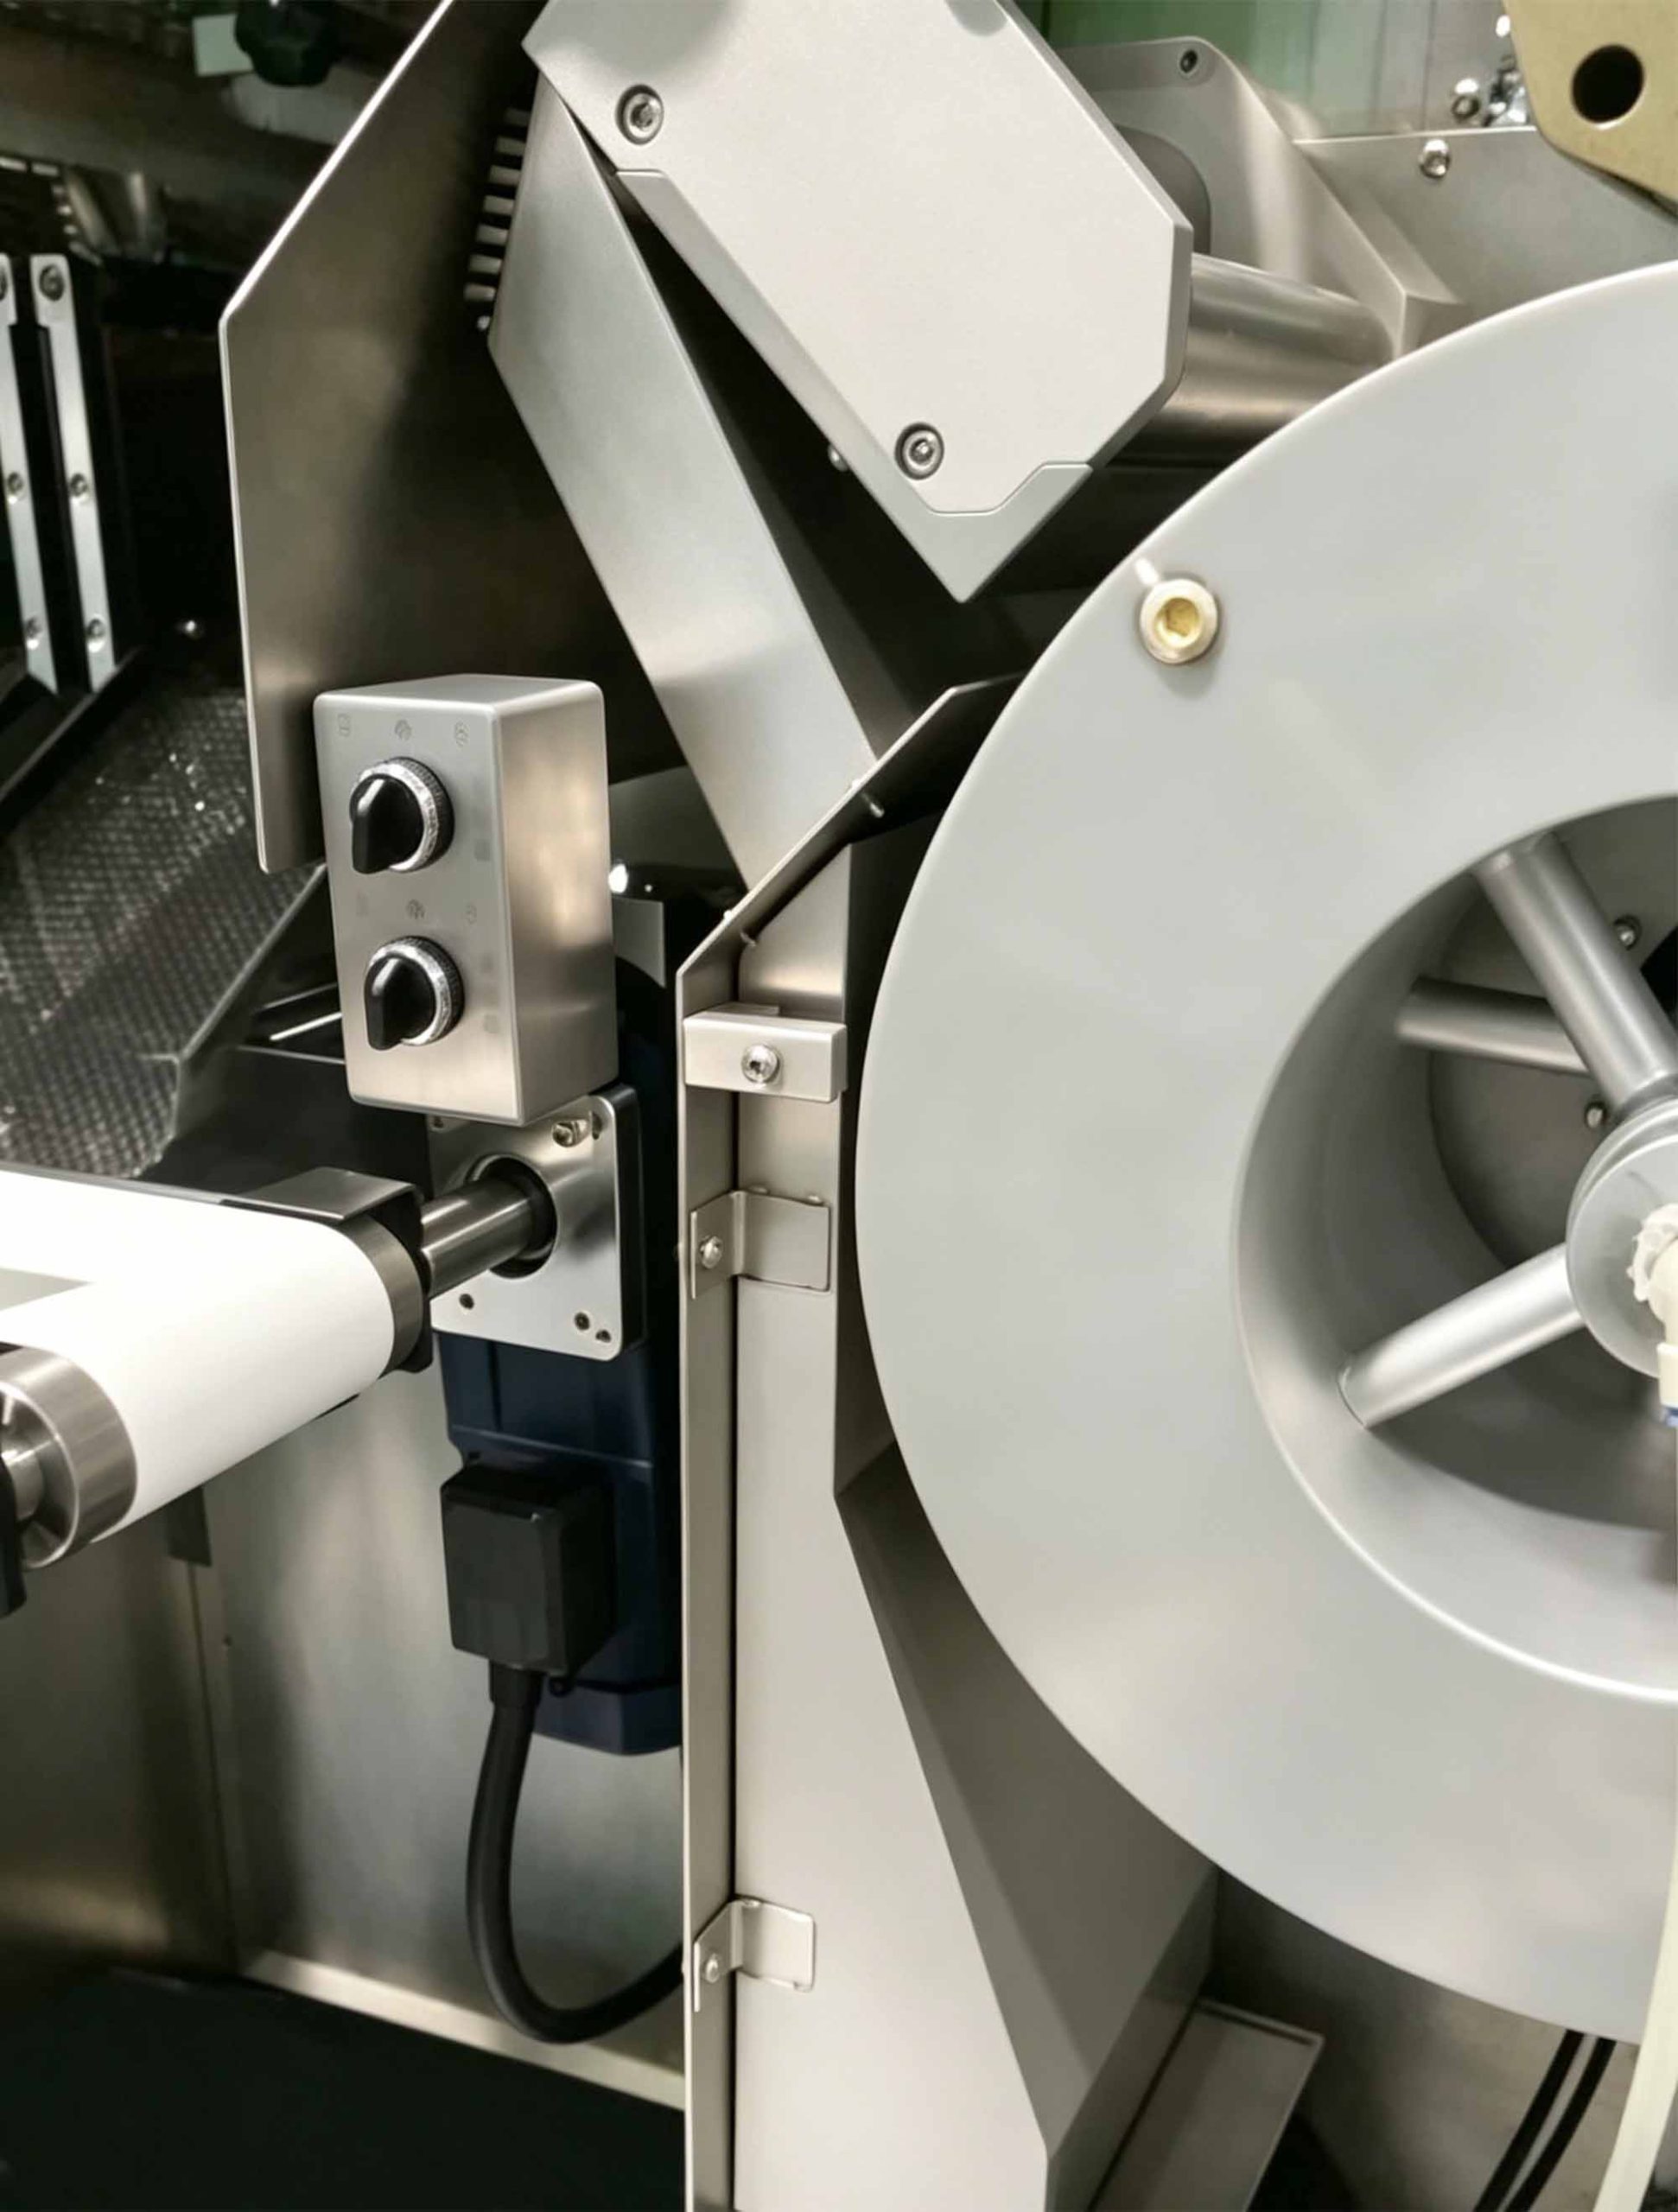
The SEM-250-II features our largest standard die roll, providing maximum pocket density. This significantly increases output per rotation, so output per rotation goes up without running the die rolls faster.
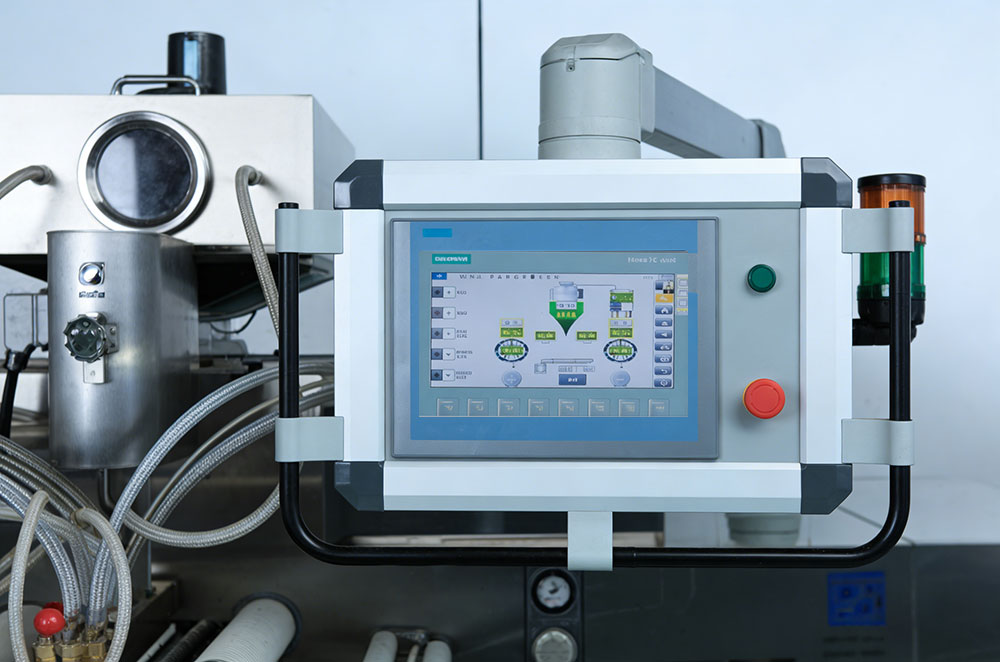
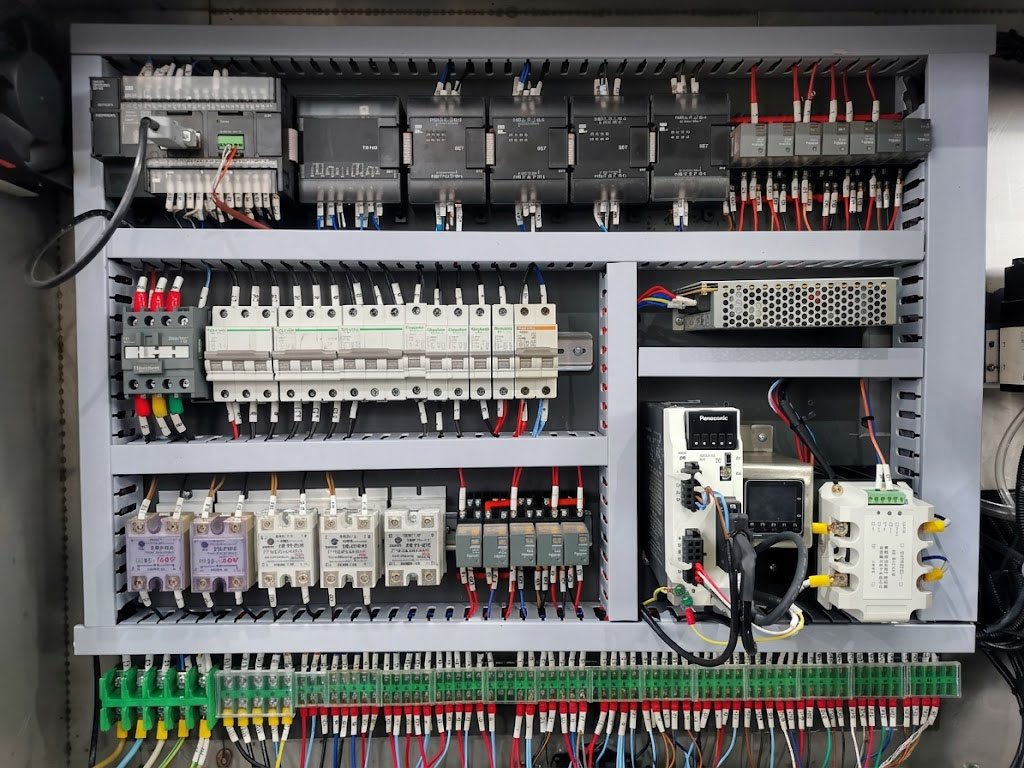
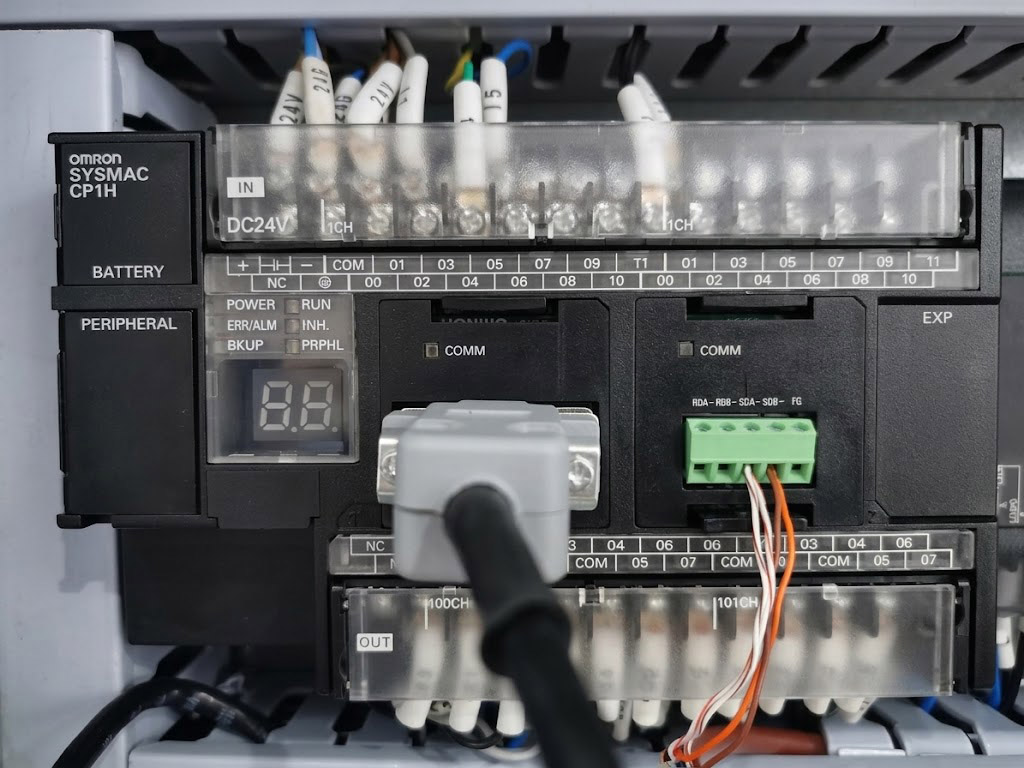
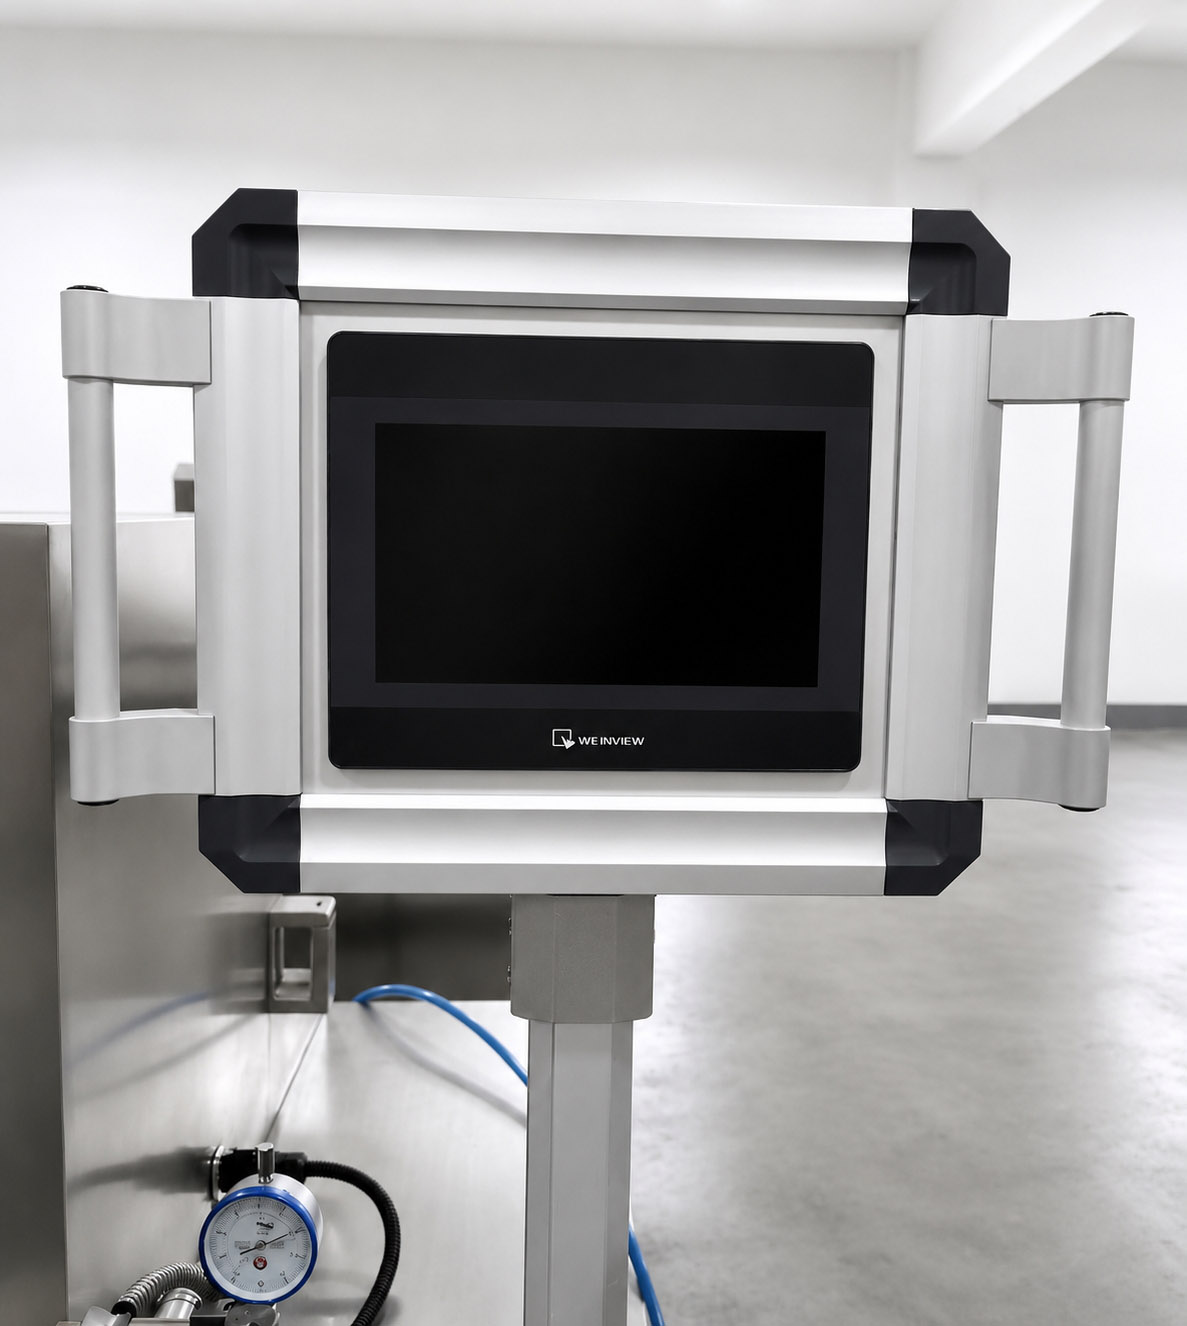
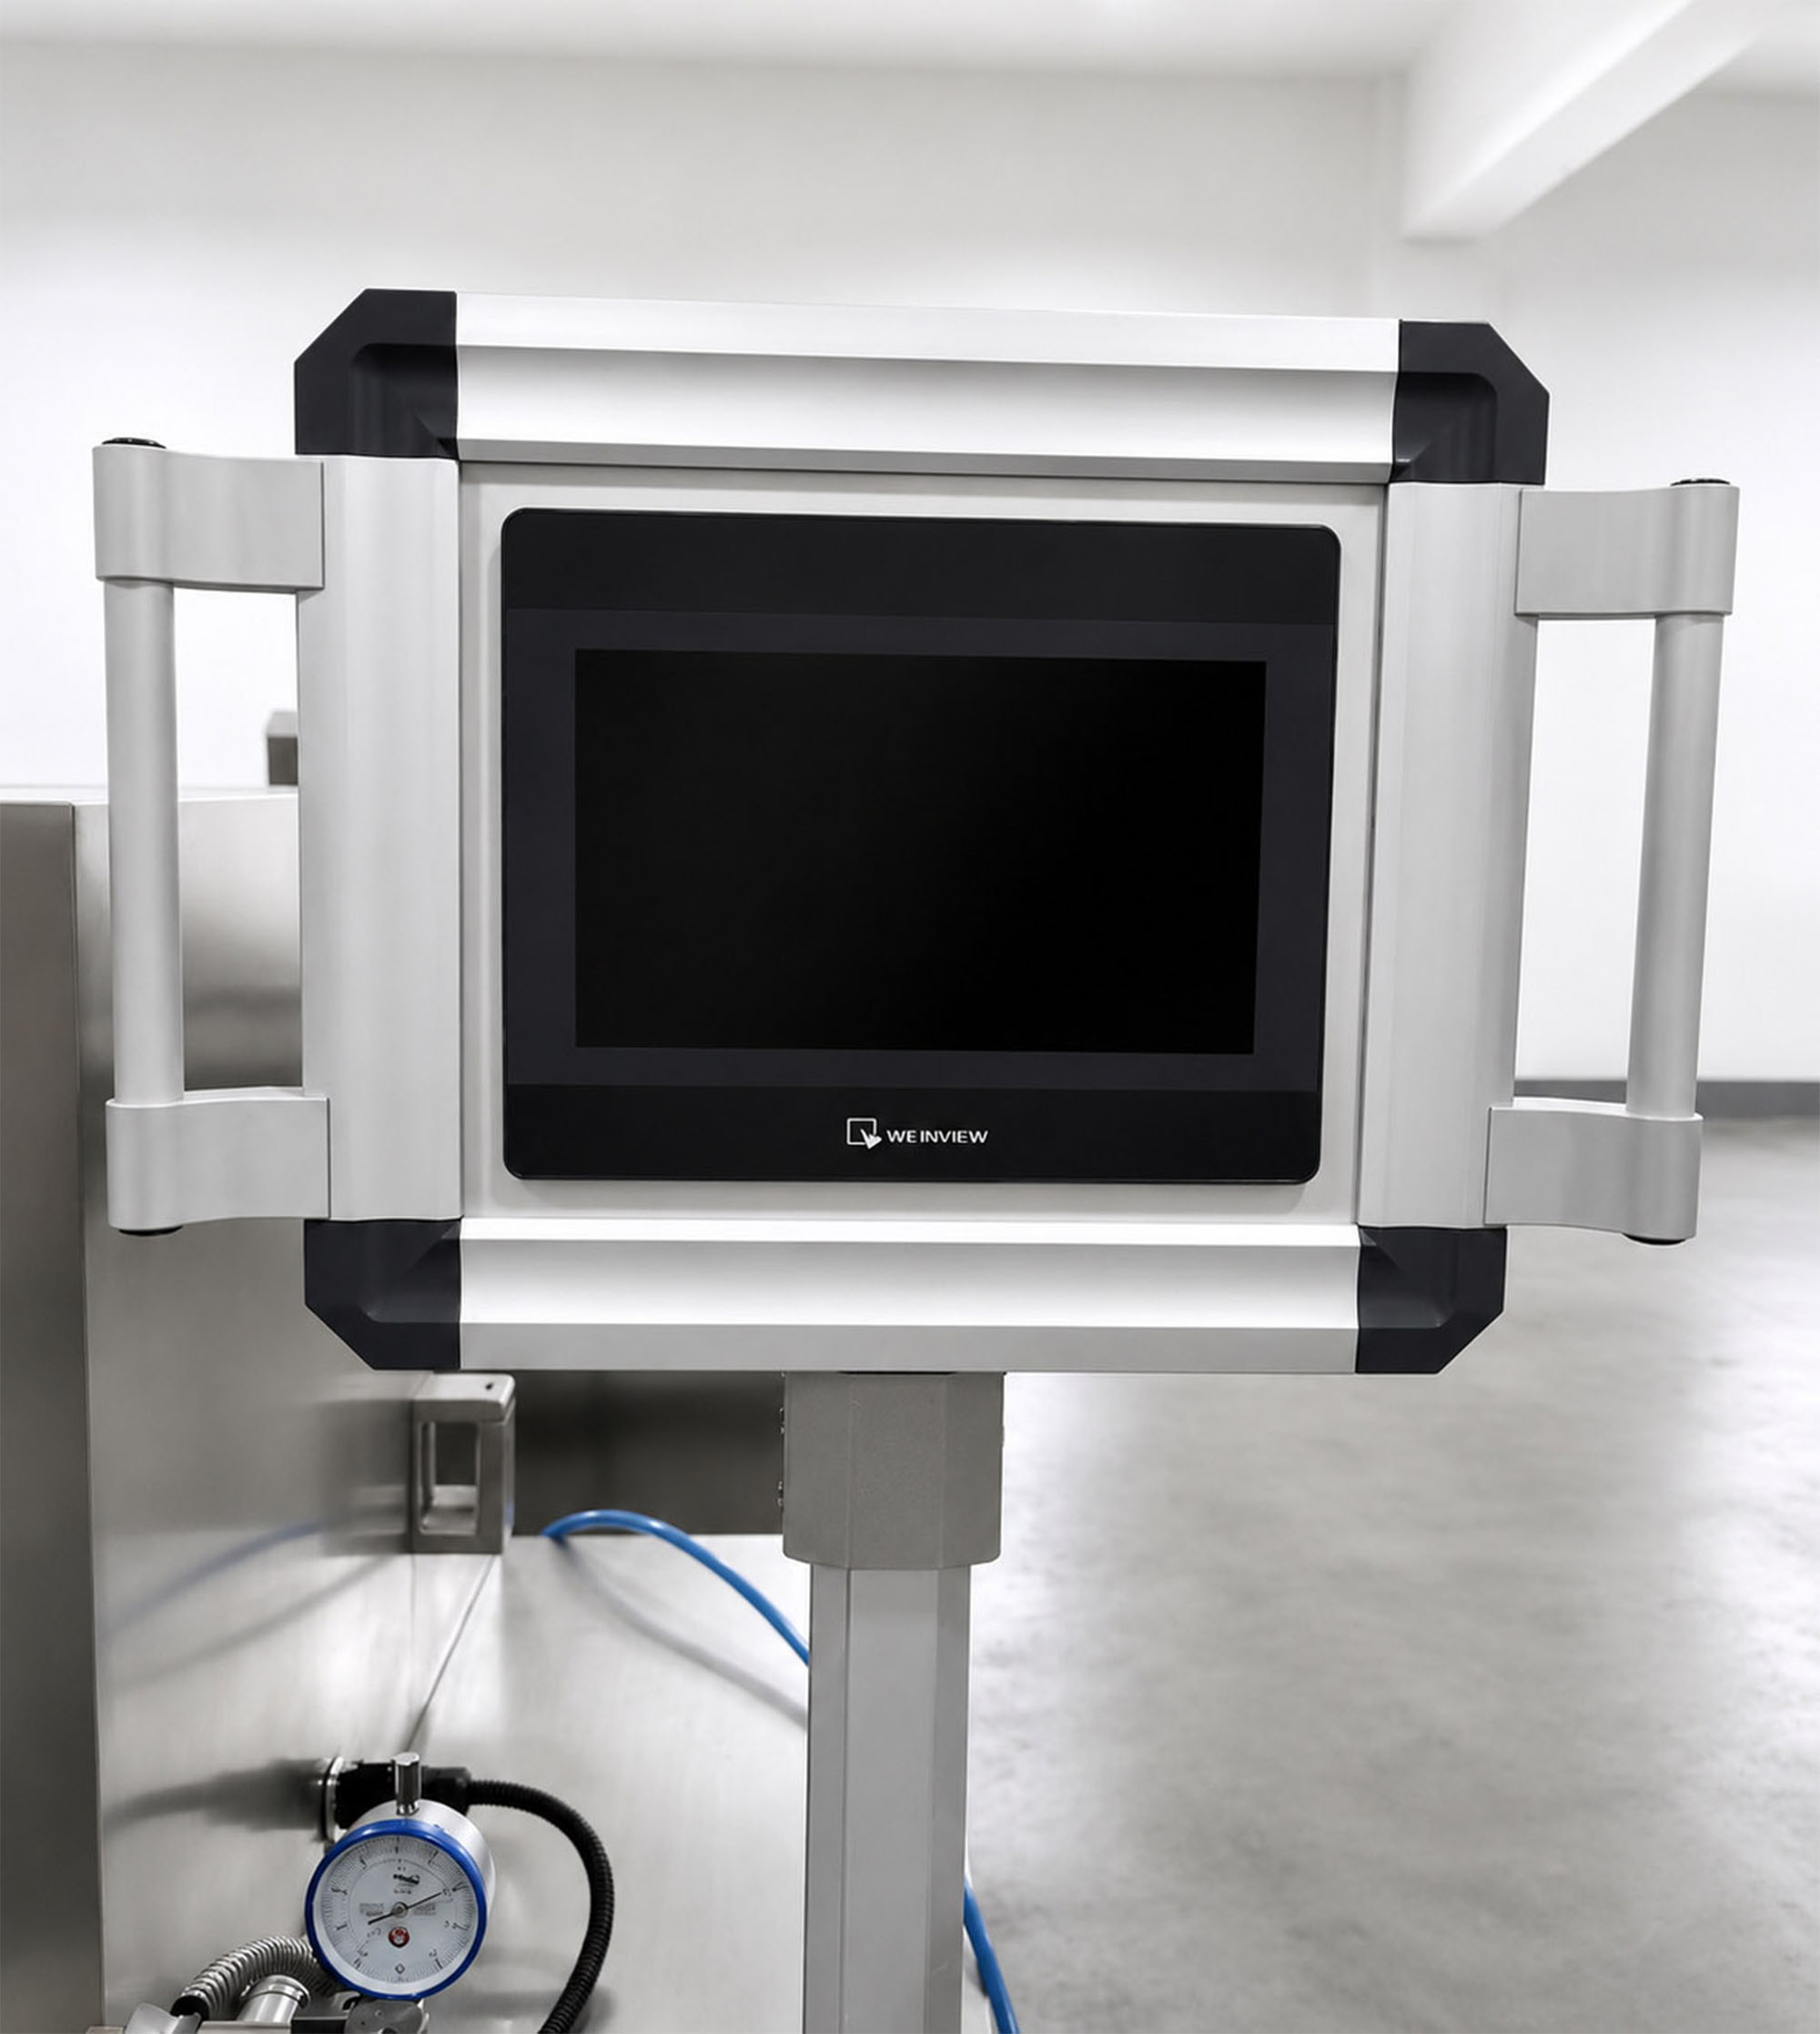
Advanced PLC Control & Touchscreen HMI
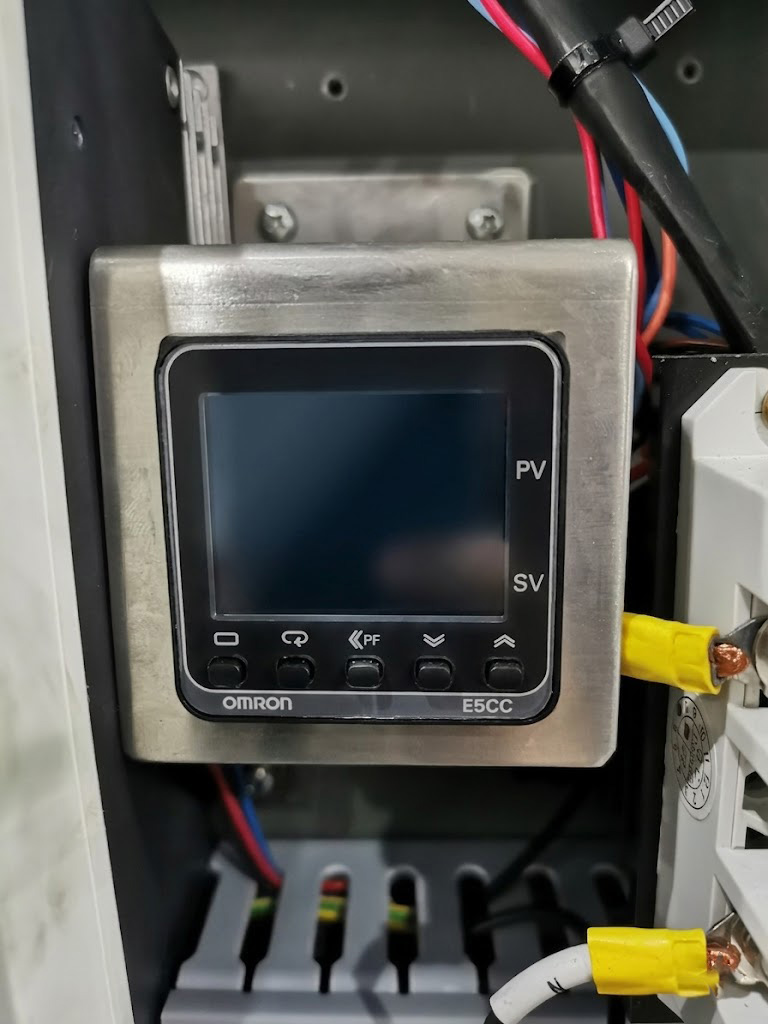
The entire production process is managed by a centralized PLC system. Operators can control die roll speed, injection timing, and temperature settings via a user-friendly interface, ensuring precise control over the entire encapsulation line.
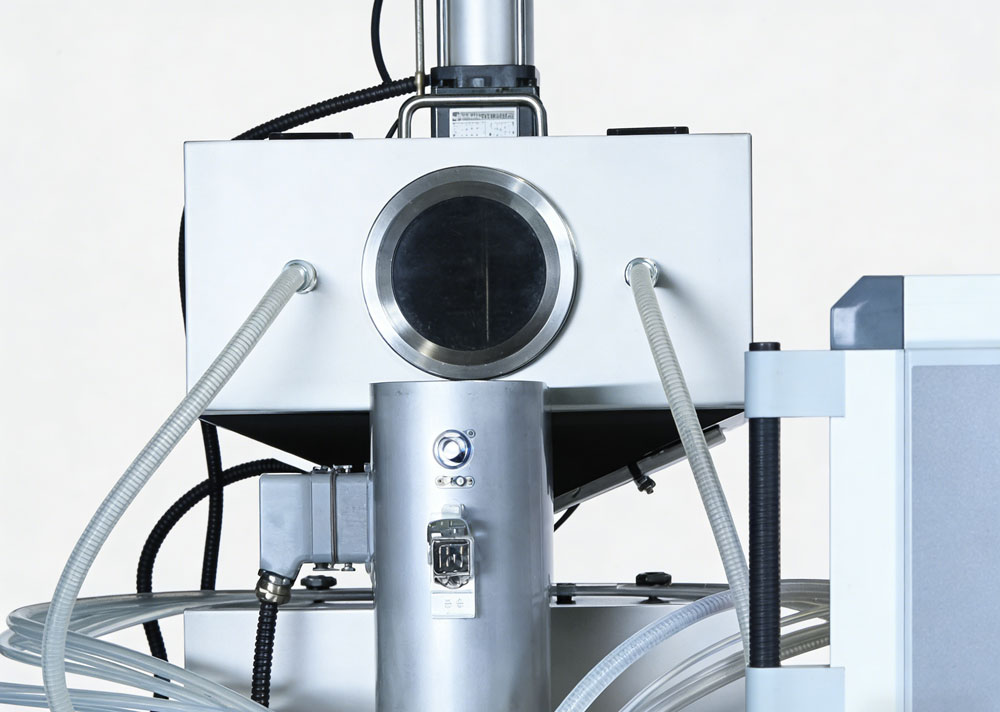
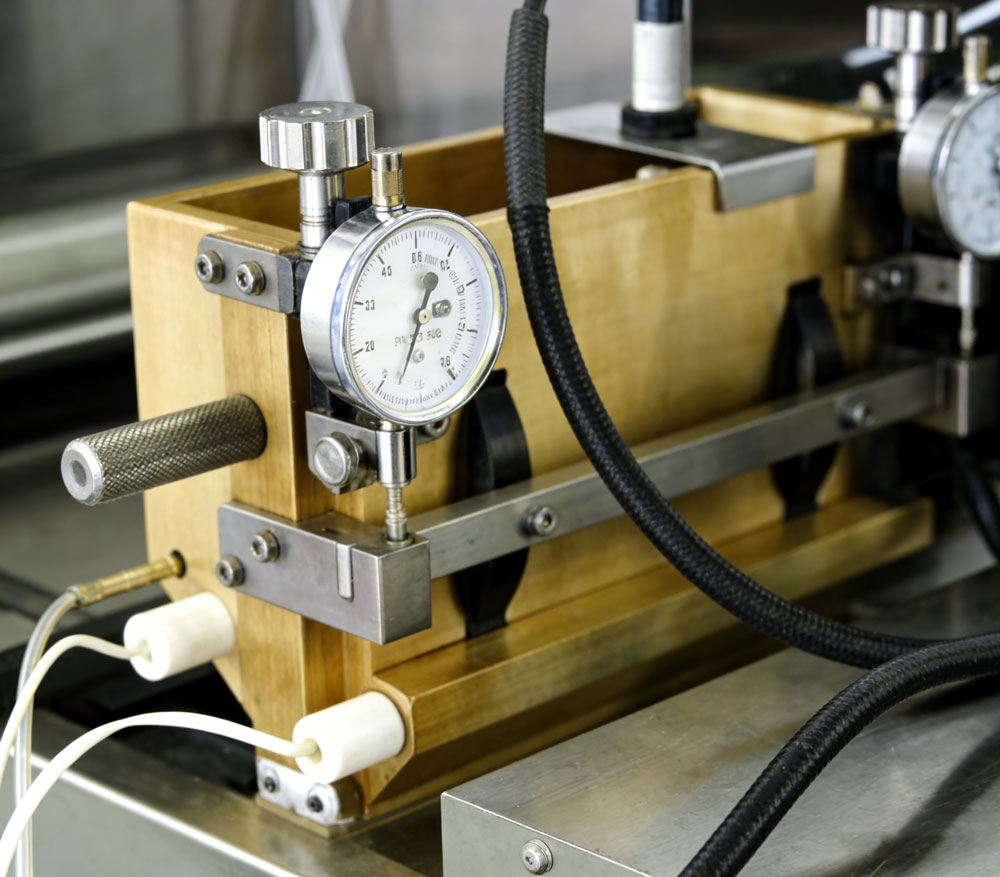
Precision Injection with High-Volume Pump
The 20-plunger injection pump holds ±0.5% on oils and ±1.5% on suspensions. The two behave differently in the plunger, which is why they hold different tolerances.
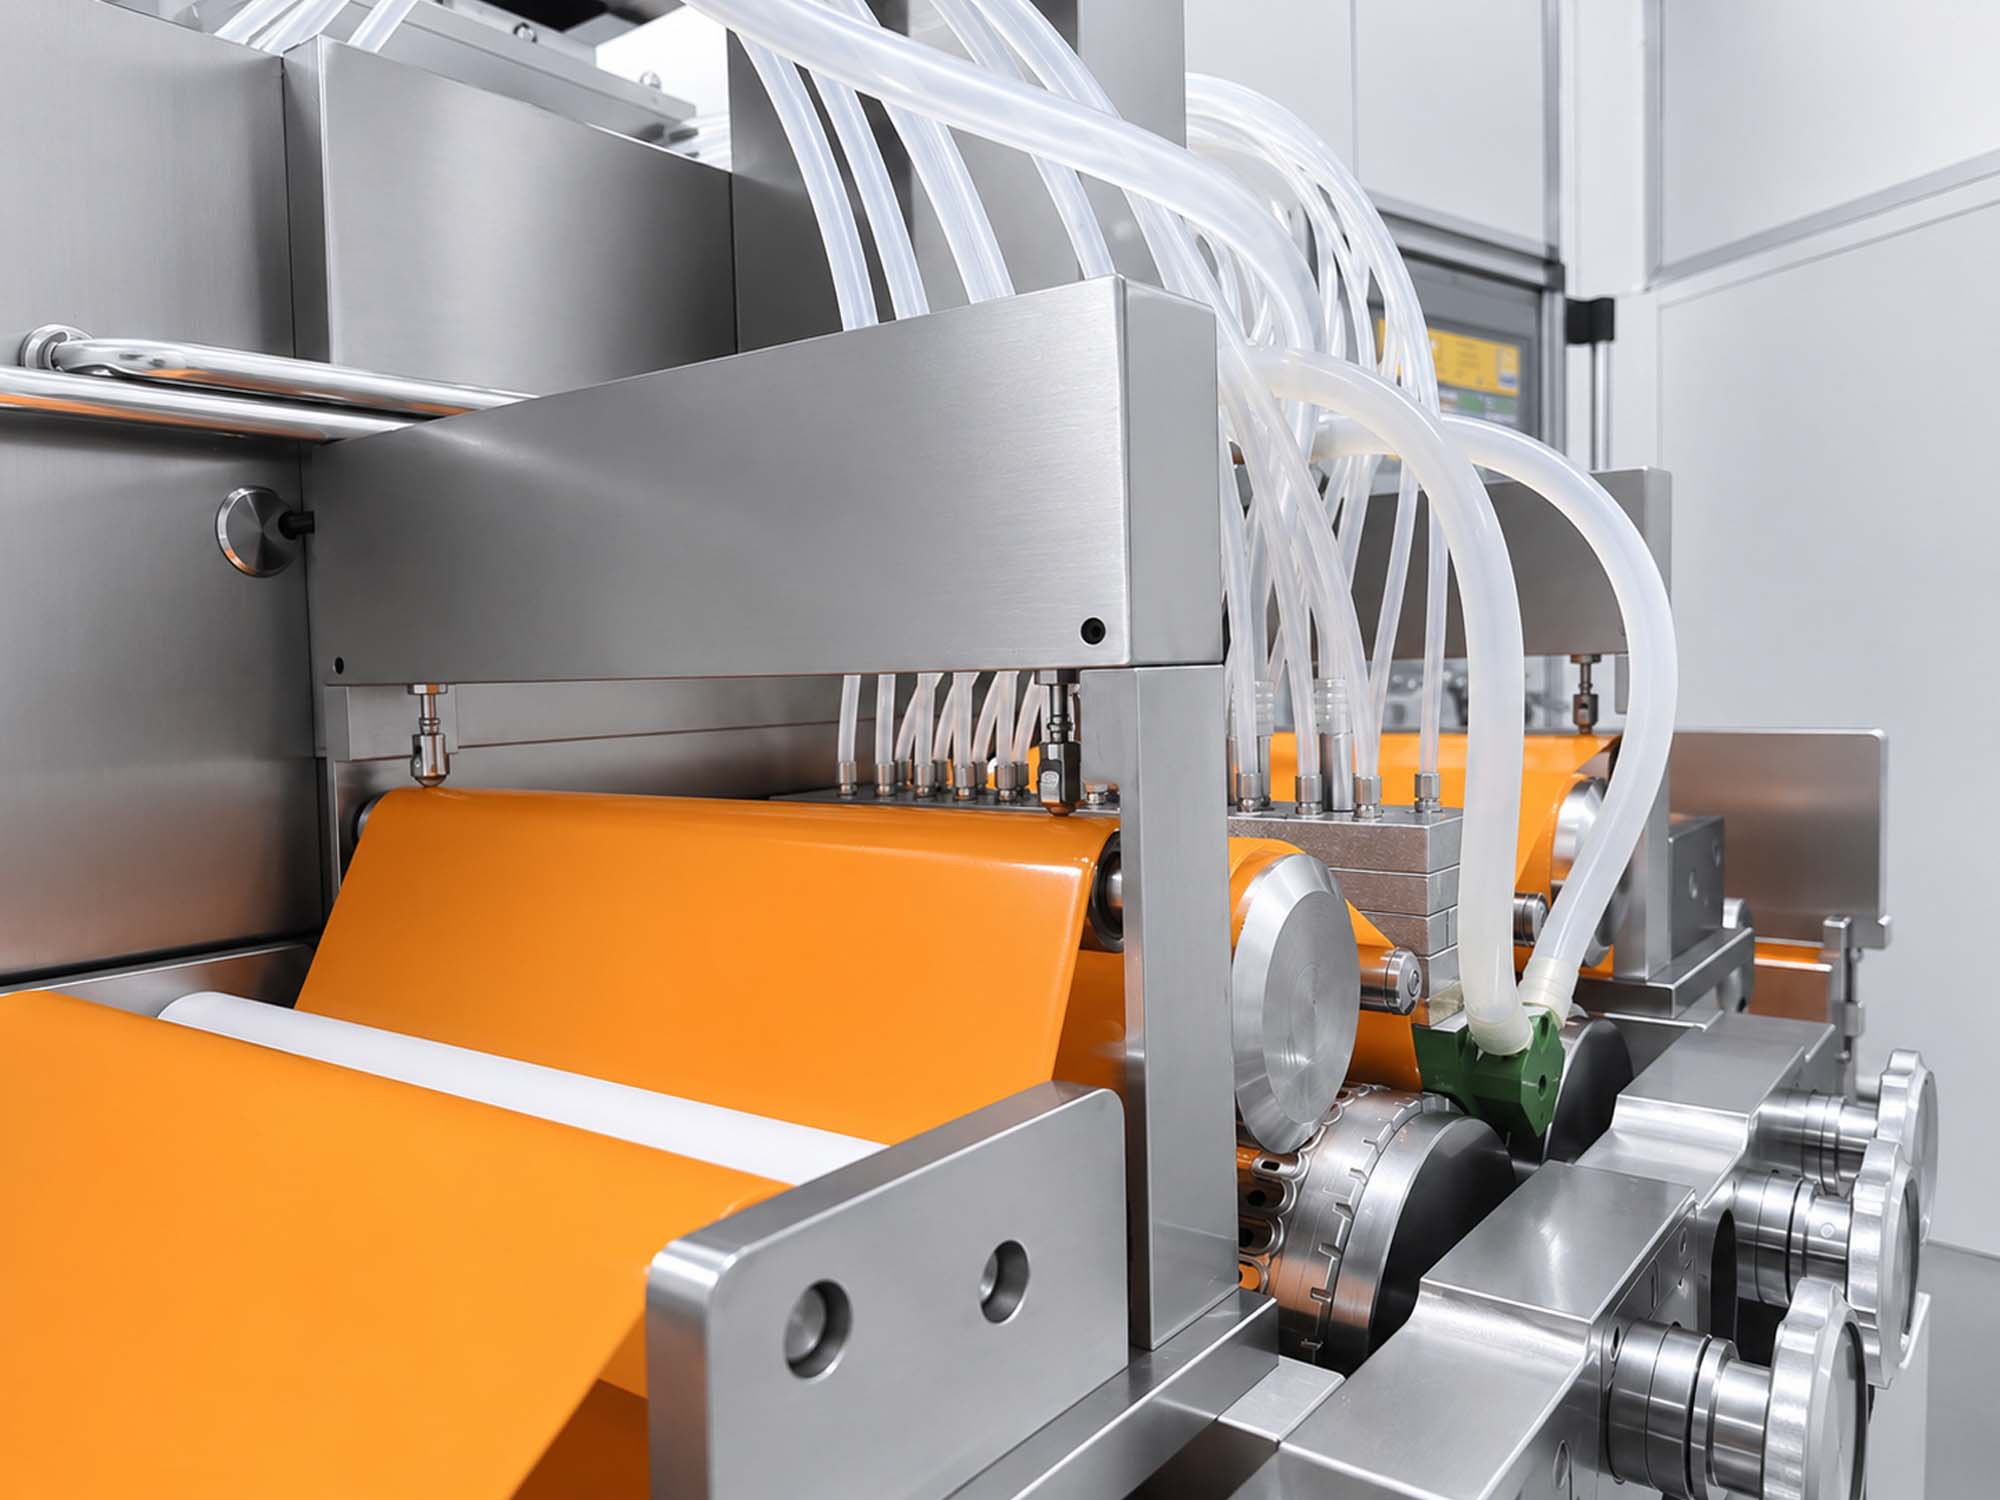
Integrated Ribbon Cooling & Thickness Control
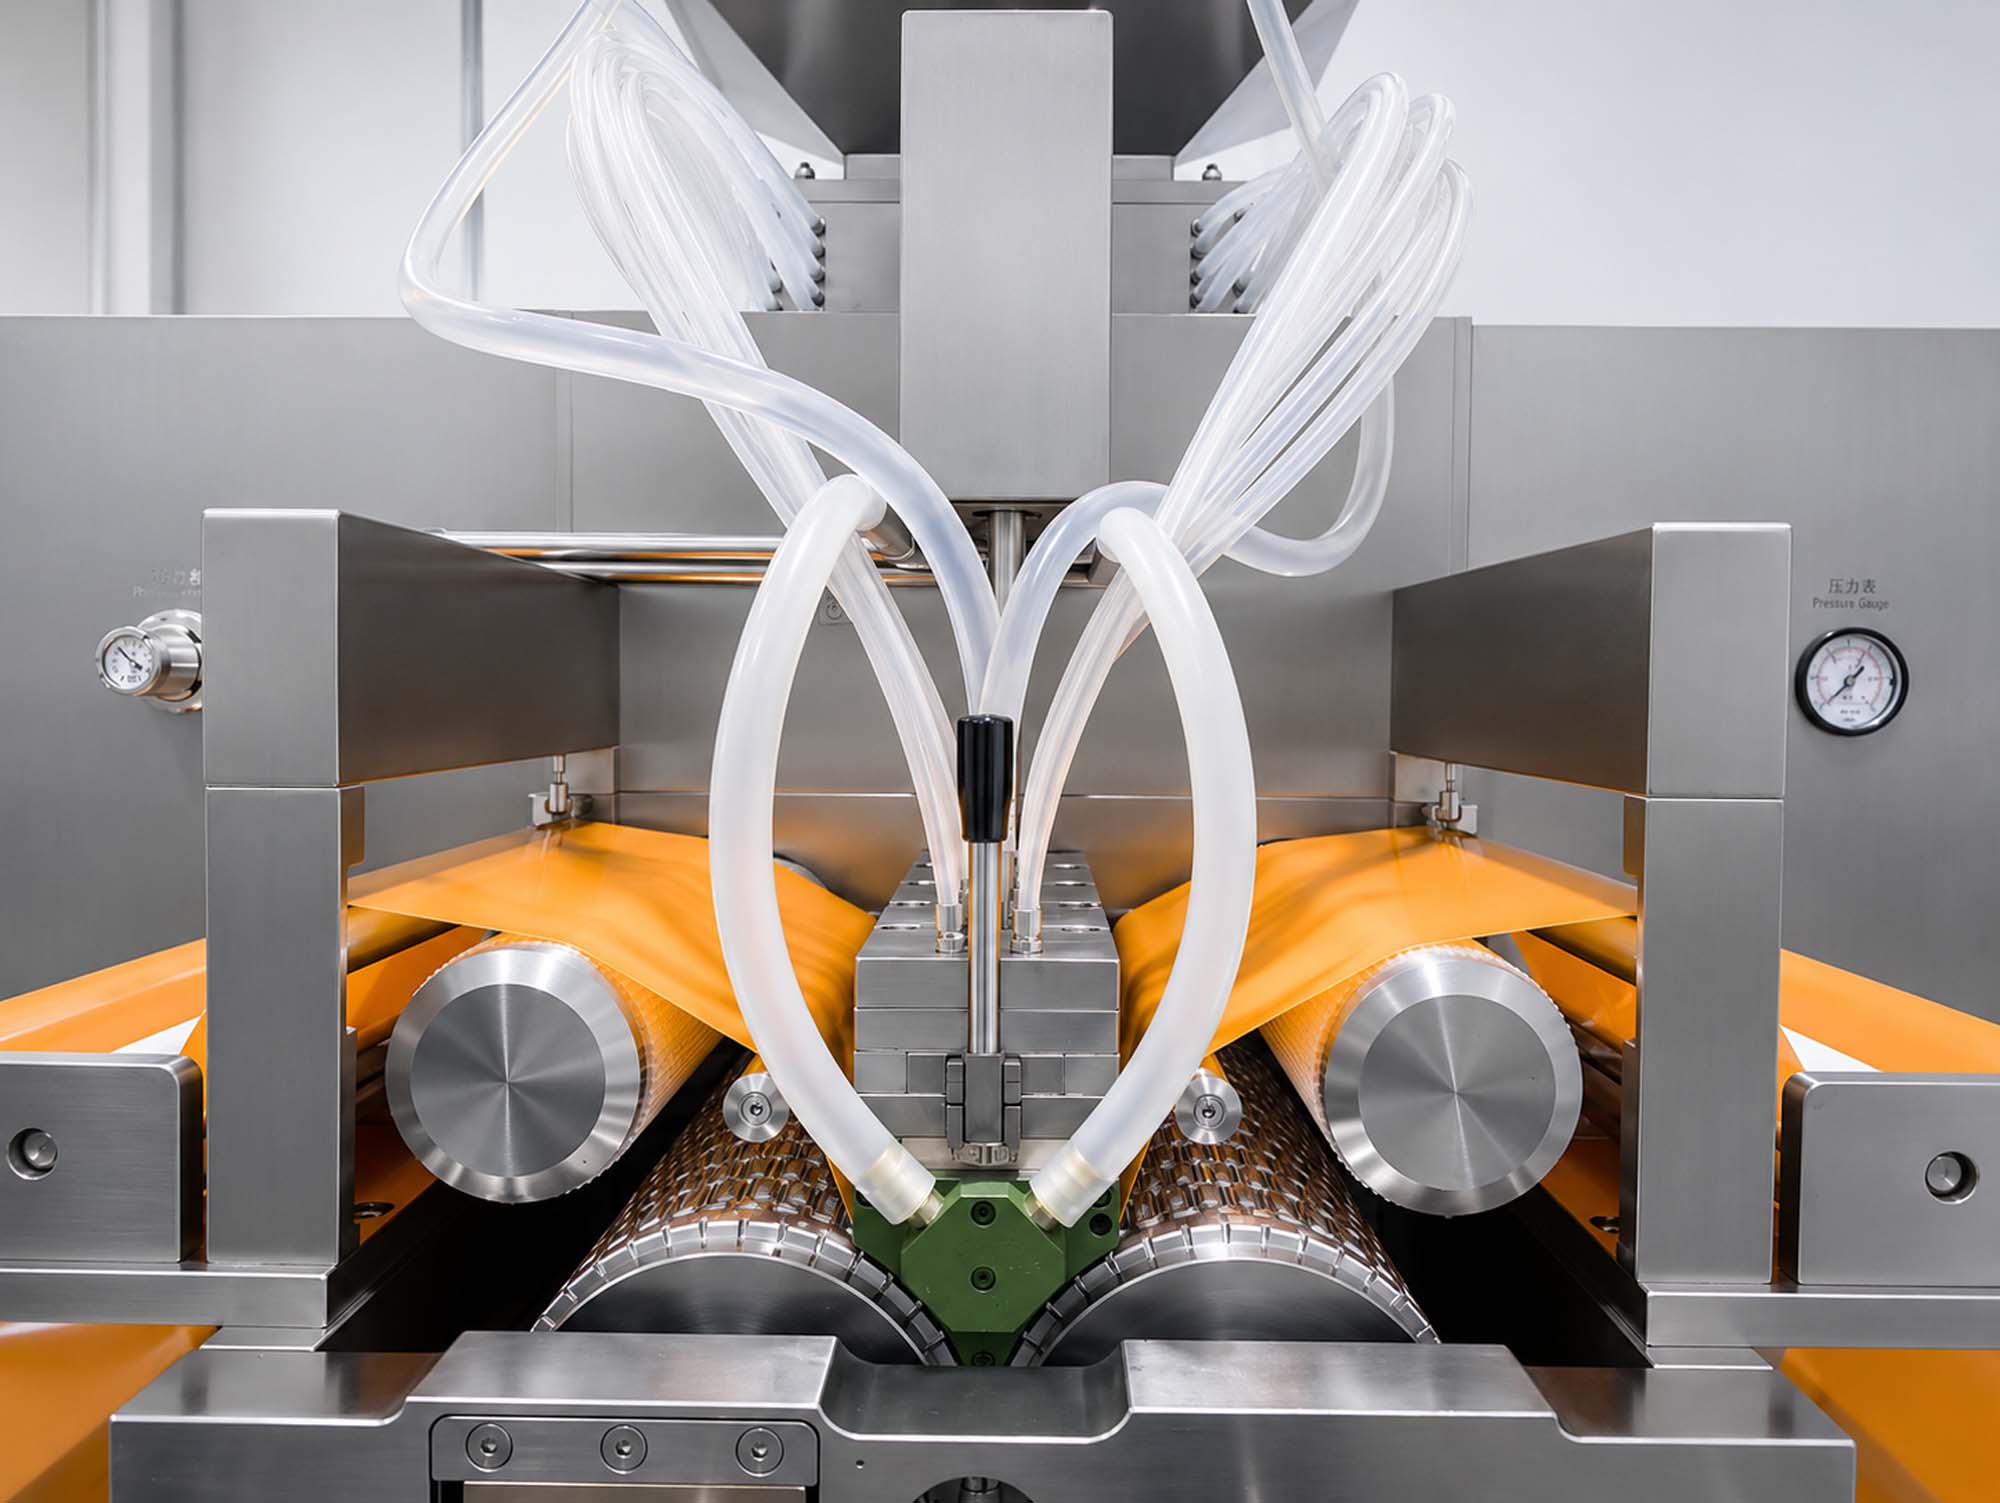
Equipped with dual independent cooling drums and high-efficiency cold air blowers, the machine ensures the gelatin ribbon reaches the perfect elasticity. An automatic ribbon control system can be added to hold the ribbon at the thickness you set.
Automatic Micro-Lubrication System
Micro-lubrication uses very little oil on the ribbon, so capsules come off cleaner and need less washing before drying.
Applications & Industries
Fish oil and omega-3
The single largest softgel category. Clean oils hold the tightest tolerance these machines offer.
Vitamin D, E and fat-soluble actives
Small fills in small shells. At 3# and 5# sizes the plunger stroke is short, which is where filling accuracy matters most.
CoQ10 and suspension fills
Suspensions behave differently from oils and hold a wider tolerance. A colloid mill upstream is usually part of the answer — tell us your particle size.
What changing over involves
Swapping the mold is physical work. Recalling the settings is not
What changed | What you adjust | Roughly |
Same shape, new batch | Nothing on the machine | — |
Different fill, same shape | Injection timing and wedge temperature | 15–30 minutes |
Different capsule shape | Die rolls and injection pump swap, then recalibrate | 15–30 minutes |
Gelatin → vegan shell | Not a changeover. That’s a build configuration | — |
On the servo models, once a product is dialed in, speed, temperature, injection timing and ribbon thickness are stored as a digital profile. The mold still has to be swapped by hand — what you save is the recalibration afterwards.
Custom die rolls for a new shape take 2 to 3 weeks to machine and test.
What to check before you buy
Filling accuracy, and on which fill
Oil and suspension don't hold the same tolerance — ours are ±0.5% and ±1.5%. Ask any supplier which number applies to your product, and ask how it's verified at the factory acceptance test. A single headline figure usually means nobody has asked.
The manual
A clear English manual gets your operator running in a week instead of a month. Ask to see a sample page before you order.
Installation and training
One engineer to your plant, about two weeks. Travel and on-site costs are quoted separately. Installation isn't free anywhere — it's either a line item or it's inside the machine price. We quote it as a line item so you can see it.
Why Choose AIPAK?
We Size the Whole Line, Not Just the Encapsulator
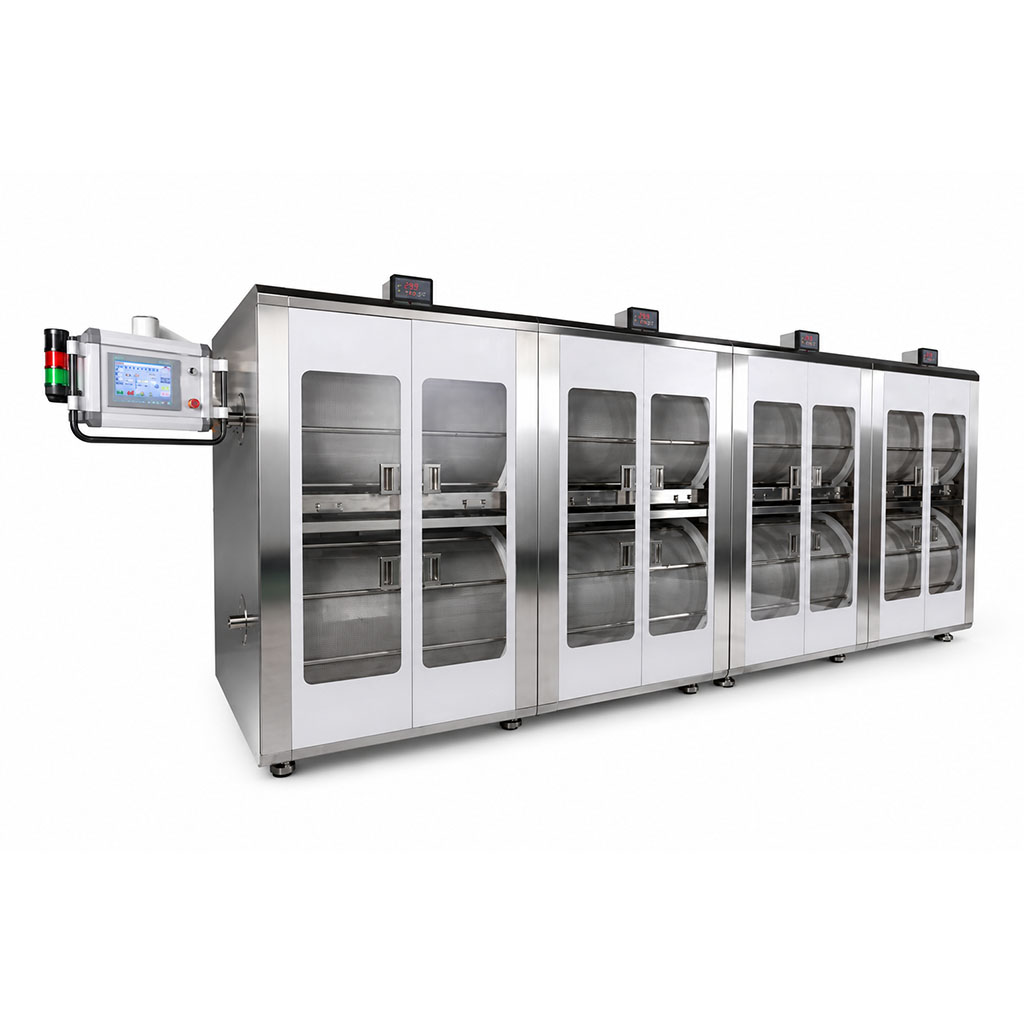
An encapsulator running at full speed produces more capsules than most buyers expect to dry. A Φ1000 tumbler line needs 16 to 18 sections to support 24-hour production, not the 10 that cover a single shift. We calculate your drying, gelatin melting and inspection capacity alongside the machine — before you order, not after.
Formulation Decides Configuration
Vegan shells need a different wedge, a different spreader box and a heated cooling drum. High-viscosity fills need a colloid mill upstream. Suspension products hold a different filling tolerance than oils. Tell us what you are encapsulating and we will specify around it, rather than sending a standard machine and hoping it fits.
A U.S. Number, Answered by Us
+1 (213) 526-8644, answered by our engineers 9 AM–7 PM China time, Monday to Friday. That’s evening and overnight in the U.S., so leave a message or send a WhatsApp anytime and we’ll pick it up first thing.
Spare Parts and Lead Time, in Writing
A kit of wear parts ships with your machine. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.
SEM-250-II Industrial Production FAQ
Stability at high speeds is our priority. The SEM-250-II features a heavy-duty frame and a precision-balanced 20-plunger injection pump. Unlike smaller machines, its transmission system is designed to handle high torque without vibration, holding ±0.5% on oils and ±1.5% on suspensions at full speed.
We understand that gelatin cost is a major factor in large-scale production. Most of the waste comes at startup, while the ribbon thickness and injection timing are being set. Adding the automatic ribbon control system shortens that, because the operator types in the thickness instead of adjusting it by hand. If startup waste matters to you, ask us to compare this machine with the servo 250-IIIA.
Yes. The cooling drums and gelatin box temperatures are independently controlled via the PLC. This allows for precise thermal management tailored to the specific melting points and setting speeds of different gelatin types, so the ribbon and seam stay consistent on each gelatin type.
To support its high capacity, the SEM-250-II is equipped with an enhanced dual-drum cooling system and independent high-volume air blowers. For continuous industrial use, we provide integrated ports for external water chillers, ensuring the cooling drums maintain a constant, optimal temperature to prevent “sticky ribbons” or shell deformation.
The main shaft bores are machined on a Swiss-imported boring mill, so runout and parallelism between the left and right shafts stay within tight limits — that alignment is what determines how long a machine holds its seam quality. Under a standard preventive maintenance schedule, the drive system is built for long-term continuous industrial operation. We supply the maintenance schedule and a spare-parts list with the machine.
Despite its size, the SEM-250-II features a modular “Easy-Access” design. A complete set of die rolls and the injection pump can be swapped and recalibrated in approximately 60–90 minutes by two trained technicians. This minimizes downtime between different product batches (e.g., switching from 20 Oblong to 10 Oval).
A kit of wear parts ships with your machine. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing, including remote video diagnostics and on-site engineering services to ensure your production line never stops.
Yes. We build to your U.S. supply at 60 Hz and confirm the voltage with your quote.
A kit of wear parts ships with your machine. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.
Customers Also Interested In...
Send Us Your Fill and Your Capsule Size
Tell us what you’re encapsulating, your shell type, your capsule size and shape, your target output, and whether you already have drying capacity. We’ll come back with the encapsulator, the drying and the gelatin melting sized to match.
- Direct from our factory
- Lead time confirmed in your quote
- Installation and training available
- Spare parts listed in your quote